Общий каталог Mitsubishi 2020 - 2021 - страница 913
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
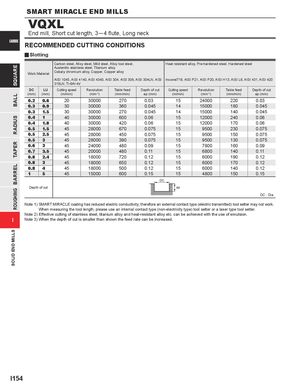
VQXL
End mill, Short cut length, 3─4 flute, Long neck
CARBIDE RECOMMENDED CUTTING CONDITIONS
y Slotting
| Work | Material | Carbon steel, Allo Austenitic stainles Cobaly chromium AISI 1045, AISI 4 316LN, Ti-6Al-4V | y steel, Mild steel s steel, Titanium alloy, Copper, Co 140, AISI 4340, AI | , Alloy tool steel, alloy pper alloy SI 304, AISI 306, | AISI 304LN, AISI | Heat resistant allo Inconel718, AISI | y, Pre-hardened P21, AISI P20, AI | steel, Hardened s SI H13, AISI L6, A | teel ISI 431, AISI 420 |
| DC (mm) | LU (mm) | Cutting speed (m/min) | Revolution (min-1) | Table feed (mm/min) | Depth of cut ap (mm) | Cutting speed (m/min) | Revolution (min-1) | Table feed (mm/min) | Depth of cut ap (mm) |
| 0.2 | 0.6 | 20 | 30000 | 270 | 0.03 | 15 | 24000 | 220 | 0.03 |
| 0.3 | 0.9 | 30 | 30000 | 360 | 0.045 | 14 | 15000 | 180 | 0.045 |
| 0.3 | 1.5 | 30 | 30000 | 270 | 0.045 | 14 | 15000 | 140 | 0.045 |
| 0.4 | 1 | 40 | 30000 | 600 | 0.06 | 15 | 12000 | 240 | 0.06 |
| 0.4 | 1.8 | 40 | 30000 | 420 | 0.06 | 15 | 12000 | 170 | 0.06 |
| 0.5 | 1.5 | 45 | 28000 | 670 | 0.075 | 15 | 9500 | 230 | 0.075 |
| 0.5 | 2.5 | 45 | 28000 | 450 | 0.075 | 15 | 9500 | 150 | 0.075 |
| 0.5 | 3 | 45 | 28000 | 390 | 0.075 | 15 | 9500 | 130 | 0.075 |
| 0.6 | 3 | 45 | 24000 | 480 | 0.09 | 15 | 7800 | 160 | 0.09 |
| 0.7 | 3.5 | 45 | 20000 | 480 | 0.11 | 15 | 6800 | 140 | 0.11 |
| 0.8 | 2.4 | 45 | 18000 | 720 | 0.12 | 15 | 6000 | 190 | 0.12 |
| 0.8 | 3 | 45 | 18000 | 650 | 0.12 | 15 | 6000 | 170 | 0.12 |
| 0.8 | 4 | 45 | 18000 | 500 | 0.12 | 15 | 6000 | 140 | 0.12 |
| 1 | 5 | 45 | 15000 | 600 | 0.15 | 15 | 4800 | 150 | 0.15 |
| Depth | of cut | DC | ap |
DC : Dia. Note 1) SMART MIRACLE coating has reduced electric conductivity; therefore an external contact type (electric transmitted) tool setter may not work. When measuring the tool length, please use an internal contact type (non-electricity type) tool setter or a laser type tool setter. Note 2) Effective cutting of stainless steel, titanium alloy and heat-resistant alloy etc. can be achieved with the use of emulsion. I Note 3) When the depth of cut is smaller than shown the feed rate can be increased.