Общий каталог Mitsubishi 2020 - 2021 - страница 908
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
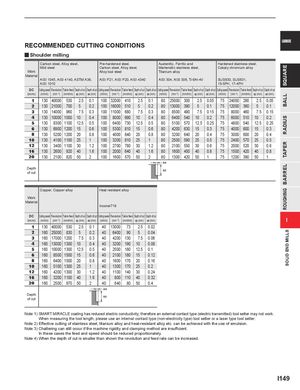
RECOMMENDED CUTTING CONDITIONS CARBIDE
y Shoulder milling
| Work Material | Carbo Mild st | n steel, A eel | lloy ste | el, | Pre-ha Carbo Alloy t | rdened n steel, A ool steel | steel, lloy st | eel, | Austen Marten Titaniu | itic, Fer sitic sta m alloy | ritic an inless s | d teel, | Harde Cobaly | ned stai chromi | nless s um allo | teel, y | ||||
| AISI 1 AISI 1 | 045, AIS 010 | I 4140, | ASTM A | 36, | AISI P | 21, AISI | P20, A | ISI 4340 | AISI 3 | 04, AISI | 306, Ti | -6Al-4V | SUS63 15-5P | 0, SUS H, 17-4P | 631, H | |||||
| DC | Cutting speed | Revolution | Table feed | Depth of cut | Depth of cut | Cutting speed | Revolution | Table feed | Depth of cut | Depth of cut | Cutting speed | Revolution | Table feed | Depth of cut | Depth of cut | Cutting speed | Revolution | Table feed | Depth of cut | Depth of cut |
| (mm) | (m/min) | (min-1) | (mm/min) | ap (mm) | ae (mm) | (m/min) | (min-1) | (mm/min) | ap (mm) | ae (mm) | (m/min) | (min-1) | (mm/min) | ap (mm) | ae (mm) | (m/min) | (min-1) | (mm/min) | ap (mm) | ae (mm) |
| 1 | 130 | 40000 | 530 | 2.5 | 0.1 | 100 | 32000 | 410 | 2.5 | 0.1 | 80 | 25000 | 300 | 2.5 | 0.05 | 75 | 24000 | 290 | 2.5 | 0.05 |
| 2 | 130 | 21000 | 700 | 5 | 0.2 | 100 | 16000 | 510 | 5 | 0.2 | 80 | 13000 | 390 | 5 | 0.1 | 75 | 12000 | 360 | 5 | 0.1 |
| 3 | 130 | 14000 | 960 | 7.5 | 0.3 | 100 | 11000 | 680 | 7.5 | 0.3 | 80 | 8500 | 490 | 7.5 | 0.15 | 75 | 8000 | 460 | 7.5 | 0.15 |
| 4 | 130 | 10000 | 1000 | 10 | 0.4 | 100 | 8000 | 690 | 10 | 0.4 | 80 | 6400 | 540 | 10 | 0.2 | 75 | 6000 | 510 | 10 | 0.2 |
| 5 | 130 | 8300 | 1100 | 12.5 | 0.5 | 100 | 6400 | 730 | 12.5 | 0.5 | 80 | 5100 | 570 | 12.5 | 0.25 | 75 | 4800 | 540 | 12.5 | 0.25 |
| 6 | 130 | 6900 | 1200 | 15 | 0.6 | 100 | 5300 | 810 | 15 | 0.6 | 80 | 4200 | 630 | 15 | 0.3 | 75 | 4000 | 600 | 15 | 0.3 |
| 8 | 130 | 5200 | 1200 | 20 | 0.8 | 100 | 4000 | 840 | 20 | 0.8 | 80 | 3200 | 640 | 20 | 0.4 | 75 | 3000 | 600 | 20 | 0.4 |
| 10 | 130 | 4100 | 1100 | 25 | 1 | 100 | 3200 | 810 | 25 | 1 | 80 | 2500 | 590 | 25 | 0.5 | 75 | 2400 | 570 | 25 | 0.5 |
| 12 | 130 | 3400 | 1100 | 30 | 1.2 | 100 | 2700 | 780 | 30 | 1.2 | 80 | 2100 | 550 | 30 | 0.6 | 75 | 2000 | 520 | 30 | 0.6 |
| 16 | 130 | 2600 | 920 | 40 | 1.6 | 100 | 2000 | 640 | 40 | 1.6 | 80 | 1600 | 450 | 40 | 0.8 | 75 | 1500 | 420 | 40 | 0.8 |
| 20 | 130 | 2100 | 820 | 50 | 2 | 100 | 1600 | 570 | 50 | 2 | 80 | 1300 | 420 | 50 | 1 | 75 | 1200 | 390 | 50 | 1 |
| ae | ||||||||||||||||||||
| Depth of cut | ap |
| Work Material | Coppe | r, Coppe | r alloy | Heat re Incone | sistant l718 | alloy | ||||
| DC (mm) | Cutting speed (m/min) | Revolution (min-1) | Table feed (mm/min) | Depth of cut ap (mm) | Depth of cut ae (mm) | Cutting speed (m/min) | Revolution (min-1) | Table feed (mm/min) | Depth of cut ap (mm) | Depth of cut ae (mm) |
| 1 | 130 | 40000 | 530 | 2.5 | 0.1 | 40 | 13000 | 73 | 2.5 | 0.02 |
| 2 | 160 | 25000 | 830 | 5 | 0.2 | 40 | 6400 | 90 | 5 | 0.04 |
| 3 | 160 | 17000 | 1200 | 7.5 | 0.3 | 40 | 4200 | 130 | 7.5 | 0.06 |
| 4 | 160 | 13000 | 1300 | 10 | 0.4 | 40 | 3200 | 190 | 10 | 0.08 |
| 5 | 160 | 10000 | 1300 | 12.5 | 0.5 | 40 | 2500 | 180 | 12.5 | 0.1 |
| 6 | 160 | 8500 | 1500 | 15 | 0.6 | 40 | 2100 | 180 | 15 | 0.12 |
| 8 | 160 | 6400 | 1500 | 20 | 0.8 | 40 | 1600 | 170 | 20 | 0.16 |
| 10 | 160 | 5100 | 1300 | 25 | 1 | 40 | 1300 | 170 | 25 | 0.2 |
| 12 | 160 | 4200 | 1300 | 30 | 1.2 | 40 | 1100 | 140 | 30 | 0.24 |
| 16 | 160 | 3200 | 1100 | 40 | 1.6 | 40 | 800 | 110 | 40 | 0.32 |
| 20 | 160 | 2500 | 970 | 50 | 2 | 40 | 640 | 80 | 50 | 0.4 |
| ae | ||||||||||
| Depth of cut | ap |
Note 1) SMART MIRACLE coating has reduced electric conductivity; therefore an external contact type (electric transmitted) tool setter may not work. When measuring the tool length, please use an internal contact type (non-electricity type) tool setter or a laser type tool setter. Note 2) Effective cutting of stainless steel, titanium alloy and heat-resistant alloy etc. can be achieved with the use of emulsion. Note 3) Chattering can still occur if the machine rigidity and clamping method are insufficient. In these cases the feed and speed should be reduced proportionately. Note 4) When the depth of cut is smaller than shown the revolution and feed rate can be increased.