Общий каталог Mitsubishi 2020 - 2021 - страница 906
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
CARBIDE
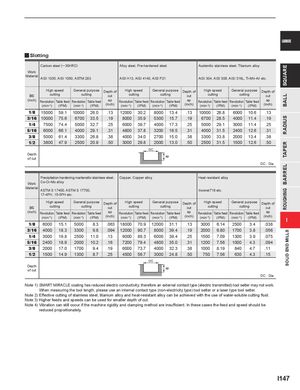
y Slotting
| Work Material | Carbon st AISI 1035 | eel(─30H , AISI 105 | RC) 0, ASTM 2 | 83 | Alloy stee AISI H13, | l, Pre-har AISI 4140 | dened steel , AISI P21 | Austenitic AISI 304, | stainless AISI 306, | steel, Tita AISI 316L, | nium alloy Ti-6Al-4V | etc. | |||
| DC | High s cutt | peed ing | General cutt | purpose ing | Depth of cut | High cut | speed ting | General cutti | purpose ng | Depth of cut | High s cutt | peed ing | General cutt | purpose ing | Depth of cut |
| (inch) | Revolution | Table feed | Revolution | Table feed | ap | Revolution | Table feed | Revolution | Table feed | ap | Revolution | Table feed | Revolution | Table feed | ap |
| (min-1) | (IPM) | (min-1) | (IPM) | (inch) | (min-1) | (IPM) | (min-1) | (IPM) | (inch) | (min-1) | (IPM) | (min-1) | (IPM) | (inch) | |
| 1/8 | 15000 | 59.1 | 10000 | 26.0 | .13 | 12000 | 30.2 | 8000 | 13.4 | .13 | 10000 | 26.8 | 6000 | 10.6 | .13 |
| 3/16 | 10000 | 75.6 | 6700 | 33.5 | .19 | 8000 | 35.9 | 5300 | 15.7 | .19 | 6700 | 28.5 | 4000 | 11.4 | .19 |
| 1/4 | 7500 | 74.4 | 5000 | 32.7 | .25 | 6000 | 39.7 | 4000 | 17.3 | .25 | 5000 | 29.1 | 3000 | 11.4 | .25 |
| 5/16 | 6000 | 66.1 | 4000 | 29.1 | .31 | 4800 | 37.8 | 3200 | 16.5 | .31 | 4000 | 31.5 | 2400 | 12.6 | .31 |
| 3/8 | 5000 | 61.4 | 3300 | 26.8 | .38 | 4000 | 34.0 | 2700 | 15.0 | .38 | 3300 | 33.8 | 2000 | 13.4 | .38 |
| 1/2 | 3800 | 47.9 | 2500 | 20.9 | .50 | 3000 | 29.8 | 2000 | 13.0 | .50 | 2500 | 31.5 | 1500 | 12.6 | .50 |
| Depth of cut | a DC | p | |||||||||||||
| Work | Precipitati Co-Cr-Mo | on hardeni alloy | ng martens | itic stainles | s steel, | Copper, C | opper allo | y | Heat resi | stant alloy | DC : Dia. | ||||
| Material | ASTM S 1 17-4PH, 1 | 7400, AS 5-5PH et | TM S 1770 c. | 0, | Inconel71 | 8 etc. | |||||||||
| High s | peed | General | purpose | Depth of | High | speed | General | purpose | Depth of | High s | peed | General | purpose | Depth of | |
| DC | cutt | ing | cutt | ing | cut | cut | ting | cutti | ng | cut | cutt | ing | cutt | ing | cut |
| (inch) | Revolution | Table feed | Revolution | Table feed | ap | Revolution | Table feed | Revolution | Table feed | ap | Revolution | Table feed | Revolution | Table feed | ap |
| (min-1) | (IPM) | (min-1) | (IPM) | (inch) | (min-1) | (IPM) | (min-1) | (IPM) | (inch) | (min-1) | (IPM) | (min-1) | (IPM) | (inch) | |
| 1/8 | 6000 | 15.1 | 5000 | 8.3 | .063 | 18000 | 70.9 | 12000 | 31.1 | .13 | 3000 | 6.14 | 2500 | 3.4 | .038 |
| 3/16 | 4000 | 18.3 | 3300 | 9.8 | .094 | 12000 | 90.7 | 8000 | 39.4 | .19 | 2000 | 6.80 | 1700 | 3.8 | .056 |
| 1/4 | 3000 | 19.8 | 2500 | 11.0 | .13 | 9000 | 89.3 | 6000 | 39.4 | .25 | 1500 | 7.09 | 1300 | 3.9 | .075 |
| 5/16 | 2400 | 18.9 | 2000 | 10.2 | .16 | 7200 | 79.4 | 4800 | 35.0 | .31 | 1200 | 7.56 | 1000 | 4.3 | .094 |
| 3/8 | 2000 | 17.0 | 1700 | 9.4 | .19 | 6000 | 73.7 | 4000 | 32.3 | .38 | 1000 | 8.19 | 840 | 4.7 | .11 |
| 1/2 | 1500 | 14.9 | 1300 | 8.7 | .25 | 4500 | 56.7 | 3000 | 24.8 | .50 | 750 | 7.56 | 630 | 4.3 | .15 |
| Depth of cut | a DC | p |
DC : Dia. Note 1) SMART MIRACLE coating has reduced electric conductivity; therefore an external contact type (electric transmitted) tool setter may not work. When measuring the tool length, please use an internal contact type (non-electricity type) tool setter or a laser type tool setter. Note 2) Effective cutting of stainless steel, titanium alloy and heat-resistant alloy can be achieved with the use of water-soluble cutting fluid. Note 3) Higher feeds and speeds can be used for smaller depth of cut. Note 4) Vibration can still occur if the machine rigidity and clamping method are insufficient. In these cases the feed and speed should be reduced proportionately.