Общий каталог Mitsubishi 2020 - 2021 - страница 892
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
CARBIDE
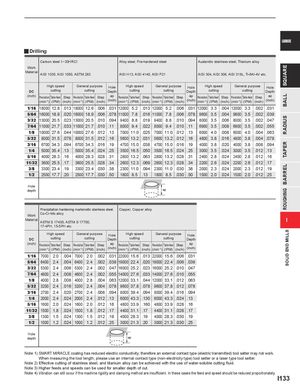
y Drilling
| Work Material | Carbon AISI 10 | steel 35, AI | (─30HR SI 1050 | C) , ASTM | 283 | Alloy s AISI H | teel, Pr 13, AIS | e-hard I 4140, | ened steel AISI P21 | Austeni AISI 30 | tic stai 4, AISI | nless s 306, A | teel, Tit ISI 316 | anium L, Ti-6A | alloy l-4V etc | . | ||||
| DC | Hi | gh spe cutting | ed | Gener c | al purp utting | ose | Hole Depth | Hi | gh spee cutting | d | General pur cutting | pose | Hole Depth | Hig c | h spe utting | ed | Gene | ral pur cutting | pose | Hole Depth |
| (inch) | Revolution | Table feed | Step | Revolution T | able feed | Step | ap | Revolution | Table feed | Step | Revolution Table feed | Step | ap | Revolution T | able feed | Step | Revolution | Table feed | Step | ap |
| (min-1) | (IPM) | (inch) | (min-1) | (IPM) | (inch) | (inch) | (min-1) | (IPM) | (inch) | (min-1) (IPM) | (inch) | (inch) | (min-1) | (IPM) | (inch) | (min-1) | (IPM) | (inch) | (inch) | |
| 1/16 | 18000 | 12.8 | .013 | 18000 | 12.6 | .006 | .031 | 12000 | 5.2 | .013 | 12000 5.2 | .006 | .031 | 12000 | 3.3 | .004 | 12000 | 3.3 | .002 | .031 |
| 5/64 | 16000 | 18.9 | .020 | 16000 | 18.9 | .006 | .078 | 11000 | 7.8 | .016 | 11000 7.8 | .006 | .078 | 9600 | 3.5 | .004 | 9600 | 3.5 | .002 | .039 |
| 3/32 | 13000 | 20.5 | .023 | 13000 | 20.5 | .010 | .094 | 9400 | 8.8 | .019 | 9400 8.8 | .010 | .094 | 8000 | 3.5 | .006 | 8000 | 3.5 | .002 | .047 |
| 7/64 | 11000 | 21.7 | .033 | 11000 | 21.7 | .010 | .11 | 8000 | 9.4 | .022 | 8000 9.4 | .010 | .11 | 6900 | 3.5 | .008 | 6900 | 3.5 | .002 | .055 |
| 1/8 | 10000 | 27.6 | .044 | 10000 | 27.6 | .012 | .13 | 7000 | 11.0 | .025 | 7000 11.0 | .012 | .13 | 6000 | 4.0 | .008 | 6000 | 4.0 | .004 | .063 |
| 5/32 | 8000 | 31.5 | .078 | 8000 | 31.5 | .012 | .16 | 5600 | 13.2 | .031 | 5600 13.2 | .012 | .16 | 4800 | 3.8 | .016 | 4800 | 3.8 | .004 | .078 |
| 3/16 | 6700 | 34.3 | .094 | 6700 | 34.3 | .016 | .19 | 4700 | 15.0 | .038 | 4700 15.0 | .016 | .19 | 4000 | 3.8 | .020 | 4000 | 3.8 | .008 | .094 |
| 1/4 | 5000 | 35.4 | .13 | 5000 | 35.4 | .024 | .25 | 3500 | 16.5 | .050 | 3500 16.5 | .024 | .25 | 3000 | 3.5 | .024 | 3000 | 3.5 | .012 | .13 |
| 5/16 | 4000 | 28.3 | .16 | 4000 | 28.3 | .028 | .31 | 2800 | 13.2 | .063 | 2800 13.2 | .028 | .31 | 2400 | 2.8 | .024 | 2400 | 2.8 | .012 | .16 |
| 11/32 | 3600 | 25.5 | .17 | 3600 | 25.5 | .028 | .34 | 2600 | 12.3 | .069 | 2600 12.3 | .028 | .34 | 2200 | 2.6 | .024 | 2200 | 2.6 | .012 | .17 |
| 3/8 | 3300 | 23.4 | .19 | 3300 | 23.4 | .030 | .38 | 2300 | 11.0 | .094 | 2300 11.0 | .030 | .38 | 2000 | 2.3 | .024 | 2000 | 2.3 | .012 | .19 |
| 1/2 | 2500 | 17.7 | .20 | 2500 | 17.7 | .030 | .50 | 1800 | 8.5 | .13 | 1800 8.5 | .030 | .50 | 1500 | 2.0 | .024 | 1500 | 2.0 | .012 | .25 |
| Hole | a | |||||||||||||||||||
| depth | p | |||||||||||||||||||
| Work | Precipit Co-Cr- | ation h Mo allo | ardenin y | g marten | sitic sta | inless s | teel, | Coppe | r, Copp | er alloy | ||||||||||
| Material | ASTM 17-4PH | S 1740 , 15-5 | 0, AST PH etc. | M S 177 | 00, | |||||||||||||||
| Hi | gh spe | ed | Gener | al purp | ose | Hole | Hi | gh spee | d | General pur | pose | Hole | ||||||||
| DC | cutting | c | utting | Depth | cutting | cutting | Depth | |||||||||||||
| (inch) | Revolution (min-1) | Table feed (IPM) | Step (inch) | Revolution (min-1) T | able feed (IPM) | Step (inch) | ap (inch) | Revolution (min-1) | Table feed (IPM) | Step (inch) | Revolution (min-1) Table feed (IPM) | Step (inch) | ap (inch) | |||||||
| 1/16 | 7000 | 2.0 | .004 | 7000 | 2.0 | .002 | .031 | 22000 | 15.6 | .013 | 22000 15.6 | .006 | .031 | |||||||
| 5/64 | 6400 | 2.4 | .004 | 6400 | 2.4 | .002 | .039 | 19000 | 22.4 | .020 | 19000 22.4 | .006 | .039 | |||||||
| 3/32 | 5300 | 2.4 | .006 | 5300 | 2.4 | .002 | .047 | 16000 | 25.2 | .023 | 16000 25.2 | .010 | .047 | |||||||
| 7/64 | 4600 | 2.4 | .008 | 4600 | 2.4 | .002 | .055 | 14000 | 27.6 | .033 | 14000 27.6 | .010 | .055 | |||||||
| 1/8 | 4000 | 2.8 | .008 | 4000 | 2.8 | .004 | .063 | 12000 | 33.1 | .044 | 12000 33.1 | .012 | .063 | |||||||
| 5/32 | 3200 | 2.4 | .016 | 3200 | 2.4 | .004 | .078 | 9600 | 37.8 | .078 | 9600 37.8 | .012 | .078 | |||||||
| 3/16 | 2700 | 2.4 | .020 | 2700 | 2.4 | .008 | .094 | 8000 | 39.4 | .094 | 8000 39.4 | .016 | .094 | |||||||
| 1/4 | 2000 | 2.4 | .024 | 2000 | 2.4 | .012 | .13 | 6000 | 43.3 | .130 | 6000 43.3 | .024 | .13 | |||||||
| 5/16 | 1600 | 2.0 | .024 | 1600 | 2.0 | .012 | .16 | 4800 | 33.9 | .160 | 4800 33.9 | .028 | .16 | |||||||
| 11/32 | 1500 | 1.8 | .024 | 1500 | 1.8 | .012 | .17 | 4400 | 31.1 | .17 | 4400 31.1 | .028 | .17 | |||||||
| 3/8 | 1300 | 1.5 | .024 | 1300 | 1.5 | .012 | .19 | 4000 | 28.3 | .19 | 4000 28.3 | .030 | .19 | |||||||
| 1/2 | 1000 | 1.2 | .024 | 1000 | 1.2 | .012 | .25 | 3000 | 21.3 | .20 | 3000 21.3 | .030 | .25 | |||||||
| Hole | ||||||||||||||||||||
| depth | a | p |
Note 1) SMART MIRACLE coating has reduced electric conductivity; therefore an external contact type (electric transmitted) tool setter may not work. Note 2) Effective cutting of stainless steel, and titanium alloy can be achieved with the use of water-soluble cutting fluid. Note 4) Vibration can still occur if the machine rigidity and clamping method are insufficient. In these cases the feed and speed should be reduced proportionately. I133