Общий каталог Mitsubishi 2020 - 2021 - страница 891
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
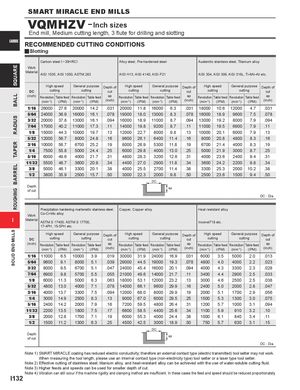
VQMHZV - Inch sizes
CARBIDE RECOMMENDED CUTTING CONDITIONS
y Slotting
| Work Material | Carbon st AISI 1035 | eel(─30H , AISI 105 | RC) 0, ASTM 2 | 83 | Alloy stee AISI H13 | l, Pre-har , AISI 414 | dened stee 0, AISI P21 | l | Austenitic AISI 304, | stainless AISI 306, | steel, Tita AISI 316L | nium alloy , Ti-6Al-4V | etc. | ||
| DC | High s cutt | peed ing | General cutt | purpose ing | Depth of cut | High cut | speed ting | General cutt | purpose ing | Depth of cut | High s cutt | peed ing | General cut | purpose ting | Depth of cut |
| (inch) | Revolution (min-1) | Table feed (IPM) | Revolution (min-1) | Table feed (IPM) | ap (inch) | Revolution (min-1) | Table feed (IPM) | Revolution (min-1) | Table feed (IPM) | ap (inch) | Revolution (min-1) | Table feed (IPM) | Revolution (min-1) | Table feed (IPM) | ap (inch) |
| 1/16 | 26000 | 27.6 | 20000 | 14.2 | .031 | 20000 | 11.8 | 16000 | 6.3 | .031 | 18000 | 10.6 | 12000 | 4.7 | .031 |
| 5/64 | 24000 | 36.9 | 16000 | 16.1 | .078 | 19000 | 18.0 | 13000 | 8.3 | .078 | 16000 | 18.9 | 9600 | 7.5 | .078 |
| 3/32 | 20000 | 37.8 | 13000 | 16.1 | .094 | 16000 | 18.9 | 11000 | 8.7 | .094 | 13000 | 19.2 | 8000 | 7.9 | .094 |
| 7/64 | 17000 | 40.2 | 11000 | 17.3 | .11 | 14000 | 19.8 | 9200 | 8.7 | .11 | 11000 | 19.5 | 6900 | 7.9 | .11 |
| 1/8 | 15000 | 44.3 | 10000 | 19.7 | .13 | 12000 | 22.7 | 8000 | 9.8 | .13 | 10000 | 20.1 | 6000 | 7.9 | .13 |
| 5/32 | 12000 | 56.7 | 8000 | 24.8 | .16 | 9600 | 26.1 | 6400 | 11.4 | .16 | 8000 | 20.8 | 4800 | 8.3 | .16 |
| 3/16 | 10000 | 56.7 | 6700 | 25.2 | .19 | 8000 | 26.9 | 5300 | 11.8 | .19 | 6700 | 21.4 | 4000 | 8.3 | .19 |
| 1/4 | 7500 | 55.8 | 5000 | 24.4 | .25 | 6000 | 29.8 | 4000 | 13.0 | .25 | 5000 | 21.9 | 3000 | 8.7 | .25 |
| 5/16 | 6000 | 49.6 | 4000 | 21.7 | .31 | 4800 | 28.3 | 3200 | 12.6 | .31 | 4000 | 23.6 | 2400 | 9.4 | .31 |
| 11/32 | 5500 | 48.7 | 3600 | 20.9 | .34 | 4400 | 27.0 | 2900 | 11.8 | .34 | 3600 | 24.2 | 2200 | 9.8 | .34 |
| 3/8 | 5000 | 46.1 | 3300 | 20.1 | .38 | 4000 | 25.5 | 2700 | 11.4 | .38 | 3300 | 25.3 | 2000 | 10.2 | .38 |
| 1/2 | 3800 | 35.9 | 2500 | 15.7 | .50 | 3000 | 22.3 | 2000 | 9.8 | .50 | 2500 | 23.6 | 1500 | 9.4 | .50 |
| DC | |||||||||||||||
| Depth of cut | ap |
DC : Dia.
| Work Material | Precipitati Co-Cr-Mo ASTM S 17-4PH, 1 | on harden alloy 17400, AS 5-5PH et | ing martens TM S 1770 c. | itic stainle 0, | ss steel, | Copper, | Copper all | oy | Heat resi Inconel71 | stant alloy 8 etc. | |||||
| DC | High s cutt | peed ing | General cutt | purpose ing | Depth of cut | High cut | speed ting | General cut | purpose ting | Depth of cut | High cut | speed ting | General cut | purpose ting | Depth of cut |
| (inch) | Revolution (min-1) | Table feed (IPM) | Revolution (min-1) | Table feed (IPM) | ap (inch) | Revolution (min-1) | Table feed (IPM) | Revolution (min-1) | Table feed (IPM) | ap (inch) | Revolution (min-1) | Table feed (IPM) | Revolution (min-1) | Table feed (IPM) | ap (inch) |
| 1/16 | 11000 | 6.5 | 10000 | 3.9 | .019 | 30000 | 31.9 | 24000 | 16.9 | .031 | 6000 | 3.5 | 5000 | 2.0 | .013 |
| 5/64 | 9600 | 9.1 | 8000 | 5.1 | .039 | 29000 | 44.5 | 19000 | 19.3 | .078 | 4800 | 4.0 | 4000 | 2.2 | .023 |
| 3/32 | 8000 | 9.5 | 6700 | 5.1 | .047 | 24000 | 45.4 | 16000 | 20.1 | .094 | 4000 | 4.3 | 3300 | 2.3 | .028 |
| 7/64 | 6900 | 9.8 | 5700 | 5.5 | .055 | 21000 | 49.6 | 14000 | 21.7 | .11 | 3400 | 4.4 | 2900 | 2.5 | .033 |
| 1/8 | 6000 | 11.3 | 5000 | 6.3 | .063 | 18000 | 53.1 | 12000 | 23.2 | .13 | 3000 | 4.6 | 2500 | 2.5 | .038 |
| 5/32 | 4800 | 13.0 | 4000 | 7.1 | .078 | 14000 | 66.1 | 9600 | 29.9 | .16 | 2400 | 5.0 | 2000 | 2.8 | .047 |
| 3/16 | 4000 | 13.7 | 3300 | 7.5 | .094 | 12000 | 68.0 | 8000 | 29.9 | .19 | 2000 | 5.1 | 1700 | 2.9 | .056 |
| 1/4 | 3000 | 14.9 | 2500 | 8.3 | .13 | 9000 | 67.0 | 6000 | 29.5 | .25 | 1500 | 5.3 | 1300 | 3.0 | .075 |
| 5/16 | 2400 | 14.2 | 2000 | 7.9 | .16 | 7200 | 59.5 | 4800 | 26.4 | .31 | 1200 | 5.7 | 1000 | 3.1 | .094 |
| 11/32 | 2200 | 13.5 | 1800 | 7.5 | .17 | 6600 | 58.5 | 4400 | 25.6 | .34 | 1100 | 5.9 | 910 | 3.2 | .10 |
| 3/8 | 2000 | 12.8 | 1700 | 7.1 | .19 | 6000 | 55.3 | 4000 | 24.4 | .38 | 1000 | 6.1 | 840 | 3.4 | .11 |
| 1/2 | 1500 | 11.2 | 1300 | 6.3 | .25 | 4500 | 42.5 | 3000 | 18.9 | .50 | 750 | 5.7 | 630 | 3.1 | .15 |
| DC | |||||||||||||||
| Depth of cut | ap | DC : Dia. |
Note 1) SMART MIRACLE coating has reduced electric conductivity; therefore an external contact type (electric transmitted) tool setter may not work. Note 2) Effective cutting of stainless steel, titanium alloy, and heat-resistant alloy can be achieved with the use of water-soluble cutting fluid. I132 Note 4) Vibration can still occur if the machine rigidity and clamping method are insufficient. In these cases the feed and speed should be reduced proportionately.