Общий каталог Mitsubishi 2020 - 2021 - страница 890
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
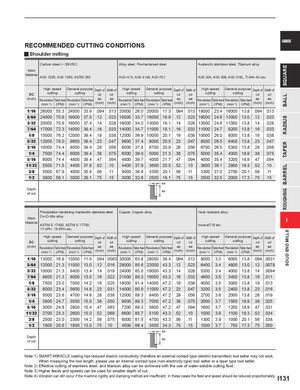
RECOMMENDED CUTTING CONDITIONS CARBIDE
y Shoulder milling
| Work Material | Carbon s AISI 103 | teel(─3 5, AISI 1 | 0HRC) 050, AST | M 283 | Alloy ste AISI H13 | el, Pre-h , AISI 4 | ardened 140, AISI | steel P21 | Austeniti AISI 304 | c stainle , AISI 30 | ss steel, T 6, AISI 31 | itanium 6L, Ti-6 | alloy Al-4V et | c. | ||||
| DC | High s cutti | peed ng | General p cutti | urpose ng | Depth of cut | Width of cut | High s cutti | peed ng | General cutt | purpose ing | Depth of cut | Width of cut | High s cutti | peed ng | General cutti | purpose ng | Depth of cut | Width of cut |
| (inch) | Revolution (min-1) | Table feed (IPM) | Revolution (min-1) | Table feed (IPM) | ap (inch) | ae (inch) | Revolution (min-1) | Table feed (IPM) | Revolution (min-1) | Table feed (IPM) | ap (inch) | ae (inch) | Revolution (min-1) | Table feed (IPM) | Revolution (min-1) | Table feed (IPM) | ap (inch) | ae (inch) |
| 1/16 | 26000 | 55.3 | 24000 | 33.9 | .094 | .013 | 20000 | 26.0 | 20000 | 17.3 | .094 | .013 | 18000 | 23.4 | 16000 | 13.8 | .094 | .013 |
| 5/64 | 24000 | 70.9 | 19000 | 37.0 | .12 | .023 | 19000 | 33.7 | 16000 | 18.9 | .12 | .023 | 16000 | 24.6 | 13000 | 13.0 | .12 | .023 |
| 3/32 | 20000 | 70.9 | 16000 | 37.4 | .14 | .028 | 16000 | 34.0 | 13000 | 18.1 | .14 | .028 | 13000 | 24.6 | 11000 | 13.8 | .14 | .028 |
| 7/64 | 17000 | 72.3 | 14000 | 39.4 | .16 | .033 | 14000 | 34.7 | 11000 | 18.1 | .16 | .033 | 11000 | 24.7 | 9200 | 13.8 | .16 | .033 |
| 1/8 | 15000 | 76.2 | 12000 | 39.4 | .19 | .038 | 12000 | 36.9 | 10000 | 20.1 | .19 | .038 | 10000 | 26.0 | 8000 | 13.8 | .19 | .038 |
| 5/32 | 12000 | 78.0 | 9600 | 39.4 | .23 | .047 | 9600 | 37.4 | 8000 | 20.5 | .23 | .047 | 8000 | 26.5 | 6400 | 13.8 | .23 | .047 |
| 3/16 | 10000 | 74.4 | 8000 | 39.4 | .28 | .056 | 8000 | 37.8 | 6700 | 20.9 | .28 | .056 | 6700 | 26.5 | 5300 | 13.8 | .28 | .056 |
| 1/4 | 7500 | 74.4 | 6000 | 39.4 | .38 | .075 | 6000 | 39.0 | 5000 | 21.3 | .38 | .075 | 5000 | 35.4 | 4000 | 18.9 | .38 | .075 |
| 5/16 | 6000 | 74.4 | 4800 | 39.4 | .47 | .094 | 4800 | 39.7 | 4000 | 21.7 | .47 | .094 | 4000 | 35.4 | 3200 | 18.9 | .47 | .094 |
| 11/32 | 5500 | 71.5 | 4400 | 37.8 | .52 | .10 | 4400 | 37.9 | 3600 | 20.5 | .52 | .10 | 3600 | 36.1 | 2900 | 19.3 | .52 | .10 |
| 3/8 | 5000 | 67.9 | 4000 | 35.8 | .56 | .11 | 4000 | 36.9 | 3300 | 20.1 | .56 | .11 | 3300 | 37.0 | 2700 | 20.1 | .56 | .11 |
| 1/2 | 3800 | 56.1 | 3000 | 29.1 | .75 | .15 | 3000 | 32.6 | 2500 | 18.1 | .75 | .15 | 2500 | 32.5 | 2000 | 17.3 | .75 | .15 |
| ae | ||||||||||||||||||
| Depth of cut | ap |
| Work Material | Precipitat Co-Cr-M ASTM S 17-4PH, | ion hard o alloy 17400, 15-5PH | ening mart ASTM S 1 etc. | ensitic s 7700, | tainless | steel, | Copper, | Copper | alloy | Heat resi Inconel7 | stant all 18 etc. | oy | ||||||
| DC | High s cutti | peed ng | General p cutti | urpose ng | Depth of cut | Width of cut | High s cutti | peed ng | General cutti | purpose ng | Depth of cut | Width of cut | High s cutti | peed ng | General cutti | purpose ng | Depth of cut | Width of cut |
| (inch) | Revolution (min-1) | Table feed (IPM) | Revolution (min-1) | Table feed (IPM) | ap (inch) | ae (inch) | Revolution (min-1) | Table feed (IPM) | Revolution (min-1) | Table feed (IPM) | ap (inch) | ae (inch) | Revolution (min-1) | Table feed (IPM) | Revolution (min-1) | Table feed (IPM) | ap (inch) | ae (inch) |
| 1/16 | 13000 | 16.9 | 13000 | 11.0 | .094 | .0063 | 30000 | 63.8 | 28000 | 39.4 | .094 | .013 | 8000 | 3.3 | 6000 | 13.8 | .094 | .0031 |
| 5/64 | 12000 | 21.3 | 11000 | 13.0 | .12 | .016 | 29000 | 85.6 | 22000 | 43.3 | .12 | .023 | 6400 | 3.4 | 4800 | 13.0 | .12 | .0078 |
| 3/32 | 10000 | 21.3 | 9400 | 13.4 | .14 | .019 | 24000 | 85.0 | 19000 | 43.3 | .14 | .028 | 5300 | 3.4 | 4000 | 13.8 | .14 | .0094 |
| 7/64 | 8600 | 21.3 | 8000 | 13.0 | .16 | .022 | 21000 | 89.3 | 16000 | 43.3 | .16 | .033 | 4600 | 3.5 | 3400 | 13.8 | .16 | .011 |
| 1/8 | 7500 | 23.0 | 7000 | 14.2 | .19 | .025 | 18000 | 91.4 | 14000 | 47.2 | .19 | .038 | 4000 | 3.5 | 3000 | 13.8 | .19 | .013 |
| 5/32 | 6000 | 23.4 | 5600 | 14.6 | .23 | .031 | 14000 | 90.9 | 11000 | 47.2 | .23 | .047 | 3200 | 3.5 | 2400 | 13.8 | .23 | .016 |
| 3/16 | 5000 | 23.6 | 4700 | 14.6 | .28 | .038 | 12000 | 89.3 | 9400 | 47.2 | .28 | .056 | 2700 | 3.6 | 2000 | 13.8 | .28 | .019 |
| 1/4 | 3800 | 24.7 | 3500 | 15.0 | .38 | .050 | 9000 | 89.3 | 7000 | 47.2 | .38 | .075 | 2000 | 3.7 | 1500 | 18.9 | .38 | .025 |
| 5/16 | 3000 | 24.8 | 2800 | 15.4 | .47 | .063 | 7200 | 89.3 | 5600 | 47.2 | .47 | .094 | 1600 | 3.7 | 1200 | 18.9 | .47 | .031 |
| 11/32 | 2700 | 23.3 | 2600 | 15.0 | .52 | .069 | 6600 | 85.7 | 5100 | 43.3 | .52 | .10 | 1500 | 3.9 | 1100 | 19.3 | .52 | .034 |
| 3/8 | 2500 | 23.0 | 2300 | 14.2 | .56 | .075 | 6000 | 81.5 | 4700 | 43.3 | .56 | .11 | 1300 | 3.9 | 1000 | 20.1 | .56 | .038 |
| 1/2 | 1900 | 20.6 | 1800 | 13.0 | .75 | .10 | 4500 | 66.4 | 3500 | 34.3 | .75 | .15 | 1000 | 3.7 | 750 | 17.3 | .75 | .050 |
| ae | ||||||||||||||||||
| Depth of cut | ap |
Note 2) Effective cutting of stainless steel, and titanium alloy can be achieved with the use of water-soluble cutting fluid. Note 4) Vibration can still occur if the machine rigidity and clamping method are insufficient. In these cases the feed and speed should be reduced proportionately. I131