Общий каталог Mitsubishi 2020 - 2021 - страница 882
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
CARBIDE
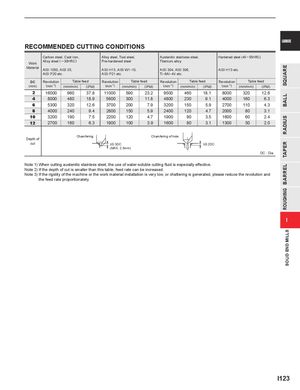
RECOMMENDED CUTTING CONDITIONS
| Work Material | Carbon stee Alloy steel( AISI 1050, A AISI P20 et | l, Cast iron, ─30HRC) ISI 35, c. | Alloy steel, Pre-hardene AISI H13, AI AISI P21 etc | Tool steel, d steel SI W1-10, . | Austenitic st Titanium allo AISI 304, AI Ti-6Al-4V e | ainless stee y SI 306, tc. | l, | Hardened ste AISI H13 etc | el (45─55HR . | C) | ||
| DC | Revolution | Table | feed | Revolution | Table | feed | Revolution | Tabl | e feed | Revolution | Table | feed |
| (mm) | (min-1) | (mm/min) | (IPM) | (min-1) | (mm/min) | (IPM) | (min-1) | (mm/min) | (IPM) | (min-1) | (mm/min) | (IPM) |
| 2 | 16000 | 960 | 37.8 | 11000 | 590 | 23.2 | 9500 | 460 | 18.1 | 8000 | 320 | 12.6 |
| 4 | 8000 | 480 | 18.9 | 5600 | 300 | 11.8 | 4800 | 230 | 9.1 | 4000 | 160 | 6.3 |
| 6 | 5300 | 320 | 12.6 | 3700 | 200 | 7.9 | 3200 | 150 | 5.9 | 2700 | 110 | 4.3 |
| 8 | 4000 | 240 | 9.4 | 2800 | 150 | 5.9 | 2400 | 120 | 4.7 | 2000 | 80 | 3.1 |
| 10 | 3200 | 190 | 7.5 | 2200 | 120 | 4.7 | 1900 | 90 | 3.5 | 1600 | 60 | 2.4 |
| 12 | 2700 | 160 | 6.3 | 1900 | 100 | 3.9 | 1600 | 80 | 3.1 | 1300 | 50 | 2.0 |
| Depth of cut | Cha | mfering | (MAX. | 2.5mm) C | Cha | mfering of hole |
DC : Dia. Note 1) When cutting austenitic stainless steel, the use of water-soluble cutting fluid is especially effective. Note 2) If the depth of cut is smaller than this table, feed rate can be increased. Note 3) If the rigidity of the machine or the work material installation is very low, or chattering is generated, please reduce the revolution and the feed rate proportionately.