Общий каталог Mitsubishi 2020 - 2021 - страница 857
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
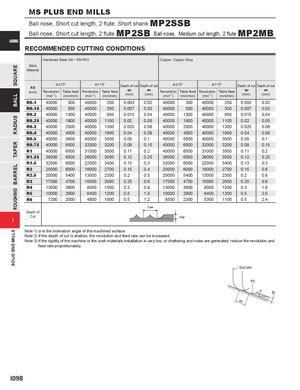
Ball nose, Short cut length, 2 flute, Short shank MP2SSB
Ball nose, Short cut length, 2 flute MP2SB Ball nose, Medium cut length, 2 flute MP2MB
CARBIDE
RECOMMENDED CUTTING CONDITIONS
| Work Material | Hardened S | teel (45─55 | HRC) | Copper, Co | pper Alloy | |||||||
| RE | % | 15° | %> | 15° | Depth of cut | Depth of cut | % | 15° | %> | 15° | Depth of cut | Depth of cut |
| (mm) | Revolution (min-1) | Table feed (mm/min) | Revolution (min-1) | Table feed (mm/min) | ap (mm) | ae (mm) | Revolution (min-1) | Table feed (mm/min) | Revolution (min-1) | Table feed (mm/min) | ap (mm) | ae (mm) |
| R0.1 | 40000 | 300 | 40000 | 250 | 0.003 | 0.02 | 40000 | 300 | 40000 | 250 | 0.003 | 0.02 |
| R0.15 | 40000 | 500 | 40000 | 350 | 0.007 | 0.03 | 40000 | 500 | 40000 | 350 | 0.007 | 0.03 |
| R0.2 | 40000 | 1300 | 40000 | 950 | 0.015 | 0.04 | 40000 | 1300 | 40000 | 950 | 0.015 | 0.04 |
| R0.25 | 40000 | 1900 | 40000 | 1100 | 0.02 | 0.05 | 40000 | 1900 | 40000 | 1100 | 0.02 | 0.05 |
| R0.3 | 40000 | 2500 | 40000 | 1300 | 0.025 | 0.06 | 40000 | 2500 | 40000 | 1300 | 0.025 | 0.06 |
| R0.4 | 40000 | 4000 | 40000 | 1900 | 0.04 | 0.08 | 40000 | 4000 | 40000 | 1900 | 0.04 | 0.08 |
| R0.5 | 40000 | 5600 | 40000 | 3000 | 0.05 | 0.1 | 40000 | 5600 | 40000 | 3000 | 0.05 | 0.1 |
| R0.75 | 40000 | 6500 | 32000 | 3200 | 0.08 | 0.15 | 40000 | 6500 | 32000 | 3200 | 0.08 | 0.15 |
| R1 | 40000 | 6500 | 31000 | 3500 | 0.11 | 0.2 | 40000 | 6500 | 31000 | 3500 | 0.11 | 0.2 |
| R1.25 | 36000 | 6500 | 26000 | 3500 | 0.12 | 0.25 | 36000 | 6500 | 26000 | 3500 | 0.12 | 0.25 |
| R1.5 | 32000 | 6000 | 22000 | 3400 | 0.13 | 0.3 | 32000 | 6000 | 22000 | 3400 | 0.13 | 0.3 |
| R2 | 25000 | 6000 | 16000 | 2700 | 0.15 | 0.4 | 25000 | 6000 | 16000 | 2700 | 0.15 | 0.6 |
| R2.5 | 20000 | 5400 | 13000 | 2300 | 0.2 | 0.5 | 20000 | 5400 | 13000 | 2300 | 0.2 | 0.8 |
| R3 | 17000 | 4700 | 10000 | 2000 | 0.25 | 0.6 | 17000 | 4700 | 10000 | 2000 | 0.25 | 0.9 |
| R4 | 13000 | 3600 | 8000 | 1500 | 0.3 | 0.8 | 13000 | 3600 | 8000 | 1500 | 0.3 | 1.6 |
| R5 | 10000 | 2900 | 6400 | 1200 | 0.5 | 1.0 | 10000 | 2900 | 6400 | 1200 | 0.5 | 2.0 |
| R6 | 7200 | 2000 | 4800 | 1000 | 0.5 | 1.2 | 8500 | 2300 | 5300 | 1100 | 0.5 | 2.4 |
| Depth of | ||||||||||||
| Cut |
I < Note 1) % is the inclination angle of the machined surface. Note 2) If the depth of cut is shallow, the revolution and feed rate can be increased. Note 3) If the rigidity of the machine or the work materials installation is very low, or chattering and noise are generated, reduce the revolution and feed rate proportionately.
End Mill
RE
ap ae