Общий каталог Mitsubishi 2020 - 2021 - страница 1400
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
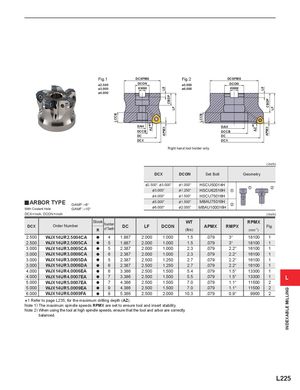
| Fig | .1 | DCSFMS | Fig.2 | DCSFMS | |||||||
| ø2. ø3. ø4. | LCCB 500 000 000 | KWW DCON 1 | L8 CBDP LF | ø5.000 ø6.000 | LCCB | KWW DCON | L8 | CBDP LF | |||
| AZ DCCB DC DCX DAH | APMX Right | hand tool ho | lder only. | DCCB DC DCX DAH | AZ 1 | APMX (inch) | |||||
| D | CX | DCON | Set Bolt | Geometry | |||||||
| &2.500 | ",&3.000" | &1.000" | HSCU5001 | 4H | |||||||
| &3 | .000" | &1.250" | HSCU6251 | z 6H | z | x | |||||
| &4 | .000" | &1.500" | HSCU7501 | 6H | |||||||
| y ARB | GAMP :‒6° OR TYPE | &5 | .000" | &1.500" | MBAU7501 | 6H x | |||||
| With Coola | GAMF :‒10° nt Hole | &6 | .000" | &2.000" | MBAU10001 | 6H | |||||
| DCX=inc | h, DCON=inch | (inch) | |||||||||
| Stock | WT | RPMX | |||||||||
| DCX | Order Number | R | Number of Teeth | DC | LF | DCON | (lbs) | APMX | RMPX | (min-1) | Fig. |
| 2.500 | WJX14UR2.5004CA | a | 4 | 1.887 | 2.000 | 1.000 | 1.5 | .079 | 3° | 18100 | 1 |
| 2.500 | WJX14UR2.5005CA | a | 5 | 1.887 | 2.000 | 1.000 | 1.5 | .079 | 3° | 18100 | 1 |
| 3.000 | WJX14UR3.0005CA | a | 5 | 2.387 | 2.000 | 1.000 | 2.3 | .079 | 2.2° | 16100 | 1 |
| 3.000 | WJX14UR3.0006CA | a | 6 | 2.387 | 2.000 | 1.000 | 2.3 | .079 | 2.2° | 16100 | 1 |
| 3.000 | WJX14UR3.0005DA | a | 5 | 2.387 | 2.500 | 1.250 | 2.7 | .079 | 2.2° | 16100 | 1 |
| 3.000 | WJX14UR3.0006DA | a | 6 | 2.387 | 2.500 | 1.250 | 2.7 | .079 | 2.2° | 16100 | 1 |
| 4.000 | WJX14UR4.0006EA | a | 6 | 3.386 | 2.500 | 1.500 | 5.4 | .079 | 1.5° | 13300 | 1 |
| 4.000 | WJX14UR4.0007EA | a | 7 | 3.386 | 2.500 | 1.500 | 5.5 | .079 | 1.5° | 13300 | 1 |
| 5.000 | WJX14UR5.0007EA | a | 7 | 4.386 | 2.500 | 1.500 | 7.0 | .079 | 1.1° | 11500 | 2 |
| 5.000 | WJX14UR5.0009EA | a | 9 | 4.386 | 2.500 | 1.500 | 7.0 | .079 | 1.1° | 11500 | 2 |
| 6.000 | WJX14UR6.0009FA | a | 9 | 5.386 | 2.500 | 2.000 | 10.3 | .079 | 0.9° | 9900 | 2 |
*1 Refer to page L235, for the maximum drilling depth (AZ). Note 1) The maximum spindle speeds RPMX are set to ensure tool and insert stability. Note 2) When using the tool at high spindle speeds, ensure that the tool and arbor are correctly balanced.