Общий каталог Mitsubishi 2020 - 2021 - страница 1378
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
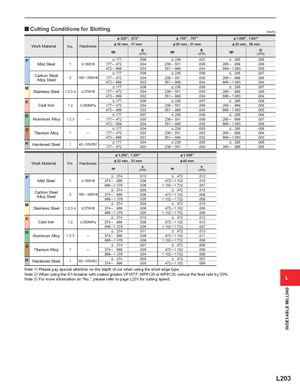
y Cutting Conditions for Slotting
| (inch) | |||||||||
| &.625", . | 672" | &.750", | .797" | &1.000", | 1.047" | ||||
| &16 mm | 17 mm | &20 mm | 21 mm | &25 mm | 26 mm | ||||
| Work Material | No | Hardness | , | , | , | ||||
| . | ap | fr (IPR) | ap | fr (IPR) | ap | fr (IPR) | |||
| P | .006 | .007 | .008 | ||||||
| Mild Steel | 1 | .177─.472 | .004 | .236─.551 | .006 | .295─.669 | .006 | ||
| .472─.669 | .003 | .551─.866 | .004 | .669─1.063 | .005 | ||||
| Cb Stl | .006 | .006 | .007 | ||||||
| aron ee Alloy Steel | 2 | 180─350HB | .177─.472 | .004 | .236─.551 | .005 | .295─.669 | .006 | |
| .472─.669 | .002 | .551─.866 | .004 | .669─1.063 | .004 | ||||
| M | .006 | .006 | .007 | ||||||
| Stainless Steel | 1,2,3,4 | .177─.472 | .004 | .236─.551 | .005 | .295─.669 | .006 | ||
| .472─.669 | .002 | .551─.866 | .004 | .669─1.063 | .004 | ||||
| K | .006 | .007 | .008 | ||||||
| Cast Iron | 1,2 | .177─.472 | .004 | .236─.551 | .006 | .295─.669 | .006 | ||
| .472─.669 | .003 | .551─.866 | .004 | .669─1.063 | .005 | ||||
| N | .007 | .008 | .009 | ||||||
| Aluminum Alloy | 1,2,3 | ─ | .177─.472 | .005 | .236─.551 | .006 | .295─.669 | .007 | |
| .472─.669 | .004 | .551─.866 | .005 | .669─1.063 | .006 | ||||
| S | .004 | .005 | .006 | ||||||
| Titanium Alloy | 1 | ─ | .177─.472 | .002 | .236─.551 | .003 | .295─.669 | .004 | |
| .472─.669 | .001 | .551─.866 | .002 | .669─1.063 | .003 | ||||
| H | Hardened Steel | 1 | 40─55HRC | .004 | .005 | .006 | |||
| .177─.472 | .003 | .236─.551 | .004 | .295─.669 | .005 | ||||
| &1.250", | 1.297" | &1.50 | 0" | ||||||
| Work Material | No. | Hardness | &32 mm, | 33 mm | &40 m | m | |||
| ap | fr (IPR) | ap | fr (IPR) | ||||||
| P | .010 | .012 | |||||||
| Mild Steel | 1 | .374─.866 | .008 | .472─1.102 | .010 | ||||
| .866─1.378 | .006 | 1.102─1.732 | .007 | ||||||
| .008 | .010 | ||||||||
| Carbon Steel | 2 | 180─350HB | .374─.866 | .006 | .472─1.102 | .008 | |||
| Alloy Steel | .866─1.378 | .005 | 1.102─1.732 | .006 | |||||
| M | .008 | .010 | |||||||
| Stainless Steel | 1,2,3,4 | .374─.866 | .006 | .472─1.102 | .008 | ||||
| .866─1.378 | .005 | 1.102─1.732 | .006 | ||||||
| K | .010 | .012 | |||||||
| Cast Iron | 1,2 | .374─.866 | .008 | .472─1.102 | .010 | ||||
| .866─1.378 | .006 | 1.102─1.732 | .007 | ||||||
| N | .011 | .013 | |||||||
| Aluminum Alloy | 1,2,3 | ─ | .374─.866 | .009 | .472─1.102 | .011 | |||
| .866─1.378 | .006 | 1.102─1.732 | .008 | ||||||
| S | .007 | .009 | |||||||
| Titanium Alloy | 1 | ─ | .374─.866 | .005 | .472─1.102 | .008 | |||
| .866─1.378 | .004 | 1.102─1.732 | .006 | ||||||
| H | .006 | .007 | |||||||
| Hardened Steel | 1 | 40─55HRC | .374─.866 | .005 | .472─1.102 | .006 |
Note 1) Please pay special attention on the depth of cut when using the short edge type.
Note 2) When using the G1-breaker wiht coated grades VP15TF, MP6120 or MP9120, reduce the feed rate by 20%. L
Note 3) For more information on "No.", please refer to page L201 for cutting speed.