Общий каталог Mitsubishi 2020 - 2021 - страница 1347
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
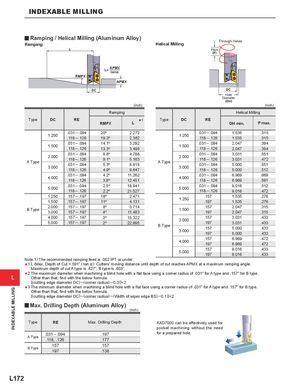
y Ramping / Helical Milling (Aluminum Alloy)
Ramping L
L= APMX tan % RMPX APMX DC
Helical Milling
Through Holes Pitch (P)
DC Hole Diameter (DH)
| Ramp | ing (inch) | |||
| Type | DC | RE | RMPX | 1 L |
| 250 | .031─.094 | 20º | 2.272 | |
| . | .118─.126 | 19.3º | 2.362 | |
| 500 | .031─.094 | 14.1º | 3.292 | |
| . | .118─.126 | 13.3º | 3.498 | |
| 000 | .031─.094 | 9.8º | 4.788 | |
| . | .118─.126 | 9.1º | 5.163 | |
| A Type | 000 | .031─.094 | 5.3º | 8.915 |
| . | .118─.126 | 4.9º | 9.647 | |
| .031─.094 | 4.2º | 11.262 | ||
| .000 | .118─.126 | 3.8º | 12.451 | |
| 000 | .031─.094 | 2.5º | 18.941 | |
| . | .118─.126 | 2.2º | 21.527 | |
| 1.250 | .157─.197 | 18º | 2.471 | |
| 1.500 | .157─.197 | 11º | 4.131 | |
| 2.000 | .157─.197 | 8º | 5.714 | |
| B Type | 3.000 | .157─.197 | 4º | 11.483 |
| 4.000 | .157─.197 | 3º | 15.322 | |
| 5.000 | .157─.197 | 2º | 22.995 |
| Helical M | illing | |||
| Type | DC | RE | ||
| DH min. | P max. | |||
| 1250 | .031─.094 | 1.535 | .315 | |
| . | .118─.126 | 1.535 | .315 | |
| 1500 | .031─.094 | 2.047 | .394 | |
| . | .118─.126 | 2.047 | .394 | |
| 2000 | .031─.094 | 3.031 | .551 | |
| A T | . | .118─.126 | 3.031 | .472 |
| ype | 000 | .031─.094 | 5.000 | .551 |
| . | .118─.126 | 5.000 | .512 | |
| 000 | .031─.094 | 6.969 | .669 | |
| . | .118─.126 | 6.969 | .591 | |
| 5000 | .031─.094 | 9.016 | .512 | |
| . | .118─.126 | 9.016 | .472 | |
| 1250 | .157 | 1.535 | .276 | |
| . | .197 | 1.535 | .276 | |
| 1500 | .157 | 2.047 | .315 | |
| . | .197 | 2.047 | .315 | |
| 2000 | .157 | 3.031 | .433 | |
| B T | . | .197 | 3.031 | .433 |
| ype | 000 | .157 | 5.000 | .433 |
| . | .197 | 5.000 | .433 | |
| 000 | .157 | 6.969 | .472 | |
| . | .197 | 6.969 | .472 | |
| 5000 | .157 | 9.016 | .433 | |
| . | .197 | 9.016 | .433 |
Note 1) The recommended ramping feed is .002 IPT or under.*
1 L (Max. Depth of Cut =.591" / tan %). Cutters' moving distance until depth of cut reaches APMX at a maximum ramping angle.
Maximum depth of cut A type is .827", B type is .803".*
L 2 The maximum diameter when machining a blind hole with a flat face using a corner radius of .031" for A type and .157" for B type. Other than that, find with the below formula. {(cutting edge diameter DC) ─(corner radius) ─0.3)}×2 *3 The minimum diameter when machining a blind hole with a flat face using a corner radius of .031" for A type and .157" for B type. Other than that, find with the below formula. {(cutting edge diameter DC) ─(corner radius) ─(Width of wiper edge BS) ─ 0.1)}×2
y Max. Drilling Depth (Aluminum Alloy)
(inch)
| Type | RE | Max. Drilling Depth |
| A T | .031─.094 | .197 |
| ype | .118,.126 | .177 |
| B T | .157 | .157 |
| ype | .197 | .138 |
pocket machining without the need