Общий каталог Mitsubishi 2020 - 2021 - страница 1348
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
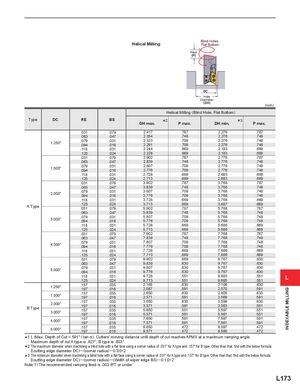
Helical Milling Blind Holes, Flat Bottom Pitch (P)
DC Hole Diameter (DH) (inch)
| Helical Milling (Blind | Hole, Flat Bottom) | |||||
| Type | DC | RE | BS | 2 DH max. P max. | 3 DH min. | P max. |
| .031 | .079 | 2.417 .787 | 2.276 | .787 | ||
| .063 | .047 | 2.354 .748 | 2.276 | .748 | ||
| 1250" | .079 | .031 | 2.323 .709 | 2.276 | .748 | |
| . | .094 | .016 | 2.291 .709 | 2.276 | .748 | |
| .118 | .031 | 2.244 .669 | 2.193 | .669 | ||
| .125 | .024 | 2.228 .669 | 2.193 | .669 | ||
| .031 | .079 | 2.902 .787 | 2.776 | .787 | ||
| .063 | .047 | 2.839 .748 | 2.776 | .748 | ||
| " | .079 | .031 | 2.807 .709 | 2.776 | .748 | |
| 1.500 | .094 | .016 | 2.776 .709 | 2.776 | .748 | |
| .118 | .031 | 2.728 .669 | 2.693 | .669 | ||
| .125 | .024 | 2.713 .669 | 2.693 | .669 | ||
| .031 | .079 | 3.902 .787 | 3.768 | .787 | ||
| .063 | .047 | 3.839 .748 | 3.768 | .748 | ||
| " | .079 | .031 | 3.807 .709 | 3.768 | .748 | |
| 2.000 | .094 | .016 | 3.776 .709 | 3.768 | .748 | |
| .118 | .031 | 3.728 .669 | 3.768 | .669 | ||
| .125 | .024 | 3.713 .669 | 3.687 | .669 | ||
| A Type | .031 | .079 | 5.902 .787 | 5.768 | .787 | |
| .063 | .047 | 5.839 .748 | 5.768 | .748 | ||
| " | .079 | .031 | 5.807 .709 | 5.768 | .748 | |
| 3.000 | .094 | .016 | 5.776 .709 | 5.768 | .748 | |
| .118 | .031 | 5.728 .669 | 5.686 | .669 | ||
| .125 | .024 | 5.713 .669 | 5.686 | .669 | ||
| .031 | .079 | 7.902 .787 | 7.768 | .787 | ||
| .063 | .047 | 7.839 .748 | 7.768 | .748 | ||
| " | .079 | .031 | 7.807 .709 | 7.768 | .748 | |
| 4.000 | .094 | .016 | 7.776 .709 | 7.768 | .748 | |
| .118 | .031 | 7.728 .669 | 7.686 | .669 | ||
| .125 | .024 | 7.713 .669 | 7.686 | .669 | ||
| .031 | .079 | 9.902 .669 | 9.767 | .630 | ||
| .063 | .047 | 9.839 .630 | 9.767 | .630 | ||
| " | .079 | .031 | 9.807 .630 | 9.767 | .630 | |
| 5.000 | .094 | .016 | 9.776 .630 | 9.767 | .630 | |
| .118 | .031 | 9.728 .551 | 9.685 | .551 | ||
| .125 | .024 | 9.713 .551 | 9.685 | .551 | ||
| " | .157 | .035 | 2.165 .630 | 2.106 | .630 | |
| 1.250 | .197 | .016 | 2.087 .591 | 2.070 | .591 | |
| " | .157 | .035 | 2.650 .630 | 2.605 | .630 | |
| 1.500 | .197 | .016 | 2.571 .591 | 2.569 | .591 | |
| " | .157 | .035 | 3.650 .630 | 3.599 | .630 | |
| 2.000 | .197 | .016 | 3.571 .591 | 3.563 | .591 | |
| B Type | 157 | 035 | 5.650 .551 | 5.597 | .551 | |
| 3.000" | . .197 | . .016 | 5.571 .551 | 5.561 | .551 | |
| " | .157 | .035 | 7.650 .591 | 7.597 | .591 | |
| 4.000 | .197 | .016 | 7.571 .591 | 7.561 | .591 | |
| 157 | 035 | 9650 472 | 9597 | 472 | ||
| 5.000" | . .197 | . .016 | . . 9.571 .472 | . 9.560 | . .472 |
*1 L (Max. Depth of Cut =.591" / tan %). Cutters' moving distance until depth of cut reaches APMX at a maximum ramping angle.
Maximum depth of cut A type is .827", B type is .803".*
2 The maximum diameter when machining a blind hole with a flat face using a corner radius of .031" for A type and .157" for B type. Other than that, find with the below formula. {(cutting edge diameter DC)─ (corner radius)─ 0.3)}×2 *3 The minimum diameter when machining a blind hole with a flat face using a corner radius of .031" for A type and .157" for B type. Other than that, find with the below formula. {(cutting edge diameter DC)─ (corner radius)─ (Width of wiper edge BS)─ 0.1)}×2 Note 1) The recommended ramping feed is .002 IPT or under.