Общий каталог Mitsubishi 2020 - 2021 - страница 1295
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
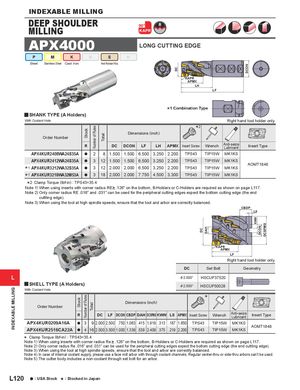
APX4000
LONG CUTTING EDGE
P M K N S H
Steel Stainless Steel Cast Iron Heat Resistant Alloy
KAPR APMX LH LF
*1 Combination Type
y SHANK TYPE (A Holders)
With Coolant Hole Right hand tool holder only.
*2
Dimensions (inch) Order Number
R DC DCON LF LH APMX Insert Screw Wrench Anti-seize Lubricant Insert Type
| APX4KUR2408WA24S35A | a | 2 | 8 1.500 1.500 6.500 3.250 2.200 TPS43 | TIP15W MK1KS | |
| APX4KUR2412WA24S35A | a | 3 12 1.500 1.500 6.500 3.250 2.200 | TPS43 | TIP15W MK1KS | |
| * | AOMT1848 | ||||
| 1 APX4KUR3212WA32S35A | 3 12 2.000 2.000 6.500 3.250 2.200 | TPS43 | TIP15W MK1KS | ||
| a | |||||
| *1 APX4KUR3218WA32M53A | 3 18 2.000 2.000 7.750 4.500 3.300 | TPS43 | TIP15W MK1KS |
a *2 Clamp Torque (lbf-in) : TPS43=35.4 Note 1) When using inserts with corner radius RE>.126" on the bottom, B-Holders or C-Holders are required as shown on page L117. Note 2) Only corner radius RE .016" and .031" can be used for the peripheral cutting edges expect the bottom cutting edge (the end
cuttting edge). Note 3) When using the tool at high spindle speeds, ensure that the tool and arbor are correctly balanced. CBDP L8
KAPR APMX LF Right hand tool holder only.
DC Set Bolt Geometry
L 2.000" HSCUF37520
y SHELL TYPE (A Holders) &2.500" HSCUF50028 With Coolant Hole Dimensions (inch)
Order Number
R DC LF DCON CBDP DAH DCSFMS KWW L8 APMX Insert Screw Wrench Anti-seize Lubricant Insert Type
| APX4KUR0209A16A | 3 9 2.000 2.500 .750 1.063 .415 1.918 .313 .187 1.650 TPS43 | TIP15W | MK1KS | ||
| a | |||||
| AOMT1848 | |||||
| APX4KUR2516CA22A | a | 4 16 2.500 3.500 1.000 1.339 .539 2.409 .375 .219 2.200 TPS43 | TIP15W | MK1KS |
* Clamp Torque (lbf-in) : TPS43=35.4 Note 1) When using inserts with corner radius Re >.126" on the bottom, B-Holders or C-Holders are required as shown on page L117. Note 2) Only corner radius Re .016" and .031" can be used for the peripheral cutting edges expect the bottom cutting edge (the end cuttting edge). Note 3) When using the tool at high spindle speeds, ensure that the tool and arbor are correctly balanced.
Note 4) In case of internal coolant supply, please use a face mill arbor with through coolant channels; Regular center-thru or side-thru arbors can't be used. Note 5) The cutter body includes a non-coolant through set bolt for an arbor.