Общий каталог Mitsubishi 2020 - 2021 - страница 1292
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
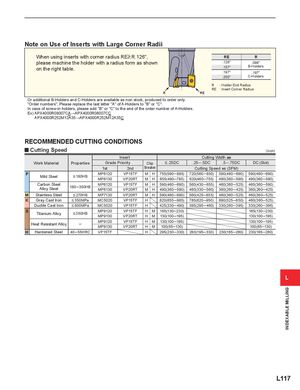
Note on Use of Inserts with Large Corner Radii
When using inserts with corner radius RE> R.126",
please machine the holder with a radius form as shown
on the right table.
R RE Or additional B-Holders and C-Holders are available as non stock, produced to order only. "Order numbers"; Please replace the last letter "A" of A-Holders to "B" or "C". In case of screw-in holders, please add "B" or "C" to the end of the order number of A-Holders. Ex) APX4000R08007CA→APX4000R08007CC APX4000R252M12A35→APX4000R252M12A35C
RECOMMENDED CUTTING CONDITIONS
| RE | R | |
| .126" | .098" | |
| .157" | B-Holders | |
| .197" | .197" | |
| .250" | C-Holders |
R : Holder End Radius RE : Insert Corner Radius
| y C | utting Speed | (inch) | |||||||
| Insert | Cutting | Width ae | |||||||
| Work Material | Properties | Grade | Priority | Chip | .25─.5DC | .5─.75DC | DC (Slot) | ||
| 1st | 2nd | Breaker | CuttingSpe | edvc (SFM) | |||||
| P | Mild Steel | MP6120 | VP15TF | M H | 755(590─885) | 720(560─850) | 590(460─690) | 590(460─690) | |
| MP6130 | VP20RT | M H | 655(490─785) | 620(460─755) | 490(360─590) | 490(360─590) | |||
| Carbon Steel | 180─350HB | MP6120 | VP15TF | M H | 590(460─690) | 560(430─655) | 460(360─525) | 460(360─590) | |
| Alloy Steel | MP6130 | VP20RT | M H | 490(360─590) | 460(330─560) | 360(260─425) | 360(260─425) | ||
| M | Stainless Steel | MP7130 | VP20RT | M H | 590(460─690) | 560(425─655) | 460(360─525) | 460(360─525) | |
| K | GrayCast Iron | MC5020 | VP15TF | H | 820(655─985) | 785(620─950) | 690(525─850) | 460(360─525) | |
| Ductile Cast Iron | MC5020 | VP15TF | H | 425(330─490) | 395(295─460) | 330(260─395) | 330(260─395) | ||
| S | Titi All | MP9120 | VP15TF | H M | 165(130─230) | 165(130─230) | |||
| anum oy | MP9130 | VP20RT | H M | 130(100─195) | 130(100─195) | ||||
| H | t Ritt All | ─ | MP9120 | VP15TF | H M | 130(100─195) | 130(100─195) | ||
| a essan oy | MP9130 | VP20RT | H M | 100(65─130) | 100(65─130) | ||||
| H | Hardened Steel | 40─55HRC | VP15TF | H | 295(230─330) | 280(195─330) | 230(165─260) | 230(165─260) |