Общий каталог Mitsubishi 2020 - 2021 - страница 993
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
CARBIDE
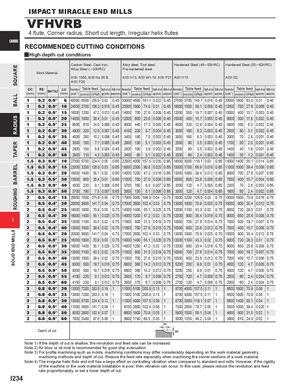
RECOMMENDED CUTTING CONDITIONS
y High depth cut conditions
| Work | Material | Carbo Alloy S AISI 1 AISI P | n Stee teel ( 050, A 20 | l, Cast Iron, ─30HRC) ISI No 35 B, | Alloy Pre-h AISI H | steel, T ardene 13, AI | ool st d stee SI W1 | eel, l -10, AI | SI P21 | Harde AISI H | ned S 13 | teel (45 | ─55H | RC) | Harde AISI D | ned S 2 | teel (5 | 5─62H | RC) | |||
| DC | RE | BHTA2 | LU | Revolution | Table | feed Depth of cut | Width of cut | Revolution | Table | feed | Depth of cut | Width of cut | Revolution | Tabl | e feed | Depth of cut | Width of cut | Revolution | Table | feed | Depth of cu | t Width of cut |
| (mm) | (mm) | (mm) | (min-1) ( | mm/min) | ap(mm) (IPM) | ae(mm) | (min-1) | (mm/min) | (IPM) | ap(mm) | ae(mm) | (min-1) ( | mm/min | ) (IPM) | ap(mm) | ae(mm) | (min-1) | (mm/min) | (IPM) | ap(mm) | ae(mm) | |
| 1 | 0.2 | 0.9° | 6 | 40000 | 6500 | 255.9 0.03 | 0.45 | 33000 | 4600 | 181.1 | 0.022 | 0.45 | 27000 | 3700 | 145.7 | 0.018 | 0.45 | 20000 | 1600 | 63.0 | 0.01 | 0.45 |
| 1 | 0.2 | 0.9° | 10 | 24000 | 2700 | 106.3 0.015 | 0.45 | 20000 | 1900 | 74.8 | 0.01 | 0.45 | 16000 | 1500 | 59.1 | 0.008 | 0.45 | 12000 | 700 | 27.6 | 0.006 | 0.45 |
| 1 | 0.2 | 0.9° | 15 | 16000 | 1200 | 47.2 0.013 | 0.45 | 14000 | 700 | 27.6 | 0.008 | 0.45 | 12000 | 500 | 19.7 | 0.007 | 0.45 | 10000 | 400 | 15.7 | 0.003 | 0.45 |
| 1 | 0.2 | 0.9° | 20 | 14000 | 1000 | 39.4 0.01 | 0.45 | 12000 | 600 | 23.6 | 0.006 | 0.45 | 10000 | 400 | 15.7 | 0.005 | 0.45 | 9000 | 300 | 11.8 | 0.002 | 0.45 |
| 1 | 0.2 | 0.9° | 25 | 9500 | 610 | 24.0 0.008 | 0.45 | 8000 | 440 | 17.3 | 0.005 | 0.45 | 6000 | 320 | 12.6 | 0.004 | 0.45 | 4800 | 160 | 6.3 | 0.002 | 0.45 |
| 1 | 0.2 | 0.9° | 30 | 4900 | 320 | 12.6 0.007 | 0.45 | 4100 | 220 | 8.7 | 0.004 | 0.45 | 3000 | 160 | 6.3 | 0.003 | 0.45 | 2500 | 80 | 3.1 | 0.002 | 0.45 |
| 1 | 0.2 | 0.9° | 35 | 4000 | 260 | 10.2 0.006 | 0.45 | 3400 | 190 | 7.5 | 0.003 | 0.45 | 3000 | 160 | 6.3 | 0.003 | 0.45 | 2000 | 70 | 2.8 | 0.001 | 0.45 |
| 1 | 0.2 | 0.9° | 40 | 3500 | 180 | 7.1 0.005 | 0.45 | 2900 | 130 | 5.1 | 0.003 | 0.45 | 2000 | 90 | 3.5 | 0.003 | 0.45 | 1700 | 50 | 2.0 | 0.001 | 0.45 |
| 1 | 0.2 | 0.9° | 45 | 2900 | 150 | 5.9 0.004 | 0.45 | 2400 | 100 | 3.9 | 0.002 | 0.45 | 2000 | 90 | 3.5 | 0.002 | 0.45 | 1400 | 40 | 1.6 | 0.001 | 0.45 |
| 1 | 0.2 | 0.9° | 50 | 2900 | 110 | 4.3 0.003 | 0.45 | 2400 | 80 | 3.1 | 0.002 | 0.45 | 2000 | 60 | 2.4 | 0.002 | 0.45 | 1400 | 30 | 1.2 | 0.001 | 0.45 |
| 1.5 | 0.3 | 0.9° | 10 | 27000 | 5700 | 224.4 0.05 | 0.65 | 22000 | 4000 | 157.5 | 0.035 | 0.65 | 18000 | 3000 | 118.1 | 0.03 | 0.65 | 14000 | 1400 | 55.1 | 0.014 | 0.65 |
| 1.5 | 0.3 | 0.9° | 15 | 22000 | 3200 | 126.0 0.03 | 0.65 | 18000 | 2300 | 90.6 | 0.025 | 0.65 | 15000 | 1700 | 66.9 | 0.018 | 0.65 | 11000 | 1000 | 39.4 | 0.009 | 0.65 |
| 1.5 | 0.3 | 0.9° | 20 | 16000 | 1400 | 55.1 0.02 | 0.65 | 14000 | 1200 | 47.2 | 0.016 | 0.65 | 13000 | 1000 | 39.4 | 0.012 | 0.65 | 9000 | 700 | 27.6 | 0.007 | 0.65 |
| 1.5 | 0.3 | 0.9° | 30 | 13000 | 900 | 35.4 0.01 | 0.65 | 11000 | 700 | 27.6 | 0.008 | 0.65 | 10000 | 600 | 23.6 | 0.006 | 0.65 | 7500 | 400 | 15.7 | 0.004 | 0.65 |
| 1.5 | 0.3 | 0.9° | 40 | 4500 | 230 | 9.1 0.008 | 0.65 | 3700 | 160 | 6.3 | 0.007 | 0.65 | 3000 | 120 | 4.7 | 0.005 | 0.65 | 2300 | 70 | 2.8 | 0.003 | 0.65 |
| 1.5 | 0.3 | 0.9° | 50 | 3700 | 190 | 7.5 0.007 | 0.65 | 3000 | 130 | 5.1 | 0.006 | 0.65 | 3000 | 120 | 4.7 | 0.004 | 0.65 | 1900 | 60 | 2.4 | 0.002 | 0.65 |
| 2 | 0.5 | 0.4° | 15 | 20000 | 7000 | 275.6 0.05 | 0.75 | 17000 | 5000 | 196.9 | 0.04 | 0.75 | 13000 | 3200 | 126.0 | 0.03 | 0.75 | 10000 | 1800 | 70.9 | 0.016 | 0.75 |
| 2 | 0.5 | 0.4° | 20 | 20000 | 3600 | 141.7 0.04 | 0.75 | 17000 | 2600 | 102.4 | 0.03 | 0.75 | 13000 | 1800 | 70.9 | 0.025 | 0.75 | 10000 | 900 | 35.4 | 0.012 | 0.75 |
| 2 | 0.5 | 0.4° | 25 | 16000 | 1800 | 70.9 0.03 | 0.75 | 14000 | 1400 | 55.1 | 0.025 | 0.75 | 12000 | 1100 | 43.3 | 0.02 | 0.75 | 9000 | 720 | 28.3 | 0.01 | 0.75 |
| 2 | 0.5 | 0.4° | 30 | 16000 | 1400 | 55.1 0.025 | 0.75 | 14000 | 1200 | 47.2 | 0.02 | 0.75 | 12000 | 900 | 35.4 | 0.016 | 0.75 | 9000 | 650 | 25.6 | 0.008 | 0.75 |
| 2 | 0.5 | 0.4° | 35 | 13000 | 1100 | 43.3 0.02 | 0.75 | 11000 | 800 | 31.5 | 0.018 | 0.75 | 10000 | 700 | 27.6 | 0.014 | 0.75 | 7000 | 500 | 19.7 | 0.007 | 0.75 |
| 2 | 0.5 | 0.4° | 40 | 13000 | 1000 | 39.4 0.02 | 0.75 | 11000 | 700 | 27.6 | 0.015 | 0.75 | 10000 | 600 | 23.6 | 0.012 | 0.75 | 7000 | 400 | 15.7 | 0.006 | 0.75 |
| 2 | 0.5 | 0.9° | 20 | 20000 | 3600 | 141.7 0.04 | 0.75 | 17000 | 2600 | 102.4 | 0.03 | 0.75 | 13000 | 1800 | 70.9 | 0.025 | 0.75 | 10000 | 900 | 35.4 | 0.012 | 0.75 |
| 2 | 0.5 | 0.9° | 25 | 16000 | 1800 | 70.9 0.03 | 0.75 | 14000 | 1400 | 55.1 | 0.025 | 0.75 | 12000 | 1100 | 43.3 | 0.02 | 0.75 | 9000 | 720 | 28.3 | 0.01 | 0.75 |
| 2 | 0.5 | 0.9° | 30 | 16000 | 1400 | 55.1 0.025 | 0.75 | 14000 | 1200 | 47.2 | 0.02 | 0.75 | 12000 | 900 | 35.4 | 0.016 | 0.75 | 9000 | 650 | 25.6 | 0.008 | 0.75 |
| 2 | 0.5 | 0.9° | 35 | 13000 | 1100 | 43.3 0.02 | 0.75 | 11000 | 800 | 31.5 | 0.018 | 0.75 | 10000 | 700 | 27.6 | 0.014 | 0.75 | 7000 | 500 | 19.7 | 0.007 | 0.75 |
| 2 | 0.5 | 0.9° | 40 | 13000 | 1000 | 39.4 0.02 | 0.75 | 11000 | 700 | 27.6 | 0.015 | 0.75 | 10000 | 600 | 23.6 | 0.012 | 0.75 | 7000 | 400 | 15.7 | 0.006 | 0.75 |
| 2 | 0.5 | 0.9° | 45 | 8000 | 500 | 19.7 0.016 | 0.75 | 6800 | 360 | 14.2 | 0.012 | 0.75 | 5200 | 250 | 9.8 | 0.01 | 0.75 | 4000 | 120 | 4.7 | 0.005 | 0.75 |
| 2 | 0.5 | 0.9° | 50 | 8000 | 500 | 19.7 0.016 | 0.75 | 6800 | 360 | 14.2 | 0.012 | 0.75 | 5200 | 250 | 9.8 | 0.01 | 0.75 | 4000 | 120 | 4.7 | 0.005 | 0.75 |
| 2 | 0.5 | 0.9° | 55 | 4100 | 230 | 9.1 0.012 | 0.75 | 3500 | 170 | 6.7 | 0.009 | 0.75 | 2700 | 120 | 4.7 | 0.008 | 0.75 | 2000 | 60 | 2.4 | 0.004 | 0.75 |
| 2 | 0.5 | 0.9° | 60 | 4100 | 230 | 9.1 0.012 | 0.75 | 3500 | 170 | 6.7 | 0.009 | 0.75 | 2700 | 120 | 4.7 | 0.008 | 0.75 | 2000 | 60 | 2.4 | 0.004 | 0.75 |
| 3 | 0.8 | 0.9° | 20 | 13000 | 7200 | 283.5 0.19 | 1 | 11000 | 5100 | 200.8 | 0.15 | 1 | 8700 | 4000 | 157.5 | 0.11 | 1 | 6500 | 1800 | 70.9 | 0.06 | 1 |
| 3 | 0.8 | 0.9° | 25 | 13000 | 7200 | 283.5 0.19 | 1 | 11000 | 5100 | 200.8 | 0.15 | 1 | 8700 | 4000 | 157.5 | 0.11 | 1 | 6500 | 1800 | 70.9 | 0.06 | 1 |
| 3 | 0.8 | 0.9° | 30 | 13000 | 5700 | 224.4 0.12 | 1 | 11000 | 4000 | 157.5 | 0.09 | 1 | 8700 | 3000 | 118.1 | 0.07 | 1 | 6500 | 1400 | 55.1 | 0.04 | 1 |
| 3 | 0.8 | 0.9° | 40 | 11000 | 3600 | 141.7 0.08 | 1 | 9100 | 2600 | 102.4 | 0.06 | 1 | 7400 | 2000 | 78.7 | 0.05 | 1 | 5500 | 1000 | 39.4 | 0.025 | 1 |
| 3 | 0.8 | 0.9° | 50 | 8000 | 2600 | 102.4 0.07 | 1 | 6600 | 1800 | 70.9 | 0.05 | 1 | 5800 | 1500 | 59.1 | 0.04 | 1 | 4600 | 800 | 31.5 | 0.02 | 1 |
| 3 | 0.8 | 0.9° | 60 | 7800 | 2480 | 97.6 0.06 | 1 | 6600 | 1740 | 68.5 | 0.05 | 1 | 5000 | 1250 | 49.2 | 0.04 | 1 | 3900 | 610 | 24.0 | 0.02 | 1 |
| Dept | h of cut | ae |
Note 1) If the depth of cut is shallow, the revolution and feed rate can be increased. Note 2) Air blow or oil mist is recommended for good chip evacuation. Note 3) For profile machining such as molds, machining conditions may differ considerably depending on the work material geometry, machining methods and depth of cut. Reduce the feed rate especially when machining the corner sections of a work material. of the machine or the work material installation is poor, then vibration can occur. In this case, please reduce the revolution and feed