Общий каталог Mitsubishi 2020 - 2021 - страница 990
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
CARBIDE
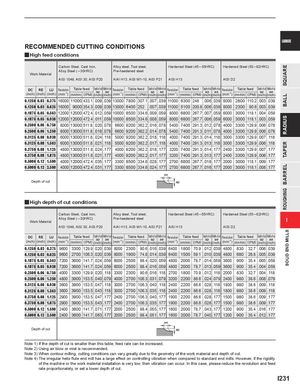
RECOMMENDED CUTTING CONDITIONS
y High feed conditions
| Work | Mat | erial | Carbon Alloy St AISI 10 | Steel, C eel (─3 49, AISI | ast Iro 0HRC) 30, AI | n, SI P20 | Alloy st Pre-hae AIAI H1 | eel, Too dened 3, AISI | l steel, steel W1-10 | , AISI P21 | Harden AISI H | ed Stee 13 | l (45─ | 55HRC) | Harde AISI D | ned Stee 2 | l (55─6 | 2HR | C) | |
| DC | RE | LU | Revolution | Table | feed | Depth of cut | Width of cut | Revolution | Table | feed | Depth of cut Width of cut | Revolution | Table | feed | Depth of cut Width of cut | Revolution | Table | feed | Depth of cu | t Width of cut |
| (inch) ( | inch) | (inch) | (min-1) | (mm/min) | (IPM) | ap (inch) | ae (inch) | (min-1) | (mm/min) | (IPM) | ap (inch) ae (inch) | (min-1) | (mm/min) | (IPM) | ap (inch) ae (inch) | (min-1) | (mm/min) | (IPM) | ap (inch) | ae (inch) |
| 0.1250 | 0.03 | 0.375 | 16000 | 11000 | 433.1 | .009 | .039 | 13000 | 7800 | 307.1 | .007 .039 | 11000 | 6300 | 248 | .006 .039 | 8000 | 2800 | 110.2 | .003 | .039 |
| 0.1250 | 0.03 | 0.625 | 16000 | 9000 | 354.3 | .009 | .039 | 13000 | 6400 | 252 | .007 .039 | 11000 | 5100 | 200.8 | .006 .039 | 8000 | 2300 | 90.6 | .003 | .039 |
| 0.1875 | 0.05 | 0.563 | 12000 | 12000 | 472.4 | .012 | .059 | 10000 | 8500 | 334.6 | .009 .059 | 8000 | 6800 | 267.7 | .007 .059 | 6000 | 3000 | 118.1 | .004 | .059 |
| 0.1875 | 0.05 | 0.938 | 12000 | 12000 | 472.4 | .011 | .059 | 10000 | 8500 | 334.6 | .008 .059 | 8000 | 6800 | 267.7 | .006 .059 | 6000 | 3000 | 118.1 | .003 | .059 |
| 0.2500 | 0.06 | 0.750 | 8000 | 13000 | 511.8 | .020 | .078 | 6600 | 9200 | 362.2 | .016 .078 | 5400 | 7400 | 291.3 | .012 .078 | 4000 | 3300 | 129.9 | .006 | .078 |
| 0.2500 | 0.06 | 1.250 | 8000 | 13000 | 511.8 | .018 | .078 | 6600 | 9200 | 362.2 | .014 .078 | 5400 | 7400 | 291.3 | .011 .078 | 4000 | 3300 | 129.9 | .006 | .078 |
| 0.3125 | 0.08 | 0.938 | 6000 | 13000 | 511.8 | .024 | .118 | 5000 | 9200 | 362.2 | .018 .118 | 4000 | 7400 | 291.3 | .014 .118 | 3000 | 3300 | 129.9 | .007 | .118 |
| 0.3125 | 0.08 | 1.563 | 6000 | 13000 | 511.8 | .021 | .118 | 5000 | 9200 | 362.2 | .017 .118 | 4000 | 7400 | 291.3 | .013 .118 | 3000 | 3300 | 129.9 | .006 | .118 |
| 0.3750 | 0.08 | 1.125 | 4800 | 13000 | 511.8 | .024 | .177 | 4000 | 9200 | 362.2 | .018 .177 | 3200 | 7400 | 291.3 | .014 .177 | 2400 | 3300 | 129.9 | .007 | .177 |
| 0.3750 | 0.08 | 1.875 | 4800 | 13000 | 511.8 | .021 | .177 | 4000 | 9200 | 362.2 | .017 .177 | 3200 | 7400 | 291.3 | .013 .177 | 2400 | 3300 | 129.9 | .006 | .177 |
| 0.5000 | 0.12 | 1.500 | 4000 | 12000 | 472.4 | .035 | .177 | 3300 | 8500 | 334.6 | .028 .177 | 2700 | 6800 | 267.7 | .018 .177 | 2000 | 3000 | 118.1 | .009 | .177 |
| 0.5000 | 0.12 | 2.500 | 4000 | 12000 | 472.4 | .031 | .177 | 3300 | 8500 | 334.6 | .024 .177 | 2700 | 6800 | 267.7 | .016 .177 | 2000 | 3000 | 118.1 | .008 | .177 |
| Dep | th of | cut | ae |
y High depth of cut conditions
| Wor | k Mat | erial | Carbon Alloy S AISI 10 | Steel, Cast Iro teel (─30HRC) 49, AISI 30, AI | n, SI P20 | Alloy st Pre-ha AIAI H | eel, Too edened 13, AISI | l steel, steel W1-10, | AISI P21 | Harden AISI H | ed Steel (45─ 13 | 55HRC) | Harden AISI D2 | ed Stee | l (55─ | 62HRC | ) | |
| DC (inch) | RE (inch) | LU (inch) | Revolution (min-1) | (mm/min) (IPM) Table feed | Depth of cut ap (inch) | Width of cut ae (inch) | Revolution (min-1) | (mm/min) Table | (IPM) feed | Depth of cut ap (inch) Width of cut ae (inch) | Revolution (min-1) | (mm/min) (IPM) Table feed | Depth of cut ap (inch) Width of cut ae (inch) | Revolution (min-1) | (mm/min) Table | (IPM) feed | Depth of cut ap (inch) ( | Width of cut ae inch) |
| 0.1250 | 0.03 | 0.375 | 9600 | 3300 129.9 | .020 | .039 | 8000 | 2300 | 90.6 | .016 .039 | 6400 | 1800 70.9 | .012 .039 | 4800 | 830 | 32.7 | .006 | .039 |
| 0.1250 | 0.03 | 0.625 | 9600 | 2700 106.3 | .020 | .039 | 8000 | 1900 | 74.8 | .014 .039 | 6400 | 1500 59.1 | .010 .039 | 4800 | 680 | 26.8 | .005 | .039 |
| 0.1875 | 0.05 | 0.563 | 7200 | 3600 141.7 | .024 | .059 | 6000 | 2500 | 98.4 | .020 .059 | 4800 | 2000 78.7 | .014 .059 | 3600 | 900 | 35.4 | .005 | .059 |
| 0.1875 | 0.05 | 0.938 | 7200 | 3600 141.7 | .024 | .059 | 6000 | 2500 | 98.4 | .016 .059 | 4800 | 2000 78.7 | .013 .059 | 3600 | 900 | 35.4 | .004 | .059 |
| 0.2500 | 0.06 | 0.750 | 4000 | 3300 129.9 | .020 | .118 | 3300 | 2300 | 90.6 | .016 .118 | 2700 | 1800 70.9 | .012 .118 | 2000 | 830 | 32.7 | .004 | .118 |
| 0.2500 | 0.06 | 1.250 | 4800 | 3900 153.5 | .040 | .079 | 4000 | 2700 | 106.3 | .031 .079 | 3200 | 2200 86.6 | .024 .079 | 2400 | 980 | 38.6 | .008 | .079 |
| 0.3125 | 0.08 | 0.938 | 3600 | 3900 153.5 | .047 | .118 | 3000 | 2700 | 106.3 | .040 .118 | 2400 | 2200 86.6 | .028 .118 | 1800 | 980 | 38.6 | .009 | .118 |
| 0.3125 | 0.08 | 1.563 | 3600 | 3900 153.5 | .043 | .118 | 3000 | 2700 | 106.3 | .035 .118 | 2400 | 2200 86.6 | .028 .118 | 1800 | 980 | 38.6 | .009 | .118 |
| 0.3750 | 0.08 | 1.125 | 2900 | 3900 153.5 | .047 | .177 | 2400 | 2700 | 106.3 | .040 .177 | 1900 | 2200 86.6 | .028 .177 | 1500 | 980 | 38.6 | .009 | .177 |
| 0.3750 | 0.08 | 1.875 | 2900 | 3900 153.5 | .043 | .177 | 2400 | 2700 | 106.3 | .035 .177 | 1900 | 2200 86.6 | .028 .177 | 1500 | 980 | 38.6 | .009 | .177 |
| 0.5000 | 0.12 | 1.500 | 2400 | 3600 141.7 | .071 | .177 | 2000 | 2500 | 98.4 | .055 .177 | 1600 | 2000 78.7 | .043 .177 | 1200 | 900 | 35.4 | .016 | .177 |
| 0.5000 | 0.12 | 2.500 | 2400 | 3600 141.7 | .063 | .177 | 2000 | 2500 | 98.4 | .051 .177 | 1600 | 2000 78.7 | .040 .177 | 1200 | 900 | 35.4 | .012 | .177 |
| Dep | th of | cut | ae |
Note 1) If the depth of cut is smaller than this table, feed rate can be increased. Note 2) Using air blow or mist is recommended. Note 3) When contour milling, cutting conditions can vary greatly due to the geometry of the work material and depth of cut.