Общий каталог Mitsubishi 2020 - 2021 - страница 986
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
CARBIDE
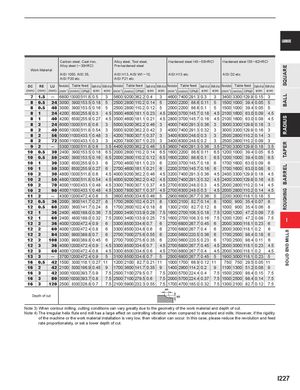
| Wo | rk Mate | rial | Carbon Alloy st AISI 10 AISI P2 | steel, Cast iron, eel(─30HRC) 50, AISI 35, 0 etc. | Alloy steel, Tool steel, Pre-hardened steel AISI H13, AISI W1─10, AISI P21 etc. | Hardened steel(45─55HR AISI H13 etc. | C) | Hardened st AISI D2 etc. | eel(55─62HR | C) | ||
| DC | RE | LU | Revolution | Depth of cut Table feed | Width of cut | Revolution Depth of cut Table feed | Width of cut | Revolution Depth of cut Table feed | Width of cut | Revolution Table | Depth of cut feed | Width of cut |
| (mm) | (mm) | (mm) | ( (min-1) | mm/min) (IPM) ap (mm) | ae (mm) | (mm/min) (IPM) (min-1) ap (mm) | ae (mm) | (mm/min) (IPM) (min-1) ap (mm) | ae (mm) | (mm/min) (min-1) | (IPM) ap (mm) | ae (mm) |
| 7 | 1.5 | ― | 68001 | 3000511.8 0.5 | 3 | 5600 9200362.2 0.4 | 3 | 4600 7400291.3 0.3 | 3 | 3400 3300 | 129.9 0.15 | 3 |
| 8 | 0.5 | 24 | 3000 | 3900153.5 0.18 | 5 | 2500 2800 110.2 0.14 | 5 | 2000 2200 86.6 0.11 | 5 | 1500 1000 | 39.4 0.05 | 5 |
| 8 | 0.5 | 40 | 3000 | 3900153.5 0.16 | 5 | 2500 2800 110.2 0.12 | 5 | 2000 2200 86.6 0.1 | 5 | 1500 1000 | 39.4 0.05 | 5 |
| 8 | 1 | 24 | 4200 | 6500255.9 0.3 | 4.5 | 3500 4600181.1 0.23 | 4.5 | 2800 3700145.7 0.18 | 4.5 | 2100 1600 | 63.0 0.09 | 4.5 |
| 8 | 1 | 40 | 4200 | 6500255.9 0.27 | 4.5 | 3500 4600181.1 0.21 | 4.5 | 2800 3700145.7 0.16 | 4.5 | 2100 1600 | 63.0 0.08 | 4.5 |
| 8 | 2 | 24 | 60001 | 3000511.8 0.6 | 3 | 5000 9200362.2 0.46 | 3 | 4000 7400291.3 0.36 | 3 | 3000 3300 | 129.9 0.18 | 3 |
| 8 | 2 | 40 | 60001 | 3000511.8 0.54 | 3 | 5000 9200362.2 0.42 | 3 | 4000 7400291.3 0.32 | 3 | 3000 3300 | 129.9 0.16 | 3 |
| 8 | 2 | 56 | 5000 1 | 1000433.1 0.48 | 3 | 4200 7800307.1 0.37 | 3 | 3400 6300248.0 0.3 | 3 | 2500 2800 | 110.2 0.14 | 3 |
| 8 | 2 | 72 | 5000 1 | 1000433.1 0.3 | 3 | 4200 7800307.1 0.23 | 3 | 3400 6300248.0 0.2 | 3 | 2500 2800 | 110.2 0.09 | 3 |
| 9 | 2 | ― | 53001 | 3000511.8 0.6 | 3.5 | 4400 9200362.2 0.46 | 3.5 | 3600 7400291.3 0.36 | 3.5 | 2700 3300 | 129.9 0.18 | 3.5 |
| 10 | 0.5 | 30 | 2400 | 3900153.5 0.18 | 6.5 | 2000 2800 110.2 0.14 | 6.5 | 1600 2200 86.6 0.11 | 6.5 | 1200 1000 | 39.4 0.05 | 6.5 |
| 10 | 0.5 | 50 | 2400 | 3900153.5 0.16 | 6.5 | 2000 2800 110.2 0.12 | 6.5 | 1600 2200 86.6 0.1 | 6.5 | 1200 1000 | 39.4 0.05 | 6.5 |
| 10 | 1 | 30 | 3300 | 6500255.9 0.3 | 6 | 2700 4600181.1 0.23 | 6 | 2200 3700145.7 0.18 | 6 | 1700 1600 | 63.0 0.09 | 6 |
| 10 | 1 | 50 | 3300 | 6500255.9 0.27 | 6 | 2700 4600181.1 0.21 | 6 | 2200 3700145.7 0.16 | 6 | 1700 1600 | 63.0 0.08 | 6 |
| 10 | 2 | 30 | 48001 | 3000511.8 0.6 | 4.5 | 4000 9200362.2 0.46 | 4.5 | 3200 7400291.3 0.36 | 4.5 | 2400 3300 | 129.9 0.18 | 4.5 |
| 10 | 2 | 50 | 48001 | 3000511.8 0.54 | 4.5 | 4000 9200362.2 0.42 | 4.5 | 3200 7400291.3 0.32 | 4.5 | 2400 3300 | 129.9 0.16 | 4.5 |
| 10 | 2 | 70 | 4000 1 | 1000433.1 0.48 | 4.5 | 3300 7800307.1 0.37 | 4.5 | 2700 6300248.0 0.3 | 4.5 | 2000 2800 | 110.2 0.14 | 4.5 |
| 10 | 2 | 90 | 4000 1 | 1000433.1 0.48 | 4.5 | 3300 7800307.1 0.37 | 4.5 | 2700 6300248.0 0.3 | 4.5 | 2000 2800 | 110.2 0.14 | 4.5 |
| 11 | 2 | ― | 43001 | 2000472.4 0.6 | 5 | 3600 8500334.6 0.46 | 5 | 2900 6800267.7 0.36 | 5 | 2200 3000 | 118.1 0.18 | 5 |
| 12 | 0.5 | 36 | 2000 | 3600141.7 0.27 | 8 | 1700 2600102.4 0.21 | 8 | 1300 2100 82.7 0.14 | 8 | 1000 900 | 35.4 0.07 | 8 |
| 12 | 0.5 | 60 | 2000 | 3600141.7 0.24 | 8 | 1700 2600102.4 0.18 | 8 | 1300 2100 82.7 0.12 | 8 | 1000 900 | 35.4 0.06 | 8 |
| 12 | 1 | 36 | 2400 | 4800189.0 0.36 | 7.5 | 2000 3400133.9 0.28 | 7.5 | 1600 2700106.3 0.18 | 7.5 | 1200 1200 | 47.2 0.09 | 7.5 |
| 12 | 1 | 60 | 2400 | 4800189.0 0.32 | 7.5 | 2000 3400133.9 0.25 | 7.5 | 1600 2700106.3 0.16 | 7.5 | 1200 1200 | 47.2 0.08 | 7.5 |
| 12 | 2 | 36 | 40001 | 2000472.4 0.9 | 6 | 3300 8500334.6 0.7 | 6 | 2700 6800267.7 0.45 | 6 | 2000 3000 | 118.1 0.23 | 6 |
| 12 | 2 | 60 | 40001 | 2000472.4 0.8 | 6 | 3300 8500334.6 0.6 | 6 | 2700 6800267.7 0.4 | 6 | 2000 3000 | 118.1 0.2 | 6 |
| 12 | 2 | 84 | 3300 | 9900389.8 0.7 | 6 | 2700 7000275.6 0.55 | 6 | 2200 5600220.5 0.36 | 6 | 1700 2500 | 98.4 0.18 | 6 |
| 12 | 2 | 108 | 3300 | 9900389.8 0.45 | 6 | 2700 7000275.6 0.35 | 6 | 2200 5600220.5 0.23 | 6 | 1700 2500 | 98.4 0.11 | 6 |
| 12 | 3 | 36 | 40001 | 2000472.4 0.9 | 4.5 | 3300 8500334.6 0.7 | 4.5 | 2700 6800267.7 0.45 | 4.5 | 2000 3000 | 118.1 0.23 | 4.5 |
| 12 | 3 | 60 | 40001 | 2000472.4 0.8 | 4.5 | 3300 8500334.6 0.6 | 4.5 | 2700 6800267.7 0.4 | 4.5 | 2000 3000 | 118.1 0.2 | 4.5 |
| 13 | 3 | ― | 37001 | 2000472.4 0.9 | 5 | 3100 8500334.6 0.7 | 5 | 2500 6800267.7 0.45 | 5 | 1900 3000 | 118.1 0.23 | 5 |
| 16 | 0.5 | 42 | 1500 | 3000118.1 0.27 | 11 | 1200 2100 82.7 0.21 | 11 | 1000 1700 66.9 0.12 | 11 | 750 750 | 29.5 0.05 | 11 |
| 16 | 2 | 42 | 2100 | 5000196.9 0.45 | 9 | 1700 3600141.7 0.35 | 9 | 1400 2900 114.2 0.2 | 9 | 1100 1300 | 51.2 0.08 | 9 |
| 16 | 3 | 42 | 30001 | 0000393.7 0.9 | 7.5 | 2500 7100279.5 0.7 | 7.5 | 2000 5700224.4 0.4 | 7.5 | 1500 2500 | 98.4 0.15 | 7.5 |
| 16 | 3 | 80 | 30001 | 0000393.7 0.8 | 7.5 | 2500 7100279.5 0.6 | 7.5 | 2000 5700224.4 0.37 | 7.5 | 1500 2500 | 98.4 0.14 | 7.5 |
| 16 | 3 | 120 | 2500 | 8300326.8 0.7 | 7.5 | 2100 5900232.3 0.55 | 7.5 | 1700 4700185.0 0.32 | 7.5 | 1300 2100 | 82.7 0.12 | 7.5 |
| De | pth of | cut | a | e |
Note 3) When contour milling, cutting conditions can vary greatly due to the geometry of the work material and depth of cut. Note 4) The irregular helix flute end mill has a large effect on controlling vibration when compared to standard end mills. However, if the rigidity of the machine or the work material installation is very low, then vibration can occur. In this case, please reduce the revolution and feed rate proportionately, or set a lower depth of cut.