Общий каталог Mitsubishi 2020 - 2021 - страница 978
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
CARBIDE
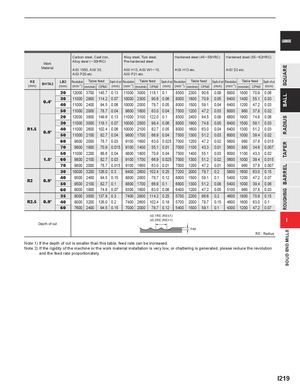
| Work Material | Carbon Alloy st AISI 10 AISI P2 | steel, C eel(─30 50, AISI 0 etc. | ast iron, HRC) 35, | Alloy st Pre-har AISI H1 AISI P2 | eel, Too dened s 3, AISI 1 etc. | l steel, teel W1─10, | Harden AISI H1 | ed steel 3 etc. | (45─55 | HRC) | Harden AISI D2 | ed steel etc. | (55─62 | HRC) | ||||
| RE | BHTA2 | LB2 | Revolution | Table | feed | Depth of cut | Revolution | Table | feed | Depth of cut | Revolution | Table | feed | Depth of cut | Revolution | Table | feed | Depth of cut |
| (mm) | (mm) | (min-1) | (mm/min) | (IPM) | (mm) | (min-1) | (mm/min) | (IPM) | (mm) | (min-1) | (mm/min) | (IPM) | (mm) | (min-1) | (mm/min) | (IPM) | (mm) | |
| 20 | 12000 | 3700 | 145.7 | 0.13 | 11000 | 3000 | 118.1 | 0.1 | 8500 | 2300 | 90.6 | 0.09 | 6800 | 1800 | 70.9 | 0.06 | ||
| ° | 30 | 11000 | 2900 | 114.2 | 0.07 | 10000 | 2300 | 90.6 | 0.06 | 8000 | 1800 | 70.9 | 0.05 | 6400 | 1400 | 55.1 | 0.03 | |
| 0.4 | 40 | 11000 | 2400 | 94.5 | 0.06 | 10000 | 2000 | 78.7 | 0.05 | 8000 | 1500 | 59.1 | 0.04 | 6400 | 1200 | 47.2 | 0.03 | |
| 50 | 11000 | 2000 | 78.7 | 0.04 | 9800 | 1600 | 63.0 | 0.04 | 7500 | 1200 | 47.2 | 0.03 | 6000 | 960 | 37.8 | 0.02 | ||
| 20 | 12000 | 3800 | 149.6 | 0.13 | 11000 | 3100 | 122.0 | 0.1 | 8500 | 2400 | 94.5 | 0.09 | 6800 | 1900 | 74.8 | 0.06 | ||
| 30 | 11000 | 3000 | 118.1 | 0.07 | 10000 | 2500 | 98.4 | 0.06 | 8000 | 1900 | 74.8 | 0.05 | 6400 | 1500 | 59.1 | 0.03 | ||
| R1.5 | ° | 40 | 11000 | 2600 | 102.4 | 0.06 | 10000 | 2100 | 82.7 | 0.05 | 8000 | 1600 | 63.0 | 0.04 | 6400 | 1300 | 51.2 | 0.03 |
| 0.9 | 50 | 11000 | 2100 | 82.7 | 0.04 | 9800 | 1700 | 66.9 | 0.04 | 7500 | 1300 | 51.2 | 0.03 | 6000 | 1000 | 39.4 | 0.02 | |
| 60 | 9800 | 2000 | 78.7 | 0.03 | 9100 | 1600 | 63.0 | 0.025 | 7000 | 1200 | 47.2 | 0.02 | 5600 | 960 | 37.8 | 0.015 | ||
| 70 | 9800 | 1800 | 70.9 | 0.015 | 9100 | 1400 | 55.1 | 0.01 | 7000 | 1100 | 43.3 | 0.01 | 5600 | 880 | 34.6 | 0.007 | ||
| 50 | 11000 | 2200 | 86.6 | 0.04 | 9800 | 1800 | 70.9 | 0.04 | 7500 | 1400 | 55.1 | 0.03 | 6000 | 1100 | 43.3 | 0.02 | ||
| 1.5° | 60 | 9800 | 2100 | 82.7 | 0.03 | 9100 | 1700 | 66.9 | 0.025 | 7000 | 1300 | 51.2 | 0.02 | 5600 | 1000 | 39.4 | 0.015 | |
| 70 | 9800 | 2000 | 78.7 | 0.015 | 9100 | 1600 | 63.0 | 0.01 | 7000 | 1200 | 47.2 | 0.01 | 5600 | 960 | 37.8 | 0.007 | ||
| 30 | 10000 | 3200 | 126.0 | 0.3 | 9400 | 2600 | 102.4 | 0.25 | 7200 | 2000 | 78.7 | 0.2 | 5800 | 1600 | 63.0 | 0.15 | ||
| ° | 40 | 9500 | 2400 | 94.5 | 0.15 | 8800 | 2000 | 78.7 | 0.12 | 6800 | 1500 | 59.1 | 0.1 | 5400 | 1200 | 47.2 | 0.07 | |
| R2 | 0.9 | 50 | 9500 | 2100 | 82.7 | 0.1 | 8800 | 1700 | 66.9 | 0.1 | 6800 | 1300 | 51.2 | 0.08 | 5400 | 1000 | 39.4 | 0.06 |
| 60 | 9000 | 1900 | 74.8 | 0.07 | 8300 | 1600 | 63.0 | 0.06 | 6400 | 1200 | 47.2 | 0.05 | 5100 | 960 | 37.8 | 0.03 | ||
| 35 | 8000 | 3500 | 137.8 | 0.3 | 7400 | 2900 | 114.2 | 0.25 | 5700 | 2200 | 86.6 | 0.2 | 4600 | 1800 | 70.9 | 0.15 | ||
| R2.5 | 0.9° | 40 | 8000 | 3200 | 126.0 | 0.2 | 7400 | 2600 | 102.4 | 0.18 | 5700 | 2000 | 78.7 | 0.15 | 4600 | 1600 | 63.0 | 0.1 |
| 60 | 7600 | 2400 | 94.5 | 0.15 | 7000 | 2000 | 78.7 | 0.12 | 5400 | 1500 | 59.1 | 0.1 | 4300 | 1200 | 47.2 | 0.07 | ||
| (RE (RE>1) | ||||||||||||||||||
| Depth of cut | ||||||||||||||||||
| RE : | Radius |
Note 1) If the depth of cut is smaller than this table, feed rate can be increased. Note 2) If the rigidity of the machine or the work material installation is very low, or chattering is generated, please reduce the revolution and the feed rate proportionately.