Общий каталог Mitsubishi 2020 - 2021 - страница 947
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
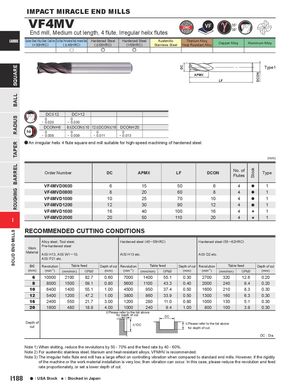
VF4MV
End mill, Medium cut length, 4 flute, Irregular helix flutes 38°
CARBIDE Carbon Steel, Alloy Steel, Cast Iron Tool Steel, Pre-Hardened Steel, Hardened Steel Hardened Steel Hardened Steel Austenitic Titanium Alloy,
| (<30HRC) | ( | 45HRC) | ( | 55HRC) | (>55HRC) | Stainless Steel | Heat Resistant Alloy | Copper Alloy | Aluminum Alloy | |
| u | e | e |
Type1 APMX LF
| DC | 12 | DC>12 |
| 0 | 0 | |
| - 0.020 | - 0.030 |
| DCON=6 | 8 | DCON | 10 12 | DCON | 16 DCON=20 | ||
| 0 | 0 | 0 | 0 | ||||
| - 0.008 | - 0.009 | - 0.011 | - 0.013 |
a An irregular helix 4 flute square end mill suitable for high-speed machining of hardened steel.
(mm)
| Order Number | DC | APMX | LF | DCON | No. of Flutes | Stock | Type |
| VF4MVD0600 | 6 | 15 | 50 | 6 | 4 | a | 1 |
| VF4MVD0800 | 8 | 20 | 60 | 8 | 4 | a | 1 |
| VF4MVD1000 | 10 | 25 | 70 | 10 | 4 | a | 1 |
| VF4MVD1200 | 12 | 30 | 90 | 12 | 4 | a | 1 |
| VF4MVD1600 | 16 | 40 | 100 | 16 | 4 | s | 1 |
| VF4MVD2000 | 20 | 50 | 110 | 20 | 4 | s | 1 |
RECOMMENDED CUTTING CONDITIONS
| Work Material | Alloy steel, T Pre-hardene AISI H13, AI AISI P21 etc | ool steel, d steel SI W1─10, . | Hardened ste AISI H13 etc. | el (45─55H | RC) | Hardened st AISI D2 etc. | eel (55─62H | RC) | ||||
| DC | Revolution | Table f | eed | Depth of cut | Revolution | Table | feed | Depth of cut | Revolution | Table | feed | Depth of cut |
| (mm) | (min-1) | (mm/min) | (IPM) | (mm) | (min-1) | (mm/min) | (IPM) | (mm) | (min-1) | (mm/min) | (IPM) | (mm) |
| 6 | 10000 | 2100 | 82.7 | 0.60 | 7000 | 1400 | 55.1 | 0.30 | 2700 | 320 | 12.6 | 0.20 |
| 8 | 8000 | 1500 | 59.1 | 0.80 | 5600 | 1100 | 43.3 | 0.40 | 2000 | 240 | 9.4 | 0.20 |
| 10 | 6400 | 1400 | 55.1 | 1.00 | 4500 | 950 | 37.4 | 0.50 | 1600 | 210 | 8.3 | 0.30 |
| 12 | 5400 | 1200 | 47.2 | 1.00 | 3800 | 860 | 33.9 | 0.50 | 1300 | 160 | 6.3 | 0.30 |
| 16 | 2400 | 550 | 21.7 | 3.00 | 1200 | 280 | 11.0 | 0.80 | 1000 | 130 | 5.1 | 0.30 |
| 20 | 1900 | 480 | 18.9 | 4.00 | 1000 | 240 | 9.4 | 1.00 | 800 | 100 | 3.9 | 0.30 |
| Depth of cut | fo | refer to the list r depth of cut. | above | DC | for de | refer to the lis pth of cut. | t above | DC : Dia. |
Note 1) When slotting, reduce the revolutions by 50 - 70% and the feed rate by 40 - 60%. Note 2) For austenitic stainless steel, titanium and heat-resistant alloys, VFMHV is recommended.