Общий каталог Mitsubishi 2020 - 2021 - страница 876
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
CARBIDE
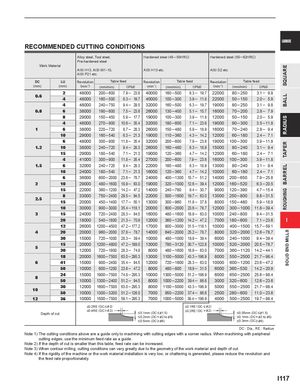
RECOMMENDED CUTTING CONDITIONS
| Work | Material | Alloy steel, Pre-harden AISI H13, A AISI P21 et | Tool steel, ed steel ISI W1-10, c. | Hardened AISI H13 e | steel(45─55HR tc. | C) | Hardened AISI D2 et | steel(55─62HR c. | C) | |
| DC | LU | Revolution | Table | feed | Revolution | Table | feed | Revolution | Table | feed |
| (mm) | (mm) | (min -1) | (mm/min) | (IPM) | (min -1) | (mm/min) | (IPM) | (min -1) | (mm/min) | (IPM) |
| 2 | 48000 | 200─600 | 7.9 ─ 23.6 | 40000 | 160─500 | 6.3 ─ 19.7 | 22000 | 80─250 | 3.1─ 9.8 | |
| 0.6 | 4 | 48000 | 160─500 | 6.3 ─ 19.7 | 40000 | 100─300 | 3.9 ─ 11.8 | 22000 | 50─150 | 2.0─ 5.9 |
| 4 | 48000 | 240─750 | 9.4 ─ 29.5 | 32000 | 160─500 | 6.3 ─ 19.7 | 19000 | 80─250 | 3.1─ 9.8 | |
| 0.8 | 6 | 38000 | 190─600 | 7.5 ─ 23.6 | 26000 | 130─400 | 5.1 ─ 15.7 | 16000 | 70─200 | 2.8─ 7.9 |
| 8 | 29000 | 150─450 | 5.9 ─ 17.7 | 19000 | 100─300 | 3.9 ─ 11.8 | 12000 | 50─150 | 2.0─ 5.9 | |
| 4 | 48000 | 270─900 | 10.6 ─ 35.4 | 32000 | 180─600 | 7.1 ─ 23.6 | 19000 | 90─300 | 3.5─ 11.8 | |
| 1 | 6 | 38000 | 220─720 | 8.7 ─ 28.3 | 26000 | 150─480 | 5.9 ─ 18.9 | 16000 | 70─240 | 2.8─ 9.4 |
| 10 | 29000 | 160─540 | 6.3 ─ 21.3 | 19000 | 110─360 | 4.3 ─ 14.2 | 12000 | 60─180 | 2.4─ 7.1 | |
| 6 | 48000 | 300─900 | 11.8 ─ 35.4 | 32000 | 200─600 | 7.9 ─ 23.6 | 19000 | 100─300 | 3.9─11.8 | |
| 1.2 | 10 | 38000 | 240─720 | 9.4 ─ 28.3 | 26000 | 160─480 | 6.3 ─ 18.9 | 15000 | 80─240 | 3.1─ 9.4 |
| 15 | 29000 | 180─540 | 7.1 ─ 21.3 | 19000 | 120─360 | 4.7 ─ 14.2 | 12000 | 60─180 | 2.4─ 7.1 | |
| 4 | 41000 | 300─900 | 11.8 ─ 35.4 | 27000 | 200─600 | 7.9 ─ 23.6 | 16000 | 100─300 | 3.9─11.8 | |
| 1.5 | 6 | 32000 | 240─720 | 9.4 ─ 28.3 | 22000 | 160─480 | 6.3 ─ 18.9 | 13000 | 80─240 | 3.1─ 9.4 |
| 10 | 24000 | 180─540 | 7.1 ─ 21.3 | 16000 | 120─360 | 4.7 ─ 14.2 | 10000 | 60─180 | 2.4─ 7.1 | |
| 6 | 36000 | 600─2000 | 23.6 ─ 78.7 | 24000 | 400─1300 | 15.7 ─ 51.2 | 14000 | 200─650 | 7.9─25.6 | |
| 2 | 10 | 29000 | 480─1600 | 18.9 ─ 63.0 | 19000 | 320─1000 | 12.6 ─ 39.4 | 12000 | 160─520 | 6.3─20.5 |
| 15 | 22000 | 360─1200 | 14.2 ─ 47.2 | 14000 | 240─780 | 9.4 ─ 30.7 | 9000 | 120─390 | 4.7─15.4 | |
| 8 | 33000 | 750─2400 | 29.5 ─ 94.5 | 22000 | 500─1600 | 19.7 ─ 63.0 | 13000 | 250─800 | 9.8─31.5 | |
| 2.5 | 15 | 20000 | 450─1400 | 17.7 ─ 55.1 | 13000 | 300─960 | 11.8 ─ 37.8 | 8000 | 150─480 | 5.9─18.9 |
| 10 | 30000 | 900─3000 | 35.4 ─ 118.1 | 20000 | 600─2000 | 23.6 ─ 78.7 | 12000 | 300─1000 | 11.8─39.4 | |
| 3 | 15 | 24000 | 720─2400 | 28.3 ─ 94.5 | 16000 | 480─1600 | 18.9 ─ 63.0 | 10000 | 240─800 | 9.4─31.5 |
| 20 | 18000 | 540─1800 | 21.3 ─ 70.9 | 12000 | 360─1200 | 14.2 ─ 47.2 | 7000 | 180─600 | 7.1─23.6 | |
| 12 | 26000 | 1200─4500 | 47.2 ─ 177.2 | 17000 | 800─3000 | 31.5 ─ 118.1 | 10000 | 400─1500 | 15.7─59.1 | |
| 4 | 20 | 20000 | 960─2000 | 37.8 ─ 78.7 | 14000 | 640─2000 | 25.2 ─ 78.7 | 8000 | 320─2000 | 12.6─78.7 |
| 30 | 15000 | 720─1000 | 28.3 ─ 39.4 | 10000 | 480─1000 | 18.9 ─ 39.4 | 6000 | 240─1000 | 9.4─39.4 | |
| 15 | 20000 | 1200─4800 | 47.2 ─ 189.0 | 13000 | 780─3120 | 30.7 ─ 122.8 | 10000 | 520─2000 | 20.5─78.7 | |
| 5 | 30 | 12000 | 720─1900 | 28.3 ─ 74.8 | 8000 | 480─1600 | 18.9 ─ 63.0 | 7000 | 360─1120 | 14.2─44.1 |
| 18 | 20000 | 1600─7500 | 63.0 ─ 295.3 | 13000 | 1100─5000 | 43.3 ─ 196.9 | 8000 | 550─2500 | 21.7─98.4 | |
| 6 | 41 | 15000 | 900─2400 | 35.4 ─ 94.5 | 12000 | 720─1600 | 28.3 ─ 63.0 | 10000 | 600─1200 | 23.6─47.2 |
| 50 | 10000 | 600─1200 | 23.6 ─ 47.2 | 8000 | 480─800 | 18.9 ─ 31.5 | 6000 | 360─530 | 14.2─20.9 | |
| 24 | 15000 | 1900─7500 | 74.8 ─ 295.3 | 10000 | 1300─5000 | 51.2 ─ 196.9 | 6000 | 650─2500 | 25.6─98.4 | |
| 8 | 50 | 10000 | 1300─2400 | 51.2 ─ 94.5 | 8000 | 1000─2200 | 39.4 ─ 86.6 | 3000 | 320─600 | 12.6─23.6 |
| 30 | 12000 | 1600─7500 | 63.0 ─ 295.3 | 8000 | 1100─5000 | 43.3 ─ 196.9 | 5000 | 550─2500 | 21.7─98.4 | |
| 10 | 50 | 10000 | 1300─3200 | 51.2 ─ 126.0 | 7000 | 950─2200 | 37.4 ─ 86.6 | 2500 | 280─600 | 11.0─23.6 |
| 12 | 36 | 10000 | 1500─7500 | 59.1 ─ 295.3 | 7000 | 1000─5000 | 39.4 ─ 196.9 | 4000 | 500─2500 | 19.7─98.4 |
| ≤0.2R | ( DC E | ( DC ≤0.1RE | 2) | |||||||
| Depth | of cut | ≤0.4R | ( >&2) E DC | 0 | .1mm (DC | &1.5) | ( >& ≤0.2RE DC | 2) | 0.05mm | (DC |
| 0 0 | = > .2mm (DC .5mm (DC | &2 to&5 &6) ) | 0.1mm ( 0.3mm ( | =&2 to&5) >&6) DC DC |
DC : Dia., RE : Radius Note 1) The cutting conditions above are a guide only to machining with cutting edges with a corner radius. When machining with peripheral cutting edges, use the minimum feed rate as a guide. Note 2) If the depth of cut is smaller than this table, feed rate can be increased. Note 3) When contour milling, cutting conditions can vary greatly due to the geometry of the work material and depth of cut.