Общий каталог Mitsubishi 2020 - 2021 - страница 872
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
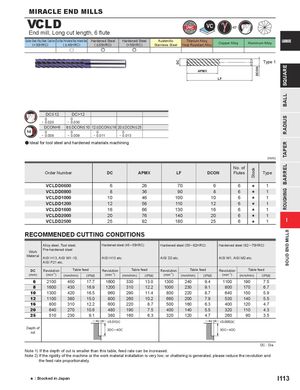
VCLD
End mill, Long cut length, 6 flute 45°
Carbon Steel, Alloy Steel, Cast Iron Tool Steel, Pre-Hardened Steel, Hardened Steel Hardened Steel Hardened Steel Austenitic Titanium Alloy, CARBIDE
| (<30HRC) | ( | 45HRC) | ( | 55HRC) | (>55HRC) | Stainless Steel | Heat Resistant Alloy | Copper Alloy | Aluminum Alloy | |
| u | e | e |
Type 1 APMX LF
| DC | 12 | DC>12 |
| 0 | 0 | |
| - 0.020 | - 0.030 |
| DCON=6 | 8 | DCON | 10 12 | DCON | 16 20 | DCON | 25 | ||
| 0 | 0 | 0 | 0 | ||||||
| - 0.008 | - 0.009 | - 0.011 | - 0.013 |
a Ideal for tool steel and hardened materials machining
(mm)
| Order Number | DC | APMX | LF | DCON | No. of Flutes | Stock | Type |
| VCLDD0600 | 6 | 26 | 70 | 6 | 6 | s | 1 |
| VCLDD0800 | 8 | 36 | 90 | 8 | 6 | s | 1 |
| VCLDD1000 | 10 | 46 | 100 | 10 | 6 | s | 1 |
| VCLDD1200 | 12 | 56 | 110 | 12 | 6 | s | 1 |
| VCLDD1600 | 16 | 66 | 130 | 16 | 6 | s | 1 |
| VCLDD2000 | 20 | 76 | 140 | 20 | 6 | s | 1 |
| VCLDD2500 | 25 | 92 | 180 | 25 | 6 | s | 1 |
RECOMMENDED CUTTING CONDITIONS
| Work Material | Alloy steel, Pre-hardene AISI H13, A AISI P21 et | Tool steel, d steel ISI W1-10, c. | Hardened ste AISI H13 etc. | el (45─55HR | C) | Hardened st AISI D2 etc. | eel (55─62H | RC) | Hardened st AISI W1, AI | eel (62─70H SI M2 etc. | RC) | |
| DC | Revolution | Table | feed | Revolution | Table | feed | Revolution | Table f | eed | Revolution | Table f | eed |
| (mm) | (min-1) | (mm/min) | (IPM) | (min-1) | (mm/min) | (IPM) | (min-1) | (mm/min) | (IPM) | (min-1) | (mm/min) | (IPM) |
| 6 | 2100 | 450 | 17.7 | 1600 | 330 | 13.0 | 1300 | 240 | 9.4 | 1100 | 190 | 7.5 |
| 8 | 1600 | 430 | 16.9 | 1200 | 310 | 12.2 | 1000 | 230 | 9.1 | 800 | 170 | 6.7 |
| 10 | 1300 | 420 | 16.5 | 960 | 290 | 11.4 | 800 | 220 | 8.7 | 640 | 150 | 5.9 |
| 12 | 1100 | 380 | 15.0 | 800 | 260 | 10.2 | 660 | 200 | 7.9 | 530 | 140 | 5.5 |
| 16 | 800 | 310 | 12.2 | 600 | 220 | 8.7 | 500 | 160 | 6.3 | 400 | 120 | 4.7 |
| 20 | 640 | 270 | 10.6 | 480 | 190 | 7.5 | 400 | 140 | 5.5 | 320 | 110 | 4.3 |
| 25 | 510 | 230 | 9.1 | 380 | 160 | 6.3 | 320 | 120 | 4.7 | 260 | 90 | 3.5 |
| Depth of cut | 3DC 4DC DC ≤ | 3DC 4DC DC ≤ |
DC : Dia. Note 1) If the depth of cut is smaller than this table, feed rate can be increased.