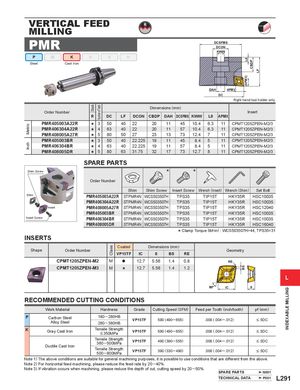
| VERTICAL MILLING | FEE | D | | | | | | | | | |
| PMR P M K Order Number Steel Cast Iron | N Stock er of Teeth | S | H | | Dimen | sions ( | mm) | | D DAH | CSFMS DCON KWW DC AP | MX (APMX) L8 CBDP LF Right hand tool holder only. Insert |
| R Numb | DC | LF | DCON | CBDP | DAH | DCSFMS | KWW | L8 | APMX | |
| PMR405003A22R ic | s 3 | 50 | 40 | 22 | 20 | 11 | 45 | 10.4 | 6.3 | 11 | CPMT1205ZPEN-M2/3 |
| PMR406304A22R etr | s 4 | 63 | 40 | 22 | 20 | 11 | 57 | 10.4 | 6.3 | 11 | CPMT1205ZPEN-M2/3 |
| PMR408005A27R M | s 5 | 80 | 50 | 27 | 23 | 13 | 73 | 12.4 | 7 | 11 | CPMT1205ZPEN-M2/3 |
| PMR405003BR h | s 3 | 50 | 40 | 22.225 | 19 | 11 | 45 | 8.4 | 5 | 11 | CPMT1205ZPEN-M2/3 |
| PMR406304BR nc | s 4 | 63 | 40 | 22.225 | 19 | 11 | 57 | 8.4 | 5 | 11 | CPMT1205ZPEN-M2/3 |
| PMR408005DR I | s 5 | 80 | 63 | 31.75 | 32 | 17 | 73 | 12.7 | 8 | 11 | CPMT1205ZPEN-M2/3 |
SPARE PARTS
| im Screw | Order N | umber | | | | | | |
| | | Shim | Shim Screw | Insert Screw | Wrench (Insert) | Wrench (Shim | ) Set Bolt |
| m | PMR4050 | 03A22R | STPMR4N | WCS503507H | TPS35 | TIP15T | HKY35R | HSC10035 |
| PMR4063 | 04A22R | STPMR4N | WCS503507H | TPS35 | TIP15T | HKY35R | HSC10035 |
| Insert | PMR4080 | 05A27R | STPMR4N | WCS503507H | TPS35 | TIP15T | HKY35R | HSC12040 |
| PMR4050 | 03BR | STPMR4N | WCS503507H | TPS35 | TIP15T | HKY35R | HSC10035 |
| ert Screw | PMR4063 | 04BR | STPMR4N | WCS503507H | TPS35 | TIP15T | HKY35R | HSC10035 |
| PMR4080 | 05DR | STPMR4N | WCS503507H | TPS35 | TIP15T | HKY35R | HSC16040 |
| SERTS | | | | | Clamp T | orque (lbf-in) : | WCS503507H | =44, TPS35=31 |
| | C ss | oated | Dimensions | (mm) | | | |
| Shape Order N | mber | la | | | | | Geometry | |
| | V C | P15TF IC | S | BS RE | | | |
| CPMT1205 | ZPEN-M2 | M | a 12.7 | 5.56 | 1.4 0.8 | | RE | |
| CPMT1205 | ZPEN-M3 | M | s 12.7 | 5.56 | 1.4 1.2 | | IC BS | S |
L
RECOMMENDED CUTTING CONDITIONS
| Work Material | Hardness | Grade | Cutting Speed (SFM) | Feed per Tooth (inch/tooth) | pf (mm) |
| P Carbon Steel Alloy Steel | 180─280HB 280─380HB | VP15TF | 590 (490─655) | .008 (.004─.012) | |
| K Gray Cast Iron | Tensile Strength | VP15TF | 590 (490─655) | .008 (.004─.012) | |
| Tensile Strength 360─500MPa | VP15TF | 490 (390─555) | .008 (.004─.012) | |
| Ductile Cast Iron | Tensile Strength 500─800MPa | VP15TF | 390 (330─490) | .008 (.004─.012) | |
Note 1) The above conditions are suitable for general machining purposes, it is possible to use conditions that are different from the above. Note 2) For horizontal feed machining, please reduce the feed rate by 20 ─ 40%. Note 3) If vibration occurs when machining, please reduce the depth of cut, cutting speed by 20─ 50%.
 Каталог Mitsubishi Materials запасные части
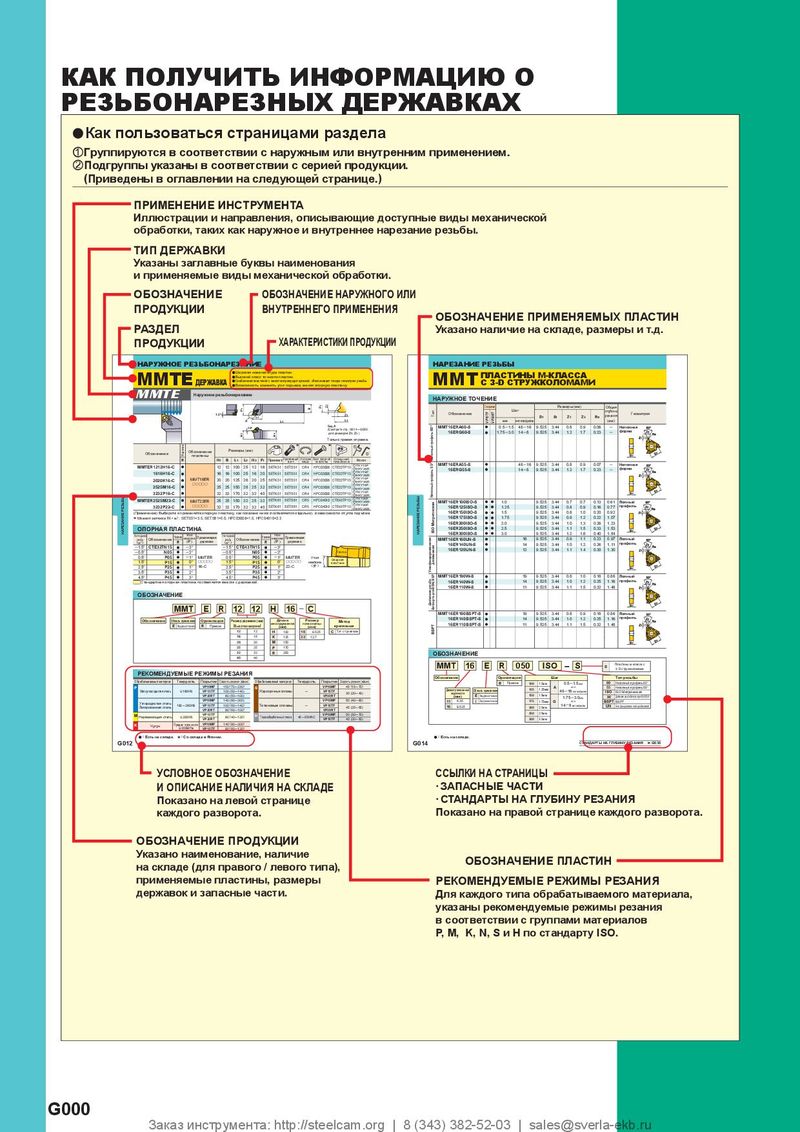 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
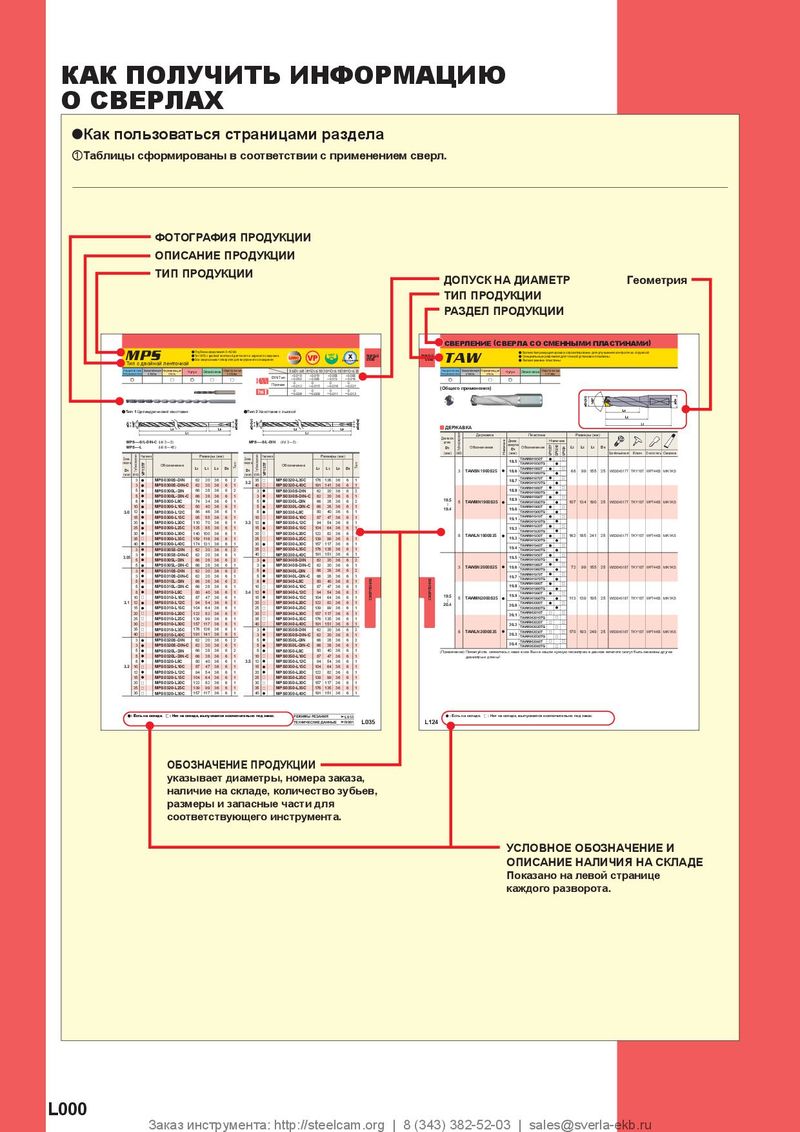 Каталог Mitsubishi Materials сверлильные инструменты
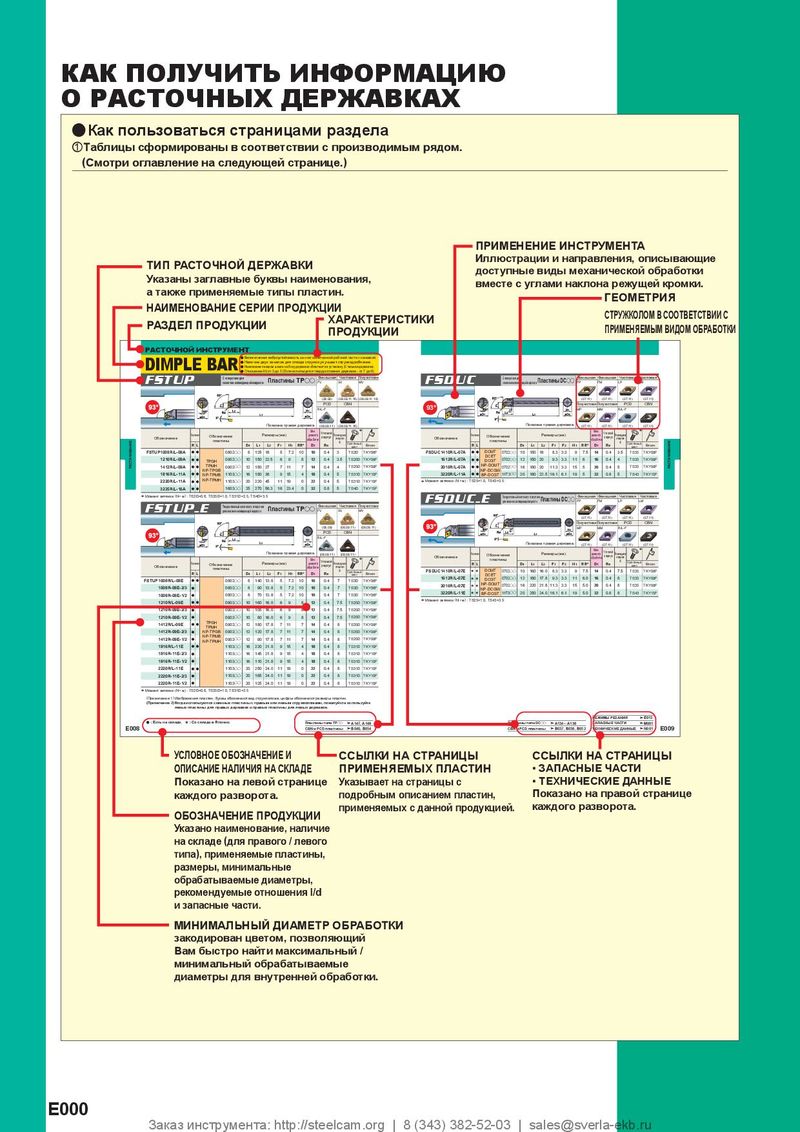 Каталог Mitsubishi Materials расточной инструмент
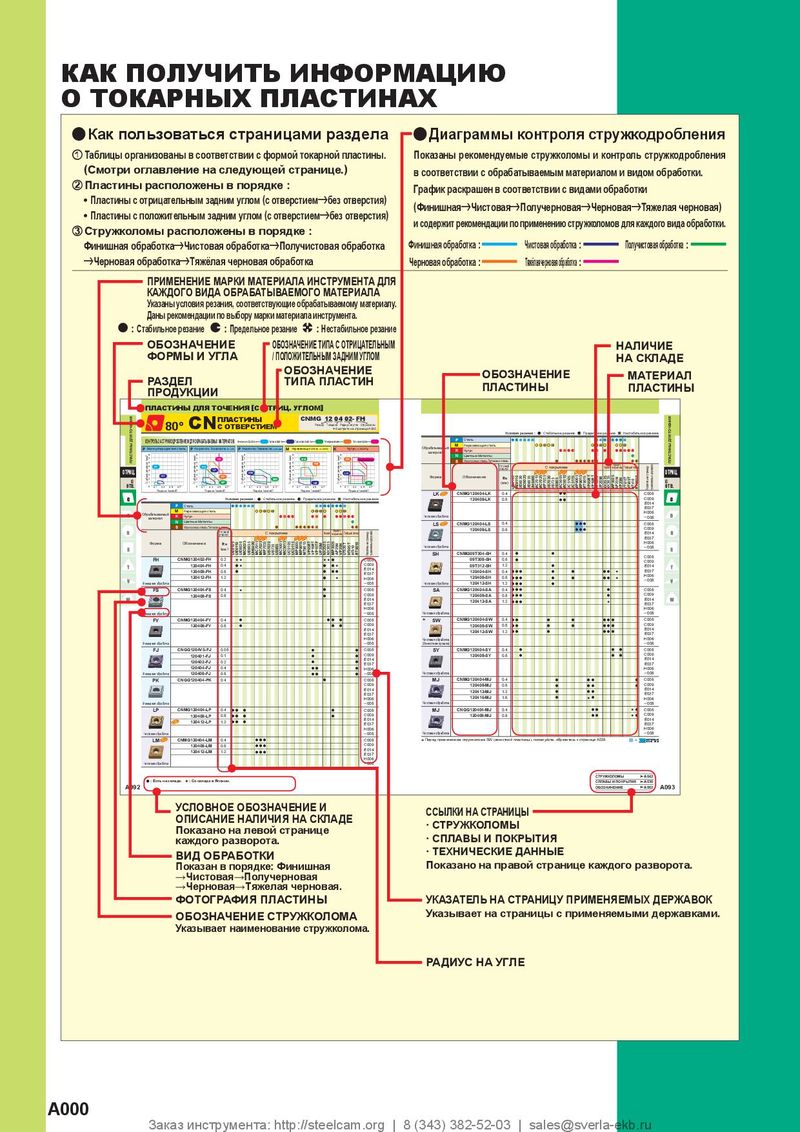 Каталог Mitsubishi Materials пластины для точения