Общий каталог Mitsubishi 2020 - 2021 - страница 1465
Навигация
 Каталог Mitsubishi Materials запасные части
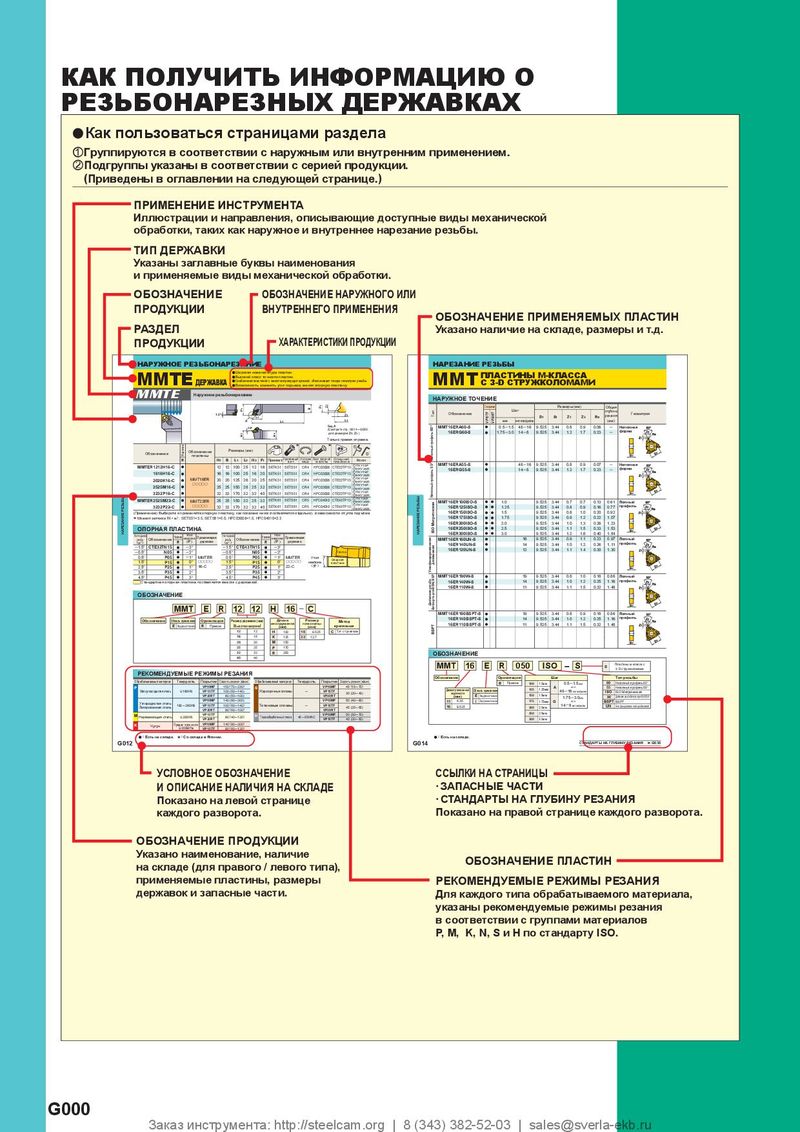 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
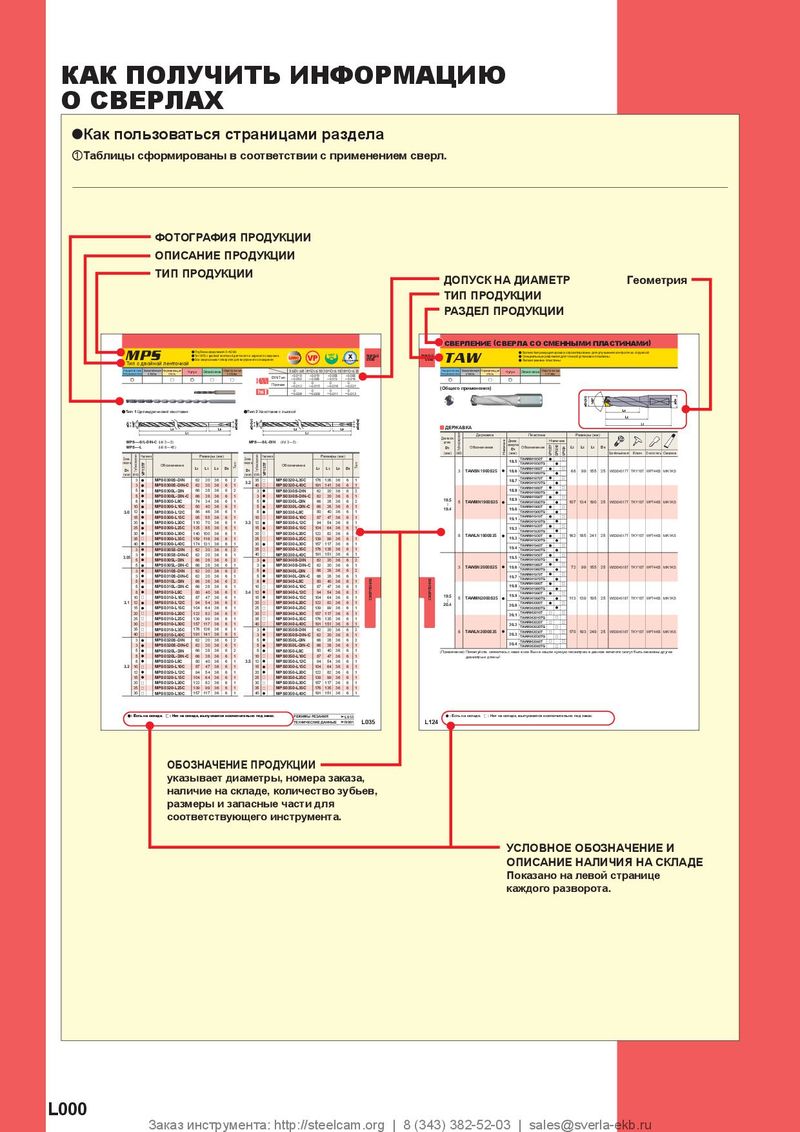 Каталог Mitsubishi Materials сверлильные инструменты
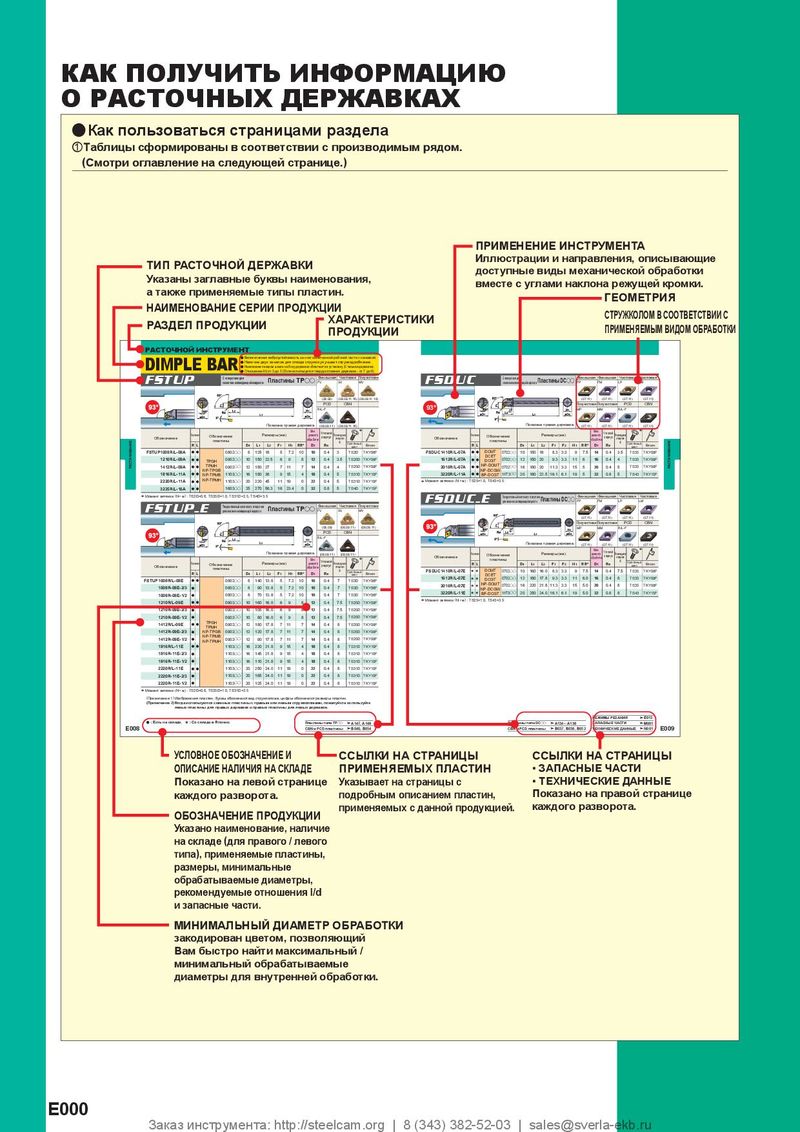 Каталог Mitsubishi Materials расточной инструмент
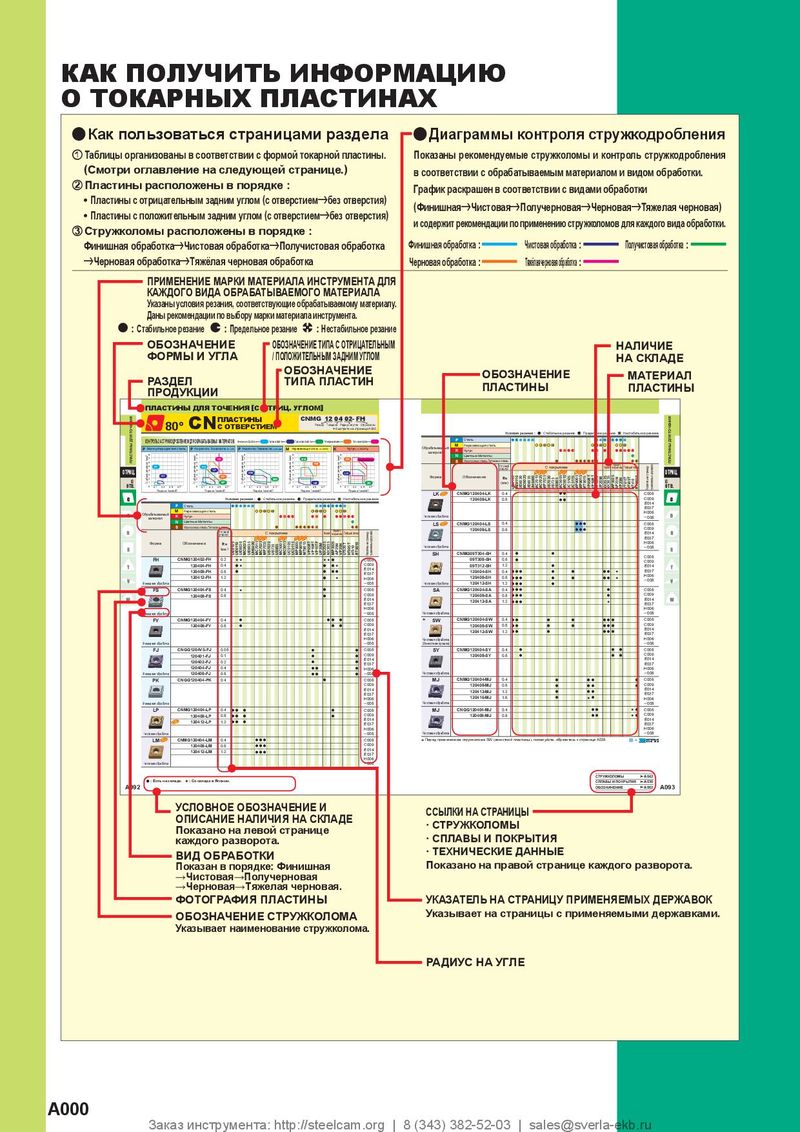 Каталог Mitsubishi Materials пластины для точения
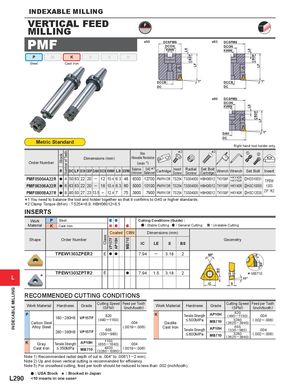
INDEXABLE MILLING
VERTICAL FEED
MILLING
PMF
ø50 DCSFMS ø63 DCSFMS
DCON DCON
KWW KWW
L8
L8
CBDP
P M K N S H
CBDP
Steel Cast Iron
LF
LF
DCCB DCCB
DC DC
ø80 DCSFMS
DCON
KWW
L8
CBDP
LF
DAH
DC
Metric Standard
Right hand tool holder only.
Max. * 2
* 2
Number of Teeth
z x
Stock
Dimensions (mm) Allowable Revolution
Order Number (min-1)
R Balance G40 *1 Cartridge Insert Radial Set Bolt Wrench Wrench Set Bolt Insert
DC LF DCON CBDP DAH DCCB KWW L8 DCSFMS Unknown Balanced Screw Screw (Cartridge)
PMF05004A22R a 4 50 63 22 20 ─ 12 10.4 6.3 48 6300 12700 PMFA13R TS254 TSS04005 HBH06012 TKY08F HKY40R
HKY50R zHDS10031 TPEW
PMF06306A22R a 6 63 63 22 20 ─ 18 10.4 6.3 60 5000 10100 PMFA13R TS254 TSS04005 HBH06012 TKY08F HKY40R xHSC10050 1303
7900 PMFA13R TS254 TSS04005 HBH06012 TKY08F HKY40R xHSC12035 ZP R2
p
PMF08008A27R a 8 80 50 27 23 13.5 ─ 12.4 7 75 3900
*12 You need to balance the tool and holder together so that it confirms to G40 or higher standards.
* Clamp Torque (lbf-in) : TS254=8.9, HBH06012=8.5
INSERTS
Work P Steel Cutting Conditions (Guide) :
Material K Cast Iron : Stable Cutting : General Cutting : Unstable Cutting
Coated CBN Dimensions (mm)
Class
Shape Order Number Geometry
VP15TF
AP10H
MB710
IC LE S BS
TPEW1303ZPER2 E a a 7.94 ─ 3.18 2 LE
BS
BS
TPEW1303ZPTR2
L *
E a 7.94 1.5 3.18 2
* MB710
IC S
INDEXABLE MILLING
RECOMMENDED CUTTING CONDITIONS
Cutting Speed Feed per Tooth Cutting Speed Feed per Tooth
Work Material Hardness Grade (SFM) (inch/tooth) Work Material Hardness Grade (SFM) (inch/tooth)
820
P 820 K Tensile Strength AP10H (490 ─ 1150) .004
180─280HB VP15TF (490 ─ 1150) (.002 ─ .006)
< 500MPa MB710 3280
Carbon Steel .004 Dactile (2625 ─ 3940)
Alloy Steel (.0019 ─ .006) Cast Iron AP10H 655
655 Tensile Strength (330 ─ 985) .004
280─380HB VP15TF (330 ─ 985) (.002 ─ .006)
< 800MPa MB710 3280
(2625 ─ 3940)
1150
K Gray Tensile Strength AP10H (655 ─ 1640) .004
Cast Iron < 350MPa MB710 4920 (.0019 ─ .006)
(3280 ─ 6560)
Note 1) Recommended radial depth of cut is .004" to .008"(1 ─ 2 mm).
Note 2) Up and down vertical cutting is recommended for efficiency.
Note 3) For crossfeed cutting, feed per tooth should be reduced to less than .002 (inch/tooth).
a : USA Stock s : Stocked in Japan
L290 <10 inserts in one case>
VERTICAL FEED
MILLING
PMF
ø50 DCSFMS ø63 DCSFMS
DCON DCON
KWW KWW
L8
L8
CBDP
P M K N S H
CBDP
Steel Cast Iron
LF
LF
DCCB DCCB
DC DC
ø80 DCSFMS
DCON
KWW
L8
CBDP
LF
DAH
DC
Metric Standard
Right hand tool holder only.
Max. * 2
* 2
Number of Teeth
z x
Stock
Dimensions (mm) Allowable Revolution
Order Number (min-1)
R Balance G40 *1 Cartridge Insert Radial Set Bolt Wrench Wrench Set Bolt Insert
DC LF DCON CBDP DAH DCCB KWW L8 DCSFMS Unknown Balanced Screw Screw (Cartridge)
PMF05004A22R a 4 50 63 22 20 ─ 12 10.4 6.3 48 6300 12700 PMFA13R TS254 TSS04005 HBH06012 TKY08F HKY40R
HKY50R zHDS10031 TPEW
PMF06306A22R a 6 63 63 22 20 ─ 18 10.4 6.3 60 5000 10100 PMFA13R TS254 TSS04005 HBH06012 TKY08F HKY40R xHSC10050 1303
7900 PMFA13R TS254 TSS04005 HBH06012 TKY08F HKY40R xHSC12035 ZP R2
p
PMF08008A27R a 8 80 50 27 23 13.5 ─ 12.4 7 75 3900
*12 You need to balance the tool and holder together so that it confirms to G40 or higher standards.
* Clamp Torque (lbf-in) : TS254=8.9, HBH06012=8.5
INSERTS
Work P Steel Cutting Conditions (Guide) :
Material K Cast Iron : Stable Cutting : General Cutting : Unstable Cutting
Coated CBN Dimensions (mm)
Class
Shape Order Number Geometry
VP15TF
AP10H
MB710
IC LE S BS
TPEW1303ZPER2 E a a 7.94 ─ 3.18 2 LE
BS
BS
TPEW1303ZPTR2
L *
E a 7.94 1.5 3.18 2
* MB710
IC S
INDEXABLE MILLING
RECOMMENDED CUTTING CONDITIONS
Cutting Speed Feed per Tooth Cutting Speed Feed per Tooth
Work Material Hardness Grade (SFM) (inch/tooth) Work Material Hardness Grade (SFM) (inch/tooth)
820
P 820 K Tensile Strength AP10H (490 ─ 1150) .004
180─280HB VP15TF (490 ─ 1150) (.002 ─ .006)
< 500MPa MB710 3280
Carbon Steel .004 Dactile (2625 ─ 3940)
Alloy Steel (.0019 ─ .006) Cast Iron AP10H 655
655 Tensile Strength (330 ─ 985) .004
280─380HB VP15TF (330 ─ 985) (.002 ─ .006)
< 800MPa MB710 3280
(2625 ─ 3940)
1150
K Gray Tensile Strength AP10H (655 ─ 1640) .004
Cast Iron < 350MPa MB710 4920 (.0019 ─ .006)
(3280 ─ 6560)
Note 1) Recommended radial depth of cut is .004" to .008"(1 ─ 2 mm).
Note 2) Up and down vertical cutting is recommended for efficiency.
Note 3) For crossfeed cutting, feed per tooth should be reduced to less than .002 (inch/tooth).
a : USA Stock s : Stocked in Japan
L290 <10 inserts in one case>