Общий каталог Mitsubishi 2020 - 2021 - страница 1447
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
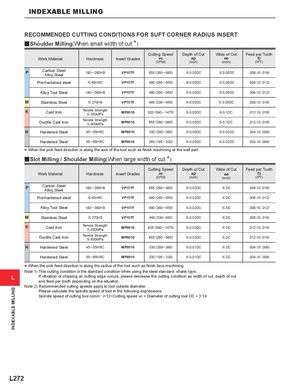
RECOMMENDED CUTTING CONDITIONS FOR SUFT CORNER RADIUS INSERT
Shoulder Milling(When small width of cut.*)
y
| Work Material | Hardness | Insert Grades | Cutting Speed vc (SFM) | Depth of Cut ap (inch) | Wide of Cut ae (inch) | Feed per Tooth fz (IPT) |
| P Carbon Steel AlloySteel | 180─280HB | VP15TF | 655(260─985) | .008( | ||
| Pre-hardened steel | VP15TF | 490(260─655) | .006( | |||
| Alloy Tool Steel | 180─380HB | VP15TF | 490(260─655) | .006( | ||
| M Stainless Steel | VP15TF | 490(330─655) | .008( | |||
| K Cast Iron | Tensile Strength | MP8010 | 820(590─1475) | .012( | ||
| Ductile Cast Iron | Tensile Strength | MP8010 | 655(260─985) | .012( | ||
| H Hardened Steel | 45─55HRC | MP8010 | 330 (260─395) | .004 ( | ||
| Hardened Steel | 55─65HRC | MP8010 | 260 (195─330) | .004 ( |
- When the pick feed direction is along the axis of the tool such as finish machining at the wall part. Slot Milling / Shoulder Milling(When large width of cut.*)
y
| Work Material | Hardness | Insert Grades | Cutting Speed vc (SFM) | Depth of Cut ap (inch) | Wide of Cut ae (inch) | Feed per Tooth fz (IPT) |
| P Carbon Steel AlloySteel | 180─280HB | VP15TF | 655 (260─985) | .008 ( | ||
| Pre-hardened steel | VP15TF | 490 (260─655) | .006 ( | |||
| Alloy Tool Steel | 180─380HB | VP15TF | 490 (260─655) | .006 ( | ||
| M Stainless Steel | VP15TF | 490 (330─655) | .008 ( | |||
| K Cast Iron | Tensile Strength | MP8010 | 835 (590─1475) | .012 ( | ||
| Ductile Cast Iron | Tensile Strength | MP8010 | 655 (260─985) | .012 ( | ||
| H Hardened Steel | 45─55HRC | MP8010 | 330 (260─395) | .004 ( | ||
| Hardened Steel | 55─65HRC | MP8010 | 230 (195─330) | .004 ( |
- When the pick feed direction is along the radius of the tool such as finish face machining.
Note 1) This cutting condition is the standard condition when using the steel standard shank type.
L If vibration or chipping on cutting edge occurs, please decrease the cutting condition as width of cut, depth of cut
and feed per tooth depending on the situation. Note 2) Recommended cutting speeds apply to tool outside diameter. Please calculate the spindle speed of tool in the following expressions.