Общий каталог Mitsubishi 2020 - 2021 - страница 1446
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
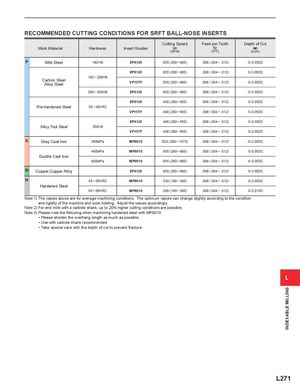
RECOMMENDED CUTTING CONDITIONS FOR SRFT BALL-NOSE INSERTS
| Work Material | Hardness | Insert Grades | Cutting Speed vc (SFM) | Feed per Tooth fz (IPT) | Depth of Cut ap (inch) |
| P Mild Steel | 180HB | EP6120 | 655 (260─985) | .008(.004─.012) | |
| 180─280HB | EP6120 | 655 (260─985) | .008(.004─.012) | ||
| Carbon Steel Alloy Steel | VP15TF | 655 (260─985) | .008(.004─.012) | ||
| 280─350HB | EP6120 | 655 (260─985) | .008(.004─.012) | ||
| Phdd Stl | 35─45HRC | EP6120 | 490 (260─655) | .008(.004─.012) | |
| re-arene ee | VP15TF | 490 (260─655) | .008(.004─.012) | ||
| All Tl Stl | 350HB | EP6120 | 490 (260─655) | .008(.004─.012) | |
| oy oo ee | VP15TF | 490 (260─655) | .008 (.004─.012) | ||
| K Gray Cast Iron | 350MPa | MP8010 | 820 (260─1475) | .008 (.004─.012) | |
| Dctile Cast Iron | 450MPa | MP8010 | 655 (260─985) | .008 (.004─.012) | |
| u | 800MPa | MP8010 | 655 (260─985) | .008 (.004─.012) | |
| N Copper,Copper Alloy | EP6120 | 655 (260─985) | .008 (.004─.012) | ||
| H | 45─55HRC | MP8010 | 330 (195─395) | .008 (.004─.012) | |
| Hardened Steel | 55─65HRC | MP8010 | 260 (195─395) | .008 (.004─.012) |
Note 1) The values above are for average machining conditions. The optimum values can change slightly according to the condition and rigidity of the machine and work holding. Adjust the values accordingly. Note 2) For end mills with a carbide shank, up to 20% higher cutting conditions are possible. Note 3) Please note the following when machining hardened steel with MP8010.
- Please shorten the overhang length as much as possible.
- Use with carbide shank recommended.
- Take special care with the depth of cut to prevent fracture.