Общий каталог Mitsubishi 2020 - 2021 - страница 1426
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
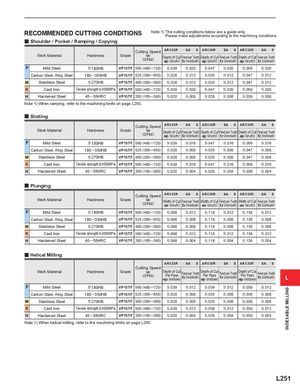
RECOMMENDED CUTTING CONDITIONS Note 1) The cutting conditions below are a guide only.
Please make adjustments according to the machining conditions.
y Shoulder / Pocket / Ramping / Copying
Cutting Speed ARX25RpppSAppS ARX30RpppSAppS ARX35RpppSAppS
Work Material Hardness Grade vc Depth of Cut Feed per Tooth Depth of Cut Feed per Tooth Depth of Cut Feed per Tooth
(SFM) ap (inch) fz (inch/tooth) ap (inch) fz (inch/tooth) ap (inch) fz (inch/tooth)
P Mild Steel < 180HB VP15TF 590 (490 ─ 720) <.039 <.020 <.047 <.020 <.059 <.020
Carbon Steel, Alloy Steel 180─ 350HB VP15TF 525 (395 ─ 655) <.028 <.012 <.035 <.012 <.047 <.012
M Stainless Steel < 270HB VP15TF 490 (395 ─ 590) <.028 <.012 <.035 <.012 <.047 <.012
K Cast Iron Tensile strength<450MPa VP15TF 590 (490 ─ 720) <.039 <.020 <.047 <.020 <.059 <.020
H Hardened Steel 45─ 55HRC VP15TF 260 (165 ─ 395) <.020 <.008 <.028 <.008 <.039 <.008
Note 1) When ramping, refer to the machining limits on page L250.
y Slotting
Cutting Speed ARX25RpppSAppS ARX30RpppSAppS ARX35RpppSAppS
Work Material Hardness Grade vc Depth of Cut Feed per Tooth Depth of Cut Feed per Tooth Depth of Cut Feed per Tooth
(SFM) ap (inch) fz (inch/tooth) ap (inch) fz (inch/tooth) ap (inch) fz (inch/tooth)
P Mild Steel < 180HB VP15TF 590 (490 ─ 720) <.039 <.016 <.047 <.016 <.059 <.016
Carbon Steel, Alloy Steel 180─ 350HB VP15TF 525 (395 ─ 655) <.028 <.008 <.035 <.008 <.047 <.008
M Stainless Steel < 270HB VP15TF 490 (395 ─ 590) <.028 <.008 <.035 <.008 <.047 <.008
K Cast Iron Tensile strength<450MPa VP15TF 590 (490 ─ 720) <.039 <.016 <.047 <.016 <.059 <.016
H Hardened Steel 45─ 55HRC VP15TF 260 (165 ─ 395) <.020 <.004 <.028 <.004 <.039 <.004
y Plunging
Cutting Speed ARX25RpppSAppS ARX30RpppSAppS ARX35RpppSAppS
Work Material Hardness Grade vc Width of Cut Feed per Tooth Width of Cut Feed per Tooth Width of Cut Feed per Tooth
(SFM) ae (inch) fz (inch/tooth) ae (inch) fz (inch/tooth) ae (inch) fz (inch/tooth)
P Mild Steel < 180HB VP15TF 590 (490 ─ 720) <.098 <.012 <.118 <.012 <.138 <.012
Carbon Steel, Alloy Steel 180─ 350HB VP15TF 525 (395 ─ 655) <.098 <.008 <.118 <.008 <.138 <.008
M Stainless Steel < 270HB VP15TF 490 (395 ─ 590) <.098 <.008 <.118 <.008 <.138 <.008
K Cast Iron Tensile strength<450MPa VP15TF 590 (490 ─ 720) <.098 <.012 <.118 <.012 <.138 <.012
H Hardened Steel 45─ 55HRC VP15TF 260 (165 ─ 395) <.098 <.004 <.118 <.004 <.138 <.004
y Helical Milling
ARX25RpppSAppS ARX30RpppSAppS ARX35RpppSAppS
Cutting Speed
Work Material Hardness Grade vc Depth of Cut Feed per Tooth Depth of Cut Feed per Tooth Depth of Cut Feed per Tooth
(SFM) Per Pass ) Per Pass ) Per Pass
( ( (
ap (inch/pass) fz inch/tooth ap (inch/pass) fz inch/tooth ap (inch/pass) fz inch/tooth
) L
P Mild Steel < 180HB VP15TF 590 (490 ─ 720) <.039 <.012 <.039 <.012 <.039 <.012 INDEXABLE MILLING
Carbon Steel, Alloy Steel 180─ 350HB VP15TF 525 (395 ─ 655) <.028 <.008 <.035 <.008 <.039 <.008
M Stainless Steel < 270HB VP15TF 490 (395 ─ 590) <.028 <.008 <.035 <.008 <.039 <.008
K Cast Iron Tensile strength<450MPa VP15TF 590 (490 ─ 720) <.039 <.012 <.039 <.012 <.039 <.012
H Hardened Steel 45─ 55HRC VP15TF 260 (165 ─ 395) <.020 <.004 <.028 <.004 <.039 <.004
Note 1) When helical milling, refer to the machining limits on page L250.
L251
Please make adjustments according to the machining conditions.
y Shoulder / Pocket / Ramping / Copying
Cutting Speed ARX25RpppSAppS ARX30RpppSAppS ARX35RpppSAppS
Work Material Hardness Grade vc Depth of Cut Feed per Tooth Depth of Cut Feed per Tooth Depth of Cut Feed per Tooth
(SFM) ap (inch) fz (inch/tooth) ap (inch) fz (inch/tooth) ap (inch) fz (inch/tooth)
P Mild Steel < 180HB VP15TF 590 (490 ─ 720) <.039 <.020 <.047 <.020 <.059 <.020
Carbon Steel, Alloy Steel 180─ 350HB VP15TF 525 (395 ─ 655) <.028 <.012 <.035 <.012 <.047 <.012
M Stainless Steel < 270HB VP15TF 490 (395 ─ 590) <.028 <.012 <.035 <.012 <.047 <.012
K Cast Iron Tensile strength<450MPa VP15TF 590 (490 ─ 720) <.039 <.020 <.047 <.020 <.059 <.020
H Hardened Steel 45─ 55HRC VP15TF 260 (165 ─ 395) <.020 <.008 <.028 <.008 <.039 <.008
Note 1) When ramping, refer to the machining limits on page L250.
y Slotting
Cutting Speed ARX25RpppSAppS ARX30RpppSAppS ARX35RpppSAppS
Work Material Hardness Grade vc Depth of Cut Feed per Tooth Depth of Cut Feed per Tooth Depth of Cut Feed per Tooth
(SFM) ap (inch) fz (inch/tooth) ap (inch) fz (inch/tooth) ap (inch) fz (inch/tooth)
P Mild Steel < 180HB VP15TF 590 (490 ─ 720) <.039 <.016 <.047 <.016 <.059 <.016
Carbon Steel, Alloy Steel 180─ 350HB VP15TF 525 (395 ─ 655) <.028 <.008 <.035 <.008 <.047 <.008
M Stainless Steel < 270HB VP15TF 490 (395 ─ 590) <.028 <.008 <.035 <.008 <.047 <.008
K Cast Iron Tensile strength<450MPa VP15TF 590 (490 ─ 720) <.039 <.016 <.047 <.016 <.059 <.016
H Hardened Steel 45─ 55HRC VP15TF 260 (165 ─ 395) <.020 <.004 <.028 <.004 <.039 <.004
y Plunging
Cutting Speed ARX25RpppSAppS ARX30RpppSAppS ARX35RpppSAppS
Work Material Hardness Grade vc Width of Cut Feed per Tooth Width of Cut Feed per Tooth Width of Cut Feed per Tooth
(SFM) ae (inch) fz (inch/tooth) ae (inch) fz (inch/tooth) ae (inch) fz (inch/tooth)
P Mild Steel < 180HB VP15TF 590 (490 ─ 720) <.098 <.012 <.118 <.012 <.138 <.012
Carbon Steel, Alloy Steel 180─ 350HB VP15TF 525 (395 ─ 655) <.098 <.008 <.118 <.008 <.138 <.008
M Stainless Steel < 270HB VP15TF 490 (395 ─ 590) <.098 <.008 <.118 <.008 <.138 <.008
K Cast Iron Tensile strength<450MPa VP15TF 590 (490 ─ 720) <.098 <.012 <.118 <.012 <.138 <.012
H Hardened Steel 45─ 55HRC VP15TF 260 (165 ─ 395) <.098 <.004 <.118 <.004 <.138 <.004
y Helical Milling
ARX25RpppSAppS ARX30RpppSAppS ARX35RpppSAppS
Cutting Speed
Work Material Hardness Grade vc Depth of Cut Feed per Tooth Depth of Cut Feed per Tooth Depth of Cut Feed per Tooth
(SFM) Per Pass ) Per Pass ) Per Pass
( ( (
ap (inch/pass) fz inch/tooth ap (inch/pass) fz inch/tooth ap (inch/pass) fz inch/tooth
) L
P Mild Steel < 180HB VP15TF 590 (490 ─ 720) <.039 <.012 <.039 <.012 <.039 <.012 INDEXABLE MILLING
Carbon Steel, Alloy Steel 180─ 350HB VP15TF 525 (395 ─ 655) <.028 <.008 <.035 <.008 <.039 <.008
M Stainless Steel < 270HB VP15TF 490 (395 ─ 590) <.028 <.008 <.035 <.008 <.039 <.008
K Cast Iron Tensile strength<450MPa VP15TF 590 (490 ─ 720) <.039 <.012 <.039 <.012 <.039 <.012
H Hardened Steel 45─ 55HRC VP15TF 260 (165 ─ 395) <.020 <.004 <.028 <.004 <.039 <.004
Note 1) When helical milling, refer to the machining limits on page L250.
L251