Общий каталог Mitsubishi 2020 - 2021 - страница 1425
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
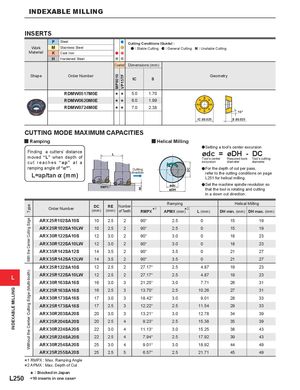
P Steel Cutting Conditions (Guide) :
| Work | M | Stainless Steel | : Stable Cutting : General Cutting : Unstable Cutting | |
| Material | K | Cast Iron | ||
| H | Hardened Steel | |||
| Coated Dimensions (mm) |
| Shape | Order Number | Geometry | |||
| IC | S | ||||
| MP8010 VP15TF |
| RDMW0517M0E | s s | 5.0 | 1.70 |
| RDMW0620M0E | s s | 6.0 | 1.99 |
| RDMW0724M0E | 7.0 | 2.38 |
s s 15° IC ±0.025 S ±0.025 CUTTING MODE MAXIMUM CAPACITIES
y Ramping y Helical Milling
aødc = øDH - DCSetting a tool’s center excursion
Finding a cutters’ distance moved “L” when depth of
| Tool’s center | Required bore | Tool’s cutting | |||
| cut reaches “ap” | at a | excursion | diameter | diameter | |
| ramping angle of “%°”. | For the depth of cut per pass, | ||||
| Cutting | a | ||||
| L=ap/tan % (mm) | direction | refer to the cutting conditions on page |
L251 for helical milling. a Set the machine spindle revolution so RMPX that the tool is rotating and cutting in a down cut direction.
| pe Order Number | DC | RE | Number | 1 | 2 Ramping | Helica | l Milling | |
| Ty | (mm) | (mm) | of Teeth | RMPX | APMX(mm) | L(mm) | DH min.(mm) | DH max.(mm) |
| ARX25R102SA10S dge | 10 | 2.5 | 2 | 90° | 2.5 | 0 | 15 | 19 |
| ARX25R102SA10LW ting E | 10 | 2.5 | 2 | 90° | 2.5 | 0 | 15 | 19 |
| ARX30R122SA10S r Cut | 12 | 3.0 | 2 | 90° | 3.0 | 0 | 18 | 23 |
| ARX30R122SA10LW Cente | 12 | 3.0 | 2 | 90° | 3.0 | 0 | 18 | 23 |
| ARX35R142SA12S the | 14 | 3.5 | 2 | 90° | 3.5 | 0 | 21 | 27 |
| ARX35R142SA12LW With | 14 | 3.5 | 2 | 90° | 3.5 | 0 | 21 | 27 |
| ARX25R122SA10S ) | 12 | 2.5 | 2 | 27.17° | 2.5 | 4.87 | 19 | 23 |
| ARX25R122SA10LW ooth | 12 | 2.5 | 2 | 27.17° | 2.5 | 4.87 | 19 | 23 |
| ARX30R163SA16S ulti-t | 16 | 3.0 | 3 | 21.25° | 3.0 | 7.71 | 26 | 31 |
| ARX25R163SA16S e (M | 16 | 2.5 | 3 | 13.70° | 2.5 | 10.26 | 27 | 31 |
| ARX30R173SA16S Edg | 17 | 3.0 | 3 | 18.42° | 3.0 | 9.01 | 28 | 33 |
| ARX25R173SA16S tting | 17 | 2.5 | 3 | 12.22° | 2.5 | 11.54 | 29 | 33 |
| ARX30R203SA20S r Cu | 20 | 3.0 | 3 | 13.21° | 3.0 | 12.78 | 34 | 39 |
| ARX25R204SA20S ente | 20 | 2.5 | 4 | 9.23° | 2.5 | 15.38 | 35 | 39 |
| ARX30R224SA20S he C | 22 | 3.0 | 4 | 11.13° | 3.0 | 15.25 | 38 | 43 |
| ARX25R224SA20S out t | 22 | 2.5 | 4 | 7.94° | 2.5 | 17.92 | 39 | 43 |
| ARX30R254SA20S With | 25 | 3.0 | 4 | 9.01° | 3.0 | 18.92 | 44 | 49 |
| ARX25R255SA20S | 25 | 2.5 | 5 | 6.57° | 2.5 | 21.71 | 45 | 49 |
*1 RMPX : Max. Ramping Angle
*2 APMX : Max. Depth of Cut
s: Stocked in Japan