Общий каталог Mitsubishi 2020 - 2021 - страница 1380
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
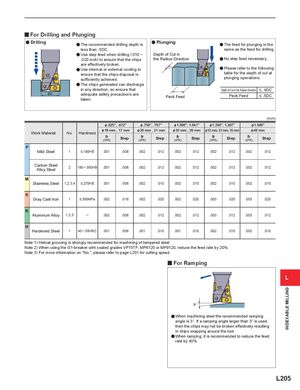
y For Drilling and Plunging
a Drilling a Plunging
aThe recommended drilling depth is a The feed for plunging is the
less than .5DC. same as the feed for drilling.
aUse step feed when drilling (.010 ─ Depth of Cut in
.020 inch) to ensure that the chips the Radius Direction a No step feed necessary.
are effectively broken. Use internal or external cooling to a Please refer to the following a ensure that the chips disposal is table for the depth of cut at
sufficiently achieved. plunging operations.
a The chips generated can discharge
| in any direction, so ensure that | Depth of Cut in the Radius Direction | .4DC | ||
| DC | adequate safety precautions are | Peck Feed | .5DC |
Peck Feed < taken.
(inch)
| Work Material | No. | Hardness | &.625" &16 mm f | , .672" , 17 mm | &.750" &20 mm f | , .797" , 21 mm | &1.000" &25 mm f | , 1.047" , 26 mm | &1.250" &32 mm, 33 f | , 1.297" mm, 35 mm | &1. &40 f | 500" mm | |
| r (IPR) | Step | r (IPR) | Step | r (IPR) | Step | r (IPR) | Step | r (IPR) | Step | ||||
| P | Mild Steel | 1 | .001 | .008 | .002 | .012 | .002 | .012 | .002 | .012 | .002 | .012 | |
| Carbon Steel Alloy Steel | 2 | 180─350HB | .001 | .008 | .002 | .012 | .002 | .012 | .002 | .012 | .002 | .012 | |
| M | Stainless Steel | 1,2,3,4 | .001 | .006 | .002 | .010 | .002 | .010 | .002 | .010 | .002 | .010 | |
| K | Gray Cast Iron | 1 | .002 | .016 | .002 | .020 | .002 | .020 | .003 | .020 | .003 | .020 | |
| N | Aluminum Alloy | 1,2,3 | ─ | .002 | .008 | .002 | .012 | .002 | .012 | .003 | .012 | .003 | .012 |
| H | Hardened Steel | 1 | 40─55HRC | .001 | .006 | .001 | .010 | .001 | .010 | .002 | .010 | .002 | .010 |
Note 1) Helical grooving is strongly recommended for machining of tempered steel. Note 2) When using the G1-breaker wiht coated grades VP15TF, MP6120 or MP9120, reduce the feed rate by 20%. Note 3) For more information on "No.", please refer to page L201 for cutting speed.
y For Ramping
L
3°
a When machining steel the recommended ramping
angle is 3°. If a ramping angle larger than 3° is used,
then the chips may not be broken effectively resulting
in chips wrapping around the tool.
a When ramping, it is recommended to reduce the feed
rate by 40%.