Общий каталог Mitsubishi 2020 - 2021 - страница 1352
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
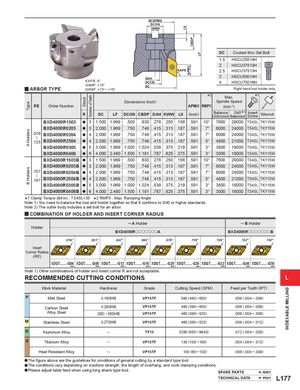
| KAP GAM | R :0° P :+15° | DAH DCC D | KWW DCON B CSFMS | L8 KAPR | CBDP LF APMX | DC 1.5 2 2.5 3 4 | HSCU2 HSCU3 HSCU3 HSCU5 HSCU7 Coolan | 5014H 7513H 7513H 0014H 5016H tthruS | et Bolt | ||||||
| y ARBO | R TYPE | GAM | F :+13°─ | +16° | DC | Right h | and tool | holder only. | |||||||
| RE Type | Order Number | Stock ber of Teeth | Dimen | sions (in | ch) | APMX | RMPX 2 | Ma Spindle (mi | x. Speed n-1) | 1 | |||||
| R Num | DC | LF | DCON | CBDP | DAH | KWW | L8 | (inch) | Balance Unknown | 1 G40 Balanced | Insert Screw | Wrench | |||
| BXD4000R1503 | a 3 | 1.500 | 1.969 | .500 | .630 | .276 | .250 | .156 | .591 | 10° | 7600 | 29000 | TS4SL | TKY15W | |
| s | BXD4000R0203 | a 3 | 2.000 | 1.969 | .750 | .748 | .415 | .313 | .187 | .591 | 7° | 6000 | 24000 | TS4SL | TKY15W |
| .016 lder | BXD4000R0204 | a 4 | 2.000 | 1.969 | .750 | .748 | .415 | .313 | .187 | .591 | 7° | 6000 | 24000 | TS4SL | TKY15W |
| ─ .125 Ho | BXD4000R2504 | a 4 | 2.500 | 1.969 | .750 | .748 | .415 | .313 | .187 | .591 | 5° | 4800 | 21000 | TS4SL | TKY15W |
| A | BXD4000R0305 | a 5 | 3.000 | 1.969 | 1.000 | 1.024 | .539 | .375 | .219 | .591 | 3° | 3800 | 19000 | TS4SL | TKY15W |
| BXD4000R0406 | a 6 | 4.000 | 2.480 | 1.500 | 1.181 | .787 | .625 | .375 | .591 | 3° | 3000 | 16000 | TS4SL | TKY15W | |
| BXD4000R1503B | a 3 | 1.500 | 1.969 | .500 | .630 | .276 | .250 | .156 | .591 | 10° | 7600 | 29000 | TS4SL | TKY15W | |
| s | BXD4000R0203B | a 3 | 2.000 | 1.969 | .750 | .748 | .415 | .313 | .187 | .591 | 7° | 6000 | 24000 | TS4SL | TKY15W |
| .157 der | BXD4000R0204B | a 4 | 2.000 | 1.969 | .750 | .748 | .415 | .313 | .187 | .591 | 7° | 6000 | 24000 | TS4SL | TKY15W |
| ─ .197 Hol | BXD4000R2504B | a 4 | 2.500 | 1.969 | .750 | .748 | .415 | .313 | .187 | .591 | 5° | 4800 | 21000 | TS4SL | TKY15W |
| B | BXD4000R0305B | a 5 | 3.000 | 1.969 | 1.000 | 1.024 | .539 | .375 | .219 | .591 | 3° | 3800 | 19000 | TS4SL | TKY15W |
| BXD4000R0406B | a 6 | 4.000 | 2.480 | 1.500 | 1.181 | .787 | .625 | .375 | .591 | 3° | 3000 | 16000 | TS4SL | TKY15W |
*1 Clamp Torque (lbf-in) : TS4SL=35 *2 RMPX : Max. Ramping Angle
Note 1) You need to balance the tool and holder together so that it confirms to G40 or higher standards. Note 2) The cutter body includes a set bolt for an arbor.
y COMBINATION OF HOLDER AND INSERT CORNER RADIUS
~ A Holder ~ B Holder Holder BXD4000RoooooooA BXD4000RoooooooB
.016" .031" .047" .063" .079" .118" .126" .157" .197"
Insert Corner Radius (RE) XDGT........-G04 XDGT........-G08 XDGT........-G12 XDGT........-G16 XDGT........-G20 XDGT........-G30 XDGT........-G32 XDGT........-G40 XDGT........-G50
Note 1) Other combinations of holder and insert corner R are not acceptable.
RECOMMENDED CUTTING CONDITIONS L
| Work Material | Hardness | Grade | Cutting Speed (SFM) | Feed per Tooth (IPT) |
| P Mild Steel | VP15TF | 590 (490─655) | .006 (.004─.008) | |
| Carbon Steel | VP15TF | 490 (390─655) | .006 (.004─.008) | |
| Alloy Steel | 280─350HB | VP15TF | 460 (390─525) | .006 (.004─.008) |
| M Stainless Steel | VP15TF | 460 (390─525) | .008 (.004─.012) | |
| N Aluminum Alloy | ─ | TF15 | 3280 (655─9840) | .012 (.004─.020) |
| S Titanium Alloy | ─ | VP15TF | 130 (100─195) | .004 (.004─.012) |
| Heat Resistant Alloy | ─ | VP15TF | 100 (65─130) | .006 (.004─.008) |
aThe figure above are the guidelines for conditions of general cutting by a standard type tool. aThe conditions vary depending on machine strength, the length of overhang, and work clamping conditions. aPlease adjust table feed when using long shank type tool. SPARE PARTS