Общий каталог Mitsubishi 2020 - 2021 - страница 1339
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
INDEXABLE MILLING
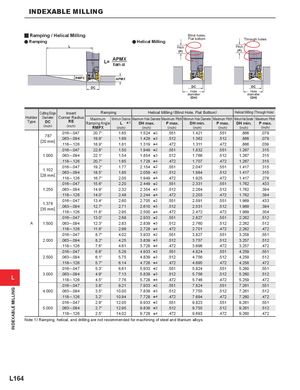
y Ramping / Helical Milling Blind holes,
Flat bottom Through holes
a Ramping a Helical Milling
L Pitch Pitch
(P) (P)
APMX
L=
tan %
RMPX APMX
DC DC DC
Hole Hole
diameter diameter
(DH) (DH)
Cutting Edge Insert Ramping Helical Milling (Blind Hole, Flat Bottom) Helical Milling (Through Hole)
Holder Diameter Corner Radius Maximum Minimum Distance Maximum Hole Diameter Maximum Pitch Minimum Hole Diameter Maximum Pitch Minimum Hole Diameter Maximum Pitch
Type DC RE
(inch) (inch)
Ramping Angle
RMPX
L 1
(inch) *
DH max.
(inch)
P max.
(inch)
DH min.
(inch)
P max.
(inch)
DH min.
(inch)
P max.
(inch)
.787
.016─.047 20.7° 1.65
*3 1.524 2 .551 1.421 .551 .866 .079
[20 mm]
.063─.094 19.9° 1.69
*4 1.429 .512 1.362 .512 .866 .079
.118─.126 18.9° 1.81
*2 1.319 .472 1.311 .472 .866 .039
.016─.047 22.6° 1.50
*3 1.949 .551 1.832 .551 1.267 .315
1.000 .063─.094 22.1° 1.54
*4 1.854 .512 1.766 .512 1.267 .315
.118─.126 20.7° 1.65
*2 1.728 .472 1.707 .472 1.267 .315
1.102
.016─.047 19.2° 1.77
*3 2.154 .551 2.047 .551 1.417 .315
[28 mm]
.063─.094 18.5° 1.85
*4 2.059 .512 1.984 .512 1.417 .315
.118─.126 16.7° 2.05
*2 1.949 .472 1.925 .472 1.417 .276
.016─.047 15.6° 2.20
*3 2.449 .551 2.331 .551 1.762 .433
1.250 .063─.094 14.9° 2.32
*4 2.354 .512 2.264 .512 1.762 .394
.118─.126 14.0° 2.48
*2 2.244 .472 2.203 .472 1.762 .394
1.378
.016─.047 13.4° 2.60
*3 2.705 .551 2.591 .551 1.969 .433
[35 mm]
.063─.094 12.7° 2.71
*4 2.610 .512 2.531 .512 1.969 .394
.118─.126 11.8° 2.95
*2 2.500 .472 2.472 .472 1.969 .354
.016─.047 13.0° 2.68
*3 2.933 .551 2.827 .551 2.262 .512
A 1.500 .063─.094 12.3° 2.83
*4 2.839 .512 2.760 .512 2.262 .512
.118─.126 11.6° 2.99
*2 2.728 .472 2.701 .472 2.262 .472
.016─.047 8.7° 4.02
*3 3.933 .551 3.827 .551 3.258 .551
2.000 .063─.094 8.2° 4.25
*4 3.839 .512 3.757 .512 3.257 .512
.118─.126 7.6° 4.61
*2 3.728 .472 3.696 .472 3.257 .472
.016─.047 6.6° 5.28
*3 4.933 .551 4.824 .551 4.259 .551
2.500 .063─.094 6.1° 5.75
*4 4.839 .512 4.756 .512 4.259 .512
.118─.126 5.7° 6.14
*2 4.728 .472 4.695 .472 4.258 .472
.016─.047 5.3° 6.61
*3 5.933 .551 5.824 .551 5.260 .551
L
3.000 .063─.094 4.9° 7.13
*4 5.839 .512 5.756 .512 5.260 .512
.118─.126 4.5° 7.76
*2 5.728 .472 5.746 .472 5.259 .472
.016─.047 3.8° 9.21
*3 7.933 .551 7.824 .551 7.261 .551
INDEXABLE MILLING
4.000 .063─.094 3.5° 10.00
*4 7.839 .512 7.755 .512 7.261 .512
.118─.126 3.2° 10.94
*2 7.728 .472 7.694 .472 7.260 .472
.016─.047 2.9° 12.05
*3 9.933 .551 9.823 .551 9.261 .551
5.000 .063─.094 2.7° 12.95
*4 9.839 .512 9.755 .512 9.261 .512
.118─.126 2.5° 14.02
* 9.728 .472
Note 1) Ramping, helical, and drilling are not recommended for machining of steel and titanium alloys.
9.693 .472 9.260 .472
L164