Общий каталог Mitsubishi 2020 - 2021 - страница 1330
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
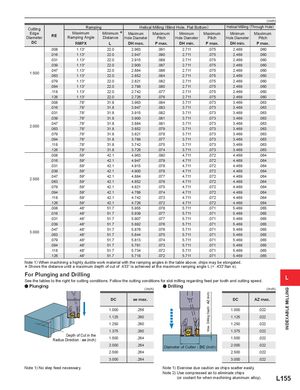
| Cutting | Rampin | g | Helica | l Milling (Blin | d Hole, Flat Bot | tom) | Helical Milling ( | Through Hole) | |
| Edge Diameter DC | RE | Maximum Ramping Angle RMPX | Minimum Distance L | Maximum Hole Diameter DH max. | Maximum Pitch P max. | Minimum Hole Diameter DH min. | Maximum Pitch P max. | Minimum Hole Diameter DH min. | Maximum Pitch P max. |
| .008 | 1.13° | 22.0 | 2.963 | .091 | 2.711 | .075 | 2.469 | .060 | |
| .016 | 1.13° | 22.0 | 2.947 | .090 | 2.711 | .075 | 2.469 | .060 | |
| .031 | 1.13° | 22.0 | 2.915 | .088 | 2.711 | .075 | 2.469 | .060 | |
| .039 | 1.13° | 22.0 | 2.900 | .087 | 2.711 | .075 | 2.469 | .060 | |
| 1500 | .047 | 1.13° | 22.0 | 2.884 | .086 | 2.711 | .075 | 2.469 | .060 |
| . | .063 | 1.13° | 22.0 | 2.852 | .084 | 2.711 | .075 | 2.469 | .060 |
| .079 | 1.13° | 22.0 | 2.821 | .082 | 2.711 | .075 | 2.469 | .060 | |
| .094 | 1.13° | 22.0 | 2.789 | .080 | 2.711 | .075 | 2.469 | .060 | |
| .118 | 1.13° | 22.0 | 2.742 | .077 | 2.711 | .075 | 2.469 | .060 | |
| .126 | 1.13° | 22.0 | 2.726 | .076 | 2.711 | .075 | 2.469 | .060 | |
| .008 | .78° | 31.8 | 3.963 | .084 | 3.711 | .073 | 3.469 | .063 | |
| .016 | .78° | 31.8 | 3.947 | .083 | 3.711 | .073 | 3.469 | .063 | |
| .031 | .78° | 31.8 | 3.915 | .082 | 3.711 | .073 | 3.469 | .063 | |
| .039 | .78° | 31.8 | 3.900 | .081 | 3.711 | .073 | 3.469 | .063 | |
| .047 | .78° | 31.8 | 3.884 | .081 | 3.711 | .073 | 3.469 | .063 | |
| 2.000 | .063 | .78° | 31.8 | 3.852 | .079 | 3.711 | .073 | 3.469 | .063 |
| .079 | .78° | 31.8 | 3.821 | .078 | 3.711 | .073 | 3.469 | .063 | |
| .094 | .78° | 31.8 | 3.789 | .077 | 3.711 | .073 | 3.469 | .063 | |
| .118 | .78° | 31.8 | 3.742 | .075 | 3.711 | .073 | 3.469 | .063 | |
| .126 | .78° | 31.8 | 3.726 | .074 | 3.711 | .073 | 3.469 | .063 | |
| .008 | .59° | 42.1 | 4.963 | .080 | 4.711 | .072 | 4.469 | .064 | |
| .016 | .59° | 42.1 | 4.947 | .079 | 4.711 | .072 | 4.469 | .064 | |
| .031 | .59° | 42.1 | 4.915 | .078 | 4.711 | .072 | 4.469 | .064 | |
| .039 | .59° | 42.1 | 4.900 | .078 | 4.711 | .072 | 4.469 | .064 | |
| .047 | .59° | 42.1 | 4.884 | .077 | 4.711 | .072 | 4.469 | .064 | |
| 2.500 | .063 | .59° | 42.1 | 4.852 | .076 | 4.711 | .072 | 4.469 | .064 |
| .079 | .59° | 42.1 | 4.821 | .075 | 4.711 | .072 | 4.469 | .064 | |
| .094 | .59° | 42.1 | 4.789 | .074 | 4.711 | .072 | 4.469 | .064 | |
| .118 | .59° | 42.1 | 4.742 | .073 | 4.711 | .072 | 4.469 | .064 | |
| .126 | .59° | 42.1 | 4.726 | .072 | 4.711 | .072 | 4.469 | .064 | |
| .008 | .48° | 51.7 | 5.955 | .078 | 5.711 | .071 | 5.469 | .065 | |
| .016 | .48° | 51.7 | 5.939 | .077 | 5.711 | .071 | 5.469 | .065 | |
| .031 | .48° | 51.7 | 5.907 | .077 | 5.711 | .071 | 5.469 | .065 | |
| .039 | .48° | 51.7 | 5.892 | .076 | 5.711 | .071 | 5.469 | .065 | |
| .047 | .48° | 51.7 | 5.876 | .076 | 5.711 | .071 | 5.469 | .065 | |
| 3.000 | .063 | .48° | 51.7 | 5.844 | .075 | 5.711 | .071 | 5.469 | .065 |
| .079 | .48° | 51.7 | 5.813 | .074 | 5.711 | .071 | 5.469 | .065 | |
| .094 | .48° | 51.7 | 5.781 | .073 | 5.711 | .071 | 5.469 | .065 | |
| .118 | .48° | 51.7 | 5.734 | .072 | 5.711 | .071 | 5.469 | .065 | |
| .126 | .48° | 51.7 | 5.718 | .072 | 5.711 | .071 | 5.469 | .065 |
Note 1) When machining a highly ductile work material with the ramping angles in the table above, chips may be elongated.* Shows the distance until a maximum depth of cut of .433” is achieved at the maximum ramping angle L (= .433”/tan α).
For Plunging and Drilling L
See the tables to the right for cutting conditions. Follow the cutting conditions for slot milling regarding feed per tooth and cutting speed.
a Plunging a Drilling
(inch) (inch)
| DC | ae max. | DC | AZ max. |
| 1.000 | .256 | 1.000 | .022 |
| 1.125 | .260 | 1.125 | .022 |
| 1.250 | .260 | 1.250 | .022 |
| 1.375 | .260 | 1.375 | .022 |
| Depth of Cut in the | |||
| Radius Direction : ae (inch) 1.500 | .264 | 1.500 | .022 |
| 2.000 | .264 | Diameter of Cutter : DC (inch) 2.000 | .022 |
| 2.500 | .264 | 2.500 | .022 |
Note 1) No step feed necessary. Note 1) Exercise due caution as chips scatter easily. Note 2) Use compressed air to eliminate chips