Общий каталог Mitsubishi 2020 - 2021 - страница 1297
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
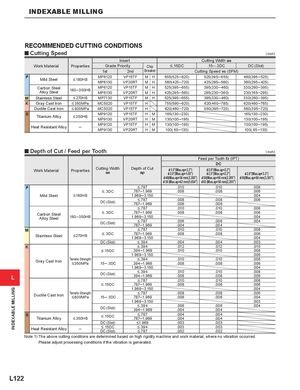
RECOMMENDED CUTTING CONDITIONS
| y C | utting Speed | (inch) | ||||||
| Insert | CuttingWidth ae | |||||||
| Work Material | Properties | Grade | Priority | Chip | .15─.3DC | DC (Slot) | ||
| 1st | 2nd | Breaker | CuttingSpeedvc (SFM | ) | ||||
| P | Mild Sl | MP6120 | VP15TF | M H | 655(525─820) | 525(395─655) | 460(395─525) | |
| tee | MP6130 | VP20RT | M H | 560(425─720) | 425(295─560) | 360(295─425) | ||
| Carbon Steel | 180350HB | MP6120 | VP15TF | M H | 525(395─655) | 395(330─460) | 330(260─395) | |
| AlloySteel | ─ | MP6130 | VP20RT | M H | 425(295─560) | 295(230─360) | 230(165─295) | |
| M | Stainless Steel | MP7130 | VP15TF | M H | 525(395─655) | 395(330─460) | 330(260─395) | |
| K | GrayCast Iron | MC5020 | VP15TF | H | 755(590─920) | 620(460─785) | 620(460─785) | |
| Ductile Cast Iron | MC5020 | VP15TF | H | 620(460─720) | 560(395─720) | 560(395─720) | ||
| S | MP9120 | VP15TF | H M | 165(130─230) | 165(130─230) | |||
| Titanium Alloy | MP9130 | VP20RT | H M | 130(100─195) | 130(100─195) | |||
| H | t Ritt All | MP9120 | VP15TF | H M | 130(100─195) | 130(100─195) | ||
| a essan oy | ─ | MP9130 | VP20RT | H M | 100(65─130) | 100(65─130) |
| y Depth of Cut / | Feedper | ooth | (inch) | ||||
| Cttin Width | Dth f Ct | "" | DC "" Feed per Toothfz (IPT | ) | |||
| Work Material | Properties | ug ae | epou ap | &1.5(Max.ap=2.2) &2.0"(Max.ap=1.65") &40(Max.ap=56 mm(2.205") &50 (Max.ap=42 mm(1.654") | &2.0(Max.ap=2.2) &2.5"(Max.ap=2.2") &50(Max.ap=56 mm(2.205") &63 (Max.ap=56 mm(2.205") | &2.0"(Max.ap= &50(Max.ap=84 m | 3.3") m(3.307") |
| P | .010 | .010 | .008 | ||||
| .787─1.969 | .008 | .008 | .006 | ||||
| Mild Steel | 1.969─3.150 | .004 | |||||
| DCSlt | .008 | .008 | .006 | ||||
| (o) | .787─1.969 | .006 | .006 | ||||
| .010 | .010 | .008 | |||||
| Carbon Steel | .787─1.969 | .008 | .008 | .006 | |||
| Alloy Steel | 180─350HB | 1.969─3.150 | .004 | ||||
| DC(Slot) | .006 | .006 | .004 | ||||
| .787─1.969 | .004 | .004 | |||||
| M | .010 | .010 | .008 | ||||
| Stil Stl | .787─1.969 | .008 | .008 | .006 | |||
| aness ee | 1.969─3.150 | .004 | |||||
| DC (Slot) | .004 | .004 | .003 | ||||
| K | .012 | .012 | .010 | ||||
| .394─1.969 | .010 | .010 | .008 | ||||
| 1.969─3.150 | .006 | ||||||
| Gra Cast Iron | Tensile Strength | .010 | .010 | .008 | |||
| y | .15─.3DC | .394─1.969 | .008 | .008 | .006 | ||
| 1.969─3.150 | .004 | ||||||
| DC(Slot) | .010 | .010 | .008 | ||||
| .394─1.969 | .008 | .008 | .006 | ||||
| .010 | .010 | .008 | |||||
| .787─1.969 | .008 | .008 | .006 | ||||
| 1.969─3.150 | .004 | ||||||
| Ductile Cast Iron | Tensile Strength | .008 | .008 | .006 | |||
| .15─.3DC | .787─1.969 | .006 | .006 | .004 | |||
| 1.969─3.150 | .003 | ||||||
| DCSl | .006 | .006 | .004 | ||||
| (ot) | .394─1.969 | .004 | .004 | ||||
| S | .004 | .004 | |||||
| Titanium Alloy | . | .787─1.969 | .004 | .004 | |||
| DC (Slot) | .003 | .003 | |||||
| Heat Resistant Allo | ─ | .003 | .003 | ||||
| y | DC(Slot) | .002 | .002 |
Note 1) The above cutting conditons are determined based on high rigidity machine and work material, where no vibration occurred. Please adjust processing conditions if the vibration is generated.