Общий каталог Mitsubishi 2020 - 2021 - страница 1201
Навигация
 Каталог Mitsubishi Materials запасные части
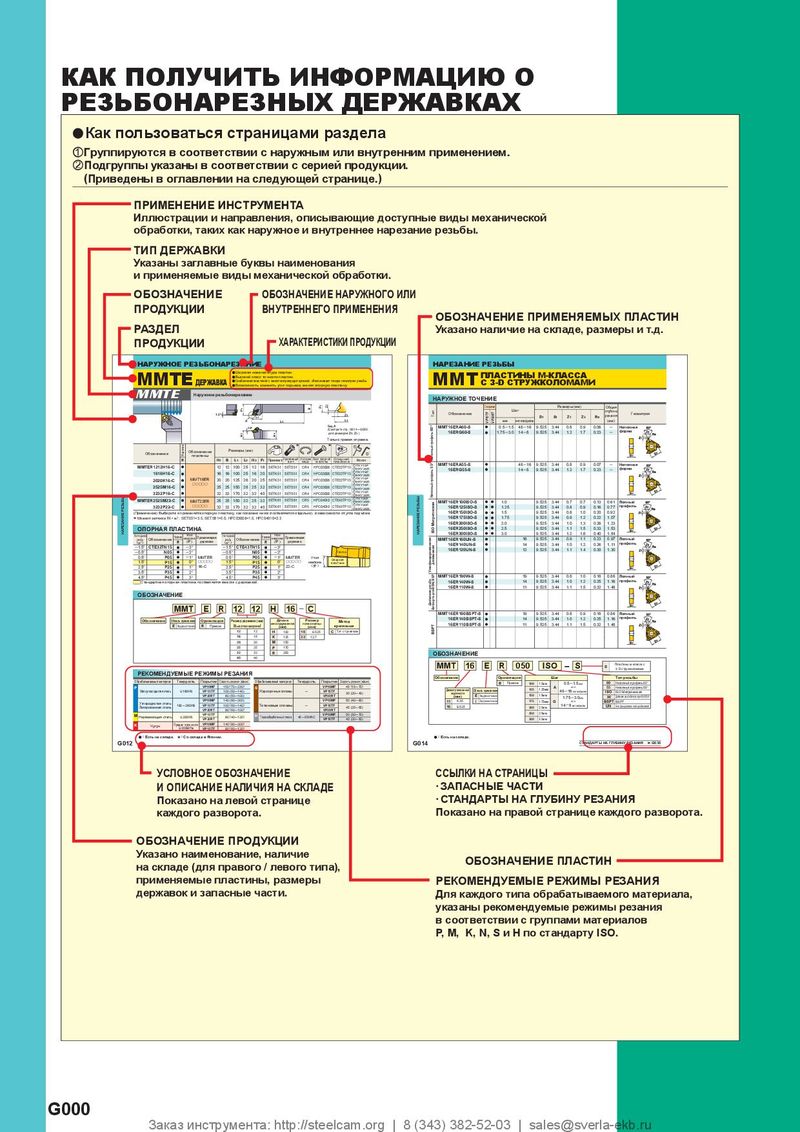 Каталог Mitsubishi Materials резьбонарезной инструмент
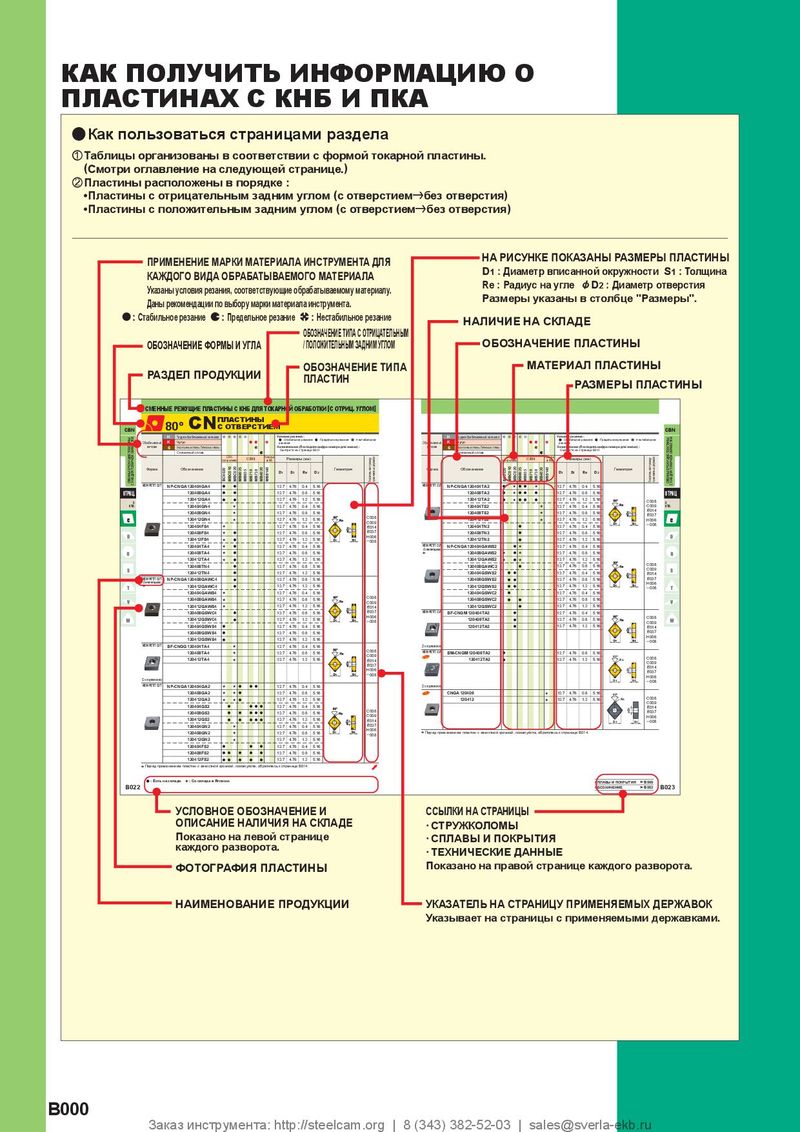 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
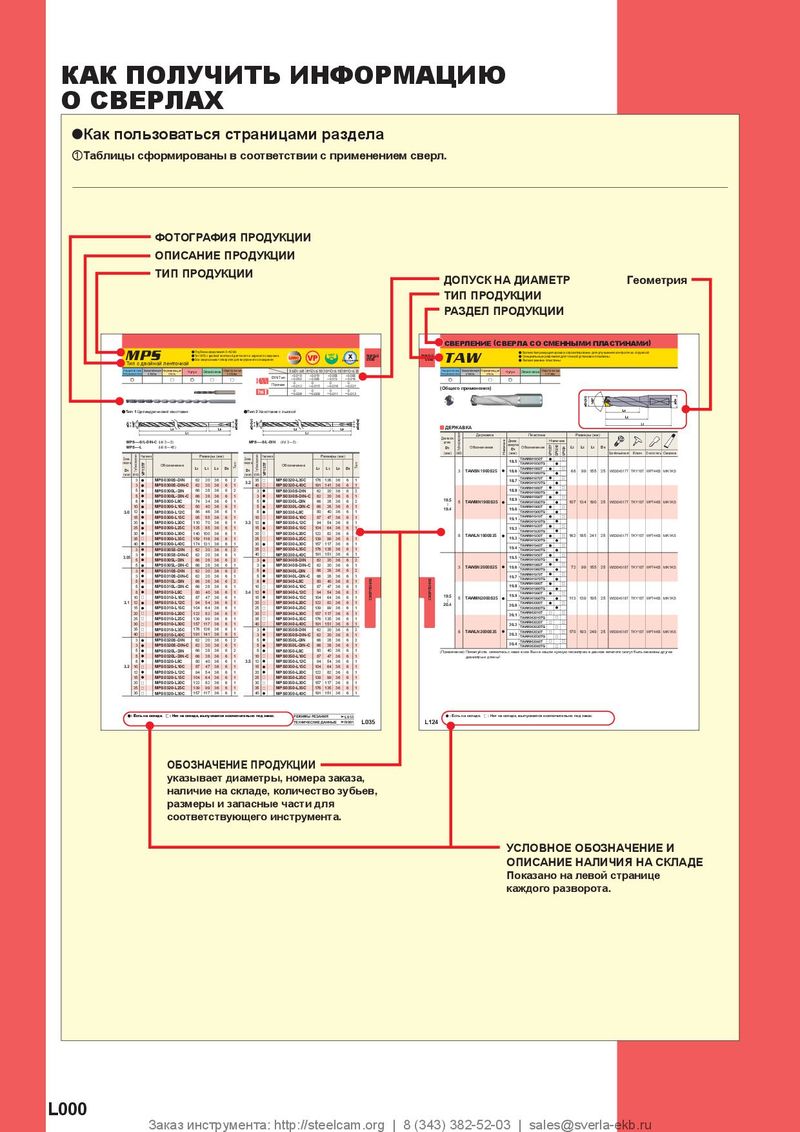 Каталог Mitsubishi Materials сверлильные инструменты
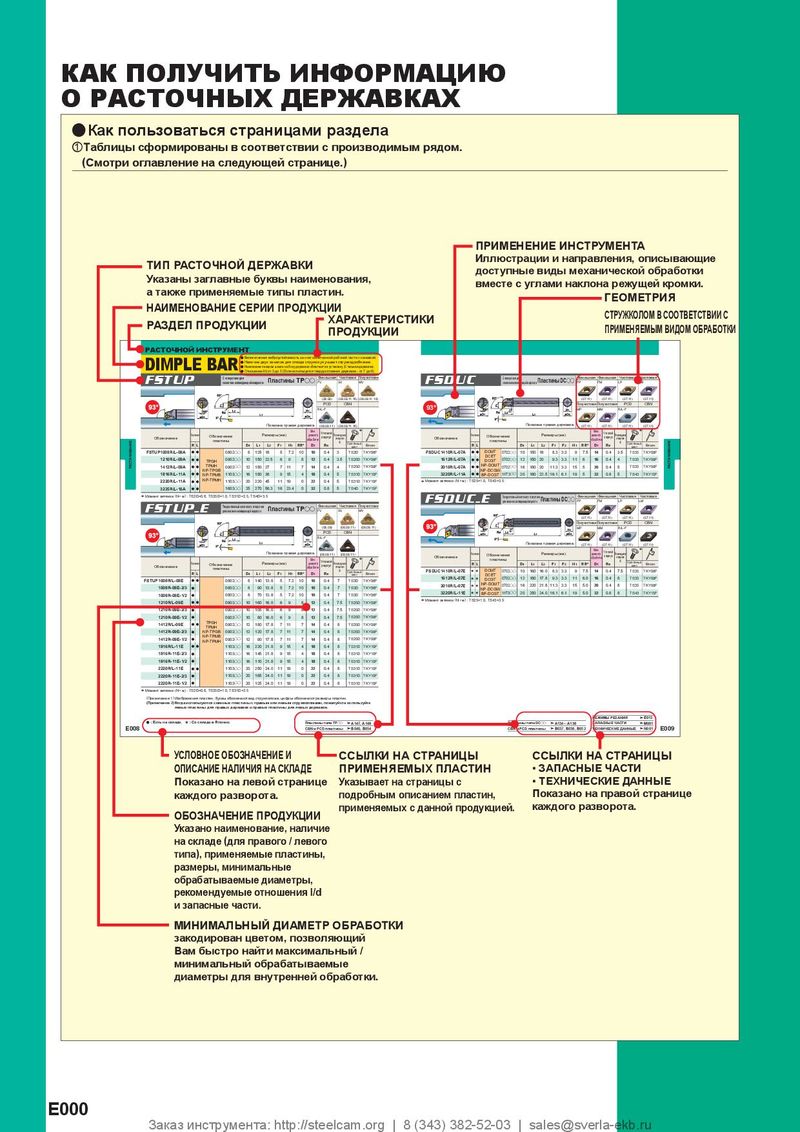 Каталог Mitsubishi Materials расточной инструмент
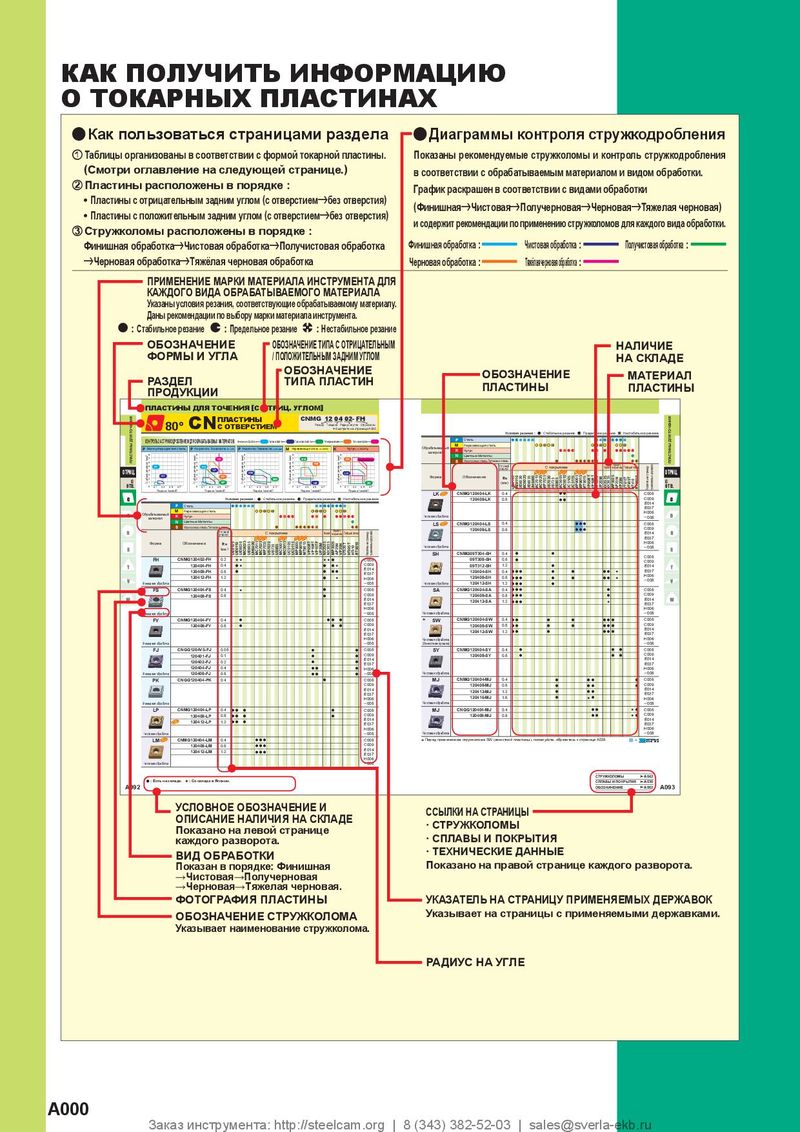 Каталог Mitsubishi Materials пластины для точения
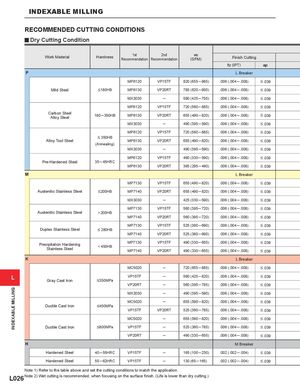
y Dry Cutting Condition
| Work Material | Hardness | 1st Recommendation | 2nd Recommendation | vc (SFM) | Finish Cutting | |
| fz(IPT) | ap | |||||
| P | L Breaker | |||||
| MP6120 | VP15TF | 820 (655─985) | .006 (.004─.008) | |||
| Mild Steel | MP6130 | VP20RT | 785 (620─950) | .006 (.004─.008) | ||
| MX3030 | ─ | 590 (425─755) | .006 (.004─.008) | |||
| MP6120 | VP15TF | 720 (560─885) | .006 (.004─.008) | |||
| Carbon Steel Alloy Steel | 180─350HB | MP6130 | VP20RT | 655 (490─820) | .006 (.004─.008) | |
| MX3030 | ─ | 490 (395─590) | .006 (.004─.008) | |||
| MP6120 | VP15TF | 720 (560─885) | .006 (.004─.008) | |||
| Alloy Tool Steel | (Annealing) | MP6130 | VP20RT | 655 (490─820) | .006 (.004─.008) | |
| MX3030 | ─ | 490 (395─590) | .006 (.004─.008) | |||
| 3545HRC | MP6120 | VP15TF | 460 (330─590) | .006 (.004─.008) | ||
| Pre-Hardened Steel | ─ | MP6130 | VP20RT | 395 (295─490) | .006 (.004─.008) | |
| M | L Breaker | |||||
| MP7130 | VP15TF | 655 (490─820) | .006 (.004─.008) | |||
| Austenitic Stainless Steel | MP7140 | VP20RT | 655 (490─820) | .006 (.004─.008) | ||
| MX3030 | ─ | 425 (330─590) | .006 (.004─.008) | |||
| MP7130 | VP15TF | 560 (395─720) | .006 (.004─.008) | |||
| Austenitic Stainless Steel | >200HB | MP7140 | VP20RT | 560 (395─720) | .006 (.004─.008) | |
| Dulex Stainless Steel | MP7130 | VP15TF | 525 (360─690) | .006 (.004─.008) | ||
| p | MP7140 | VP20RT | 525 (360─690) | .006 (.004─.008) | ||
| Precipitation Hardening | < 450HB | MP7130 | VP15TF | 490 (330─655) | .006 (.004─.008) | |
| Stainless Steel | MP7140 | VP20RT | 490 (330─655) | .006 (.004─.008) | ||
| K | L Breaker | |||||
| MC5020 | ─ | 720 (655─885) | .006 (.004─.008) | |||
| VP15TF | ─ | 590 (425─820) | .006 (.004─.008) | |||
| Gray Cast Iron | 350MPa | VP20RT | ─ | 560 (395─785) | .006 (.004─.008) | |
| MX3030 | ─ | 490 (395─590) | .006 (.004─.008) | |||
| MC5020 | ─ | 655 (590─820) | .006 (.004─.008) | |||
| Ductile Cast Iron | VP15TF | VP20RT | 525 (360─785) | .006 (.004─.008) | ||
| MC5020 | ─ | 655 (590─820) | .006 (.004─.008) | |||
| Ductile Cast Iron | VP15TF | ─ | 525 (360─785) | .006 (.004─.008) | ||
| VP20RT | ─ | 490 (330─655) | .006 (.004─.008) | |||
| H | M Breaker | |||||
| Hardened Steel | 40─55HRC | VP15TF | ─ | 165 (100─230) | .002 (.002─.004) | |
| Hardened Steel | 55─62HRC | VP15TF | ─ | 130 (65─165) | .002 (.002─.004) |
Note 1) Refer to the table above and set the cutting conditions to match the application.