Общий каталог Mitsubishi 2020 - 2021 - страница 1684
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
NOTES ON USE
y INSERT INSTALLATION
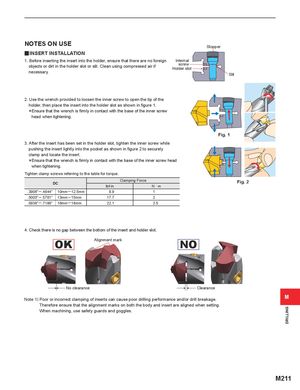
1. Before inserting the insert into the holder, ensure that there are no foreign objects or dirt in the holder slot or slit. Clean using compressed air if necessary.
Internal screw Holder slot
Stopper
Slit
2. Use the wrench provided to loosen the inner screw to open the tip of the holder, then place the insert into the holder slot as shown in figure 1.
- Ensure that the wrench is firmly in contact with the base of the inner screw head when tightening.
3. After the insert has been set in the holder slot, tighten the inner screw while pushing the insert lightly into the pocket as shown in figure 2 to securely clamp and locate the insert.
- Ensure that the wrench is firmly in contact with the base of the inner screw head when tightening.
Tighten clamp screws referring to the table for torque.
Fig. 1
open
ope n
| C | Clampi | ngForce | |
| lbf-in | N · m | ||
| .3906"─.4844" | 10mm─12.5mm | 8.9 | 1 |
| .5000"─.5781" | 13mm─15mm | 17.7 | 2 |
| .5938"─.7188" | 16mm─18mm | 22.1 | 2.5 |
4. Check there is no gap between the bottom of the insert and holder slot.
OK Alignment mark NO
No clearance Clearance
M
Note 1) Poor or incorrect clamping of inserts can cause poor drilling performance and/or drill breakage. Therefore ensure that the alignment marks on both the body and insert are aligned when setting. When machining, use safety guards and goggles.