Общий каталог Mitsubishi 2020 - 2021 - страница 1456
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
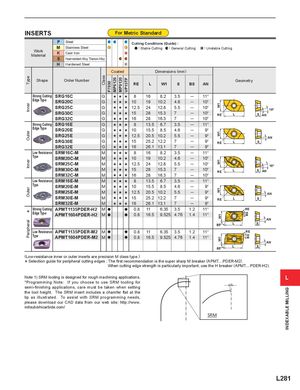
| IN pe | SERTS Work Material | P M K S H Steel Stainless Steel Cast Iron Heat-resistant Alloy, Titanium Hardened Steel | Alloy ss | 0 F Coa | 0 F orMe ted | tric S Cuttin :S | tanda g Condit table Cu | rd ions (Gui tting : Dimensio | de) : General ns (mm | Cutting ) | :Uns | table Cutting | ||
| Ty | Shape | Order Number | Cla | F7030 | MP612 | MP912 VP15T | RE | L | W1 | S | BS | AN | Geometr | y |
| Strong Cutting | SRG16C | G | s | s s | 8 | 16 | 8.2 | 3.5 | ─ | 11° | ||||
| r | Edge Type | SRG20C | G | s | s s | 10 | 19 | 10.2 | 4.6 | ─ | 10° | 1 | ||
| nne | SRG25C | G | s | s s | 12.5 | 24 | 12.8 | 5.5 | ─ | 10° | W | 18° | ||
| I | SRG30C | G | s | s s | 15 | 28 | 15.3 | 7 | ─ | 10° | L RE | S AN | ||
| SRG32C | G | s | s s | 16 | 28 | 16.3 | 7 | ─ | 10° | |||||
| Strong Cutting | SRG16E | G | s | s s | 8 | 13.5 | 6.7 | 3.5 | ─ | 11° | ||||
| er | Edge Type | SRG20E | G | s | s s | 10 | 15.5 | 8.5 | 4.6 | ─ | 9° | 1 | ||
| ut | SRG25E | G | s | s s | 12.5 | 20.5 | 10.2 | 5.5 | ─ | 9° | W | AN | ||
| O | SRG30E | G | s | s s | 15 | 25.2 | 12.2 | 7 | ─ | 9° | L RE | S | ||
| SRG32E | G | s | s s | 16 | 26.1 | 13.1 | 7 | ─ | 9° | |||||
| Low Resistance | SRM16C-M | M | s | s s | 8 | 16 | 8.2 | 3.5 | ─ | 11° | ||||
| r | Type | SRM20C-M | M | s | s s | 10 | 19 | 10.2 | 4.6 | ─ | 10° | |||
| nne | SRM25C-M | M | s | s s | 12.5 | 24 | 12.8 | 5.5 | ─ | 10° | W1 | 18° | ||
| I | SRM30C-M | M | s | s s | 15 | 28 | 15.3 | 7 | ─ | 10° | L RE | AN S | ||
| SRM32C-M | M | s | s s | 16 | 28 | 16.3 | 7 | ─ | 10° | |||||
| Low Resistance | SRM16E-M | M | s | s s | 8 | 13.5 | 6.7 | 3.5 | ─ | 11° | ||||
| r | Type | SRM20E-M | M | s | s s | 10 | 15.5 | 8.5 | 4.6 | ─ | 9° | |||
| ute | SRM25E-M | M | s | s s | 12.5 | 20.5 | 10.2 | 5.5 | ─ | 9° | W1 | AN | ||
| O | SRM30E-M | M | s | s s | 15 | 25.2 | 12.2 | 7 | ─ | 9° | L RE | S | ||
| SRM32E-M | M | s | s s | 16 | 26.1 | 13.1 | 7 | ─ | 9° | |||||
| Strong Cutting Edge Type | APMT1135PDER-H2 APMT1604PDER-H2 | M M | a a | a a | 0.8 0.8 | 11 16.5 | 6.35 9.525 | 3.5 4.76 | 1.2 1.4 | 11° 11° | RE BS 1 | |||
| eral | W L | AN S | ||||||||||||
| riph | Low Resistance | APMT1135PDER-M2 | M | a | a | 0.8 | 11 | 6.35 | 3.5 | 1.2 | 11° | RE | ||
| Pe | Type | APMT1604PDER-M2 | M | a | a | 0.8 | 16.5 | 9.525 | 4.76 | 1.4 | 11° | BS W1 L | AN S |
(Low-resistance inner or outer inserts are precision M class type.) * Selection guide for peripheral cutting edges : The first recommendation is the super sharp M breaker (APMT....PDER-M2). When cutting edge strength is particularly important, use the H breaker (APMT....PDER-H2). Note 1) SRM tooling is designed for rough machining applications. L *Programming Note: If you choose to use SRM tooling for semi-finishing applications, care must be taken when setting the tool height. The SRM insert includes a chamfer flat at the tip as illustrated. To assist with SRM programming needs, please download our CAD data from our web site; http://www. mitsubishicarbide.com/