Общий каталог Mitsubishi 2020 - 2021 - страница 1444
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
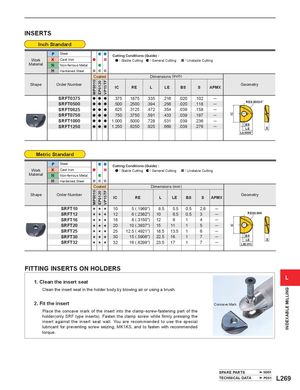
INSERTS
Inch Standard
P Steel
Cutting Conditions (Guide) :
Work K Cast Iron : Stable Cutting : General Cutting : Unstable Cutting
Material N Non-ferrous Metal
H Hardened Steel
Coated Dimensions (inch)
MP8010
VP15TF
EP6120
Shape Order Number Geometry
IC RE L LE BS S APMX
SRFT0375 a a a .375 .1875 .335 .216 .020 .102 ─
RE±.00024"
SRFT0500 a a a .500 .2500 .394 .256 .020 .118 ─
SRFT0625 a a a .625 .3125 .472 .354 .039 .158 ─
SRFT0750
IC
a a a .750 .3750 .591 .433 .039 .197 ─
SRFT1000 a a a 1.000 .5000 .728 .531 .039 .236 ─
BS
SRFT1250 a a a 1.250 .6250 .925 .669 .039 .276 ─ LE S
L±.0006"
Metric Standard
P Steel
Cutting Conditions (Guide) :
Work K Cast Iron : Stable Cutting : General Cutting : Unstable Cutting
Material N Non-ferrous Metal
H Hardened Steel
Coated Dimensions (mm)
MP8010
VP15TF
EP6120
Shape Order Number Geometry
IC RE L LE BS S APMX
SRFT10 s s s 10 5 (.1969") 8.5 5.5 0.5 2.6 ─
SRFT12 s s s 12 6 (.2362") 10 6.5 0.5 3 ─ RE±0.006
SRFT16 s s s 16 8 (.3150") 12 9 1 4 ─
SRFT20 20 10 (.3937") 15 11 1 5 ─
IC
s s s
SRFT25 s s s 25 12.5 (.4921") 18.5 13.5 1 6 ─
SRFT30 s s s 30 15 (.5906") 22.5 16 1 7 ─ BS
LE S
SRFT32 s s s 32 16 (.6299") 23.5 17 1 7 ─ L±0.015
FITTING INSERTS ON HOLDERS
L
1. Clean the insert seat
Clean the insert seat in the holder body by blowing air or using a brush.
INDEXABLE MILLING
2. Fit the insert Concave Mark
Place the concave mark of the insert into the clamp-screw-fastening part of the
holder(only SRF type inserts). Fasten the clamp screw while firmly pressing the
insert against the insert seat wall. You are recommended to use the special
lubricant for preventing screw seizing, MK1KS, and to fasten with recommended
torque.
SPARE PARTS N001
TECHNICAL DATA P001 L269
Inch Standard
P Steel
Cutting Conditions (Guide) :
Work K Cast Iron : Stable Cutting : General Cutting : Unstable Cutting
Material N Non-ferrous Metal
H Hardened Steel
Coated Dimensions (inch)
MP8010
VP15TF
EP6120
Shape Order Number Geometry
IC RE L LE BS S APMX
SRFT0375 a a a .375 .1875 .335 .216 .020 .102 ─
RE±.00024"
SRFT0500 a a a .500 .2500 .394 .256 .020 .118 ─
SRFT0625 a a a .625 .3125 .472 .354 .039 .158 ─
SRFT0750
IC
a a a .750 .3750 .591 .433 .039 .197 ─
SRFT1000 a a a 1.000 .5000 .728 .531 .039 .236 ─
BS
SRFT1250 a a a 1.250 .6250 .925 .669 .039 .276 ─ LE S
L±.0006"
Metric Standard
P Steel
Cutting Conditions (Guide) :
Work K Cast Iron : Stable Cutting : General Cutting : Unstable Cutting
Material N Non-ferrous Metal
H Hardened Steel
Coated Dimensions (mm)
MP8010
VP15TF
EP6120
Shape Order Number Geometry
IC RE L LE BS S APMX
SRFT10 s s s 10 5 (.1969") 8.5 5.5 0.5 2.6 ─
SRFT12 s s s 12 6 (.2362") 10 6.5 0.5 3 ─ RE±0.006
SRFT16 s s s 16 8 (.3150") 12 9 1 4 ─
SRFT20 20 10 (.3937") 15 11 1 5 ─
IC
s s s
SRFT25 s s s 25 12.5 (.4921") 18.5 13.5 1 6 ─
SRFT30 s s s 30 15 (.5906") 22.5 16 1 7 ─ BS
LE S
SRFT32 s s s 32 16 (.6299") 23.5 17 1 7 ─ L±0.015
FITTING INSERTS ON HOLDERS
L
1. Clean the insert seat
Clean the insert seat in the holder body by blowing air or using a brush.
INDEXABLE MILLING
2. Fit the insert Concave Mark
Place the concave mark of the insert into the clamp-screw-fastening part of the
holder(only SRF type inserts). Fasten the clamp screw while firmly pressing the
insert against the insert seat wall. You are recommended to use the special
lubricant for preventing screw seizing, MK1KS, and to fasten with recommended
torque.
SPARE PARTS N001
TECHNICAL DATA P001 L269