Общий каталог Mitsubishi 2020 - 2021 - страница 1433
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
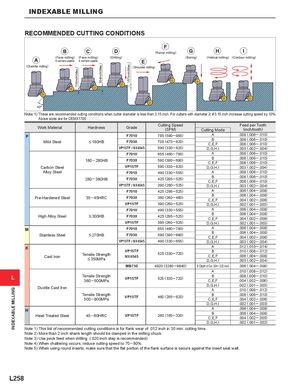
| (Ramp milling) | ||||
| (Chamfer milling) (Face milling) 8 corners usable 118ih(M) Note 1)These are recommended Above sizes are for OEM | (Face milling) 4 corners usable (Dri .ncax. .354inch(Max.) cutting conditions when c X1705pppp. | ling) (Shoulder mil .157inch(Max.) utter diameter is less th | ling) (Boring) (Helical milling) an 3.15 inch. For cutters with diameter>&3.15 inch i | (Contour milling) ncrease cutting speed by |
| Work Material | Hardness | Grade | Cutting Speed (SFM) CuttingMode | Feed per Tooth (inch/tooth) |
| P | F7010 | 785(590─985) A | .008(.006─.010) | |
| Mild Steel | F7030 | B 705(475─820) CEF | .008(.006─.010) .008(.006─.010) | |
| VP15TF / NX4545 | ,, 590(330─820) D,G,H,I | .003(.002─.004) | ||
| F7010 | 655(460─785) A | .008 (.006─.010) | ||
| 180─280HB | F7030 | B 590(390─690) C,E,F | .008(.006─.010) .008(.006─.010) | |
| Carbon Steel | VP15TF | 590(330─820) D,G,H,I | .003(.002─.004) | |
| Alloy Steel | F7010 | 490(330─555) A | .008(.006─.010) | |
| B | .008(.006─.010) | |||
| 280─380HB | F7030 | 425(295─525) C,E,F | .008(.006─.010) | |
| VP15TF / NX4545 | 390(260─525) D,G,H,I | .003(.002─.004) | ||
| F7010 | 425(295─525) A | .006 (.004─.008) | ||
| Pre-Hardened Steel | 35─45HRC | F7030 | B 360(260─460) CEF | .006(.004─.008) .004(.002─.006) |
| VP15TF | ,, 390(260─525) D,G,H,I | .002(.001─.003) | ||
| F7010 | 490(330─555) A | .006 (.004─.008) | ||
| High Alloy Steel | F7030 | B 425(295─525) CEF | .006(.004─.008) .004(.002─.006) | |
| VP15TF | ,, 390(260─525) D,G,H,I | .002(.001─.003) | ||
| M | F7010 | 655(460─785) A | .006(.004─.008) | |
| Stainless Steel | F7030 | B 590(390─690) CEF | .006(.004─.008) .004(.002─.006) | |
| VP15TF / NX4545 | ,, 490(330─655) D,G,H,I | .003(.002─.004) | ||
| K | VP15TF | A B | .012(.010─.014) .010(.008─.012) | |
| Cast Iron | Tensile Strength | NX4545 | 525(330─720) C,E,F | .006(.004─.008) |
| D,G,H,I | .003(.002─.004) | |||
| MB730 | 4920(3280─9840) B(Depth of Cut .004─.020 inch) | .006(.004─.008) | ||
| A | .010 (.008─.012) | |||
| Tensile Strength 360─500MPa | VP15TF | 525(330─720) B C,E,F | .008 (.006─.010) .004(.002─.006) | |
| Ductile Cast Iron | D,G,H,I | .002(.001─.003) | ||
| A | .010(.008─.012) | |||
| Tensile Strength | B | .008(.006─.010) | ||
| 500─800MPa | VP15TF | 460(295─620) CEF | 004(002─006) | |
| ,, D,G,H,I | ... .002(.001─.003) | |||
| H | A | .006(.004─.008) | ||
| Heat-Treated Steel | 45─60HRC | VP15TF | 260(165─330) B CEF | .006(.004─.008) 004(002─005) |
| ,, D,G,H,I | ... .002(.001─.002) |
Note 1) This list of recommended cutting conditions is for flank wear of .012 inch in 30 min. cutting time. Note 2) More than 2 inch shank length should be clamped in the milling chuck. Note 3) Use peck feed when drilling. (.020 inch step is recommended) Note 4) When chattering occurs, reduce cutting speed to 70─ 80%. Note 5) When using round inserts, make sure that the flat portion of the flank surface is secure against the insert seat wall.