Общий каталог Mitsubishi 2020 - 2021 - страница 1423
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
INDEXABLE MILLING
MULTI FUNCTIONAL R
MILLING KAPR R
R
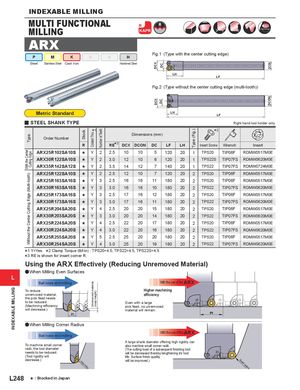
ARX Fig.1 (Type with the center cutting edge)
P M K N S H
Steel Stainless Steel Cast Iron Hardened Steel
DCX
DCON
DC
LH
LF
Fig.2 (Type without the center cutting edge (multi-tooth))
DCON
DCX
DC
Metric Standard LH
LF
y STEEL SHANK TYPE Right hand tool holder only.
* 1
* 2
Number of Teeth
Type (Fig.)
Stock
Dimensions (mm)
Coolant Thru
Type
Order Number
RE*
3
R DCX DCON DC LF LH Insert Screw Wrench Insert
ARX25R102SA10S Y 2 2.5 10 10 5 120 20 TIP06F
the Center
s 1 TPS20 RDMW0517M0E
Cutting Edge
ARX30R122SA10S s Y 2 3.0 12 10 6 120 20 1 TPS22S TIP07FS RDMW0620M0E
ARX35R142SA12S Y 2 140 20 TIP07FS
Without the Center Cutting Edge (Multi-tooth) With
s 3.5 14 12 7 1 TPS22 RDMW0724M0E
ARX25R122SA10S s Y 2 2.5 12 10 7 120 20 2 TPS20 TIP06F RDMW0517M0E
ARX25R163SA16S s Y 3 2.5 16 16 11 180 20 2 TPS20 TIP06F RDMW0517M0E
ARX30R163SA16S s Y 3 3.0 16 16 10 180 20 2 TPS22 TIP07FS RDMW0620M0E
ARX25R173SA16S s Y 3 2.5 17 16 12 180 20 2 TPS20 TIP06F RDMW0517M0E
ARX30R173SA16S s Y 3 3.0 17 16 11 180 20 2 TPS22 TIP07FS RDMW0620M0E
ARX25R204SA20S s Y 4 2.5 20 20 15 180 20 2 TPS20 TIP06F RDMW0517M0E
ARX30R203SA20S s Y 3 3.0 20 20 14 180 20 2 TPS22 TIP07FS RDMW0620M0E
ARX25R224SA20S s Y 4 2.5 22 20 17 180 20 2 TPS20 TIP06F RDMW0517M0E
ARX30R224SA20S s Y 4 3.0 22 20 16 180 20 2 TPS22 TIP07FS RDMW0620M0E
ARX25R255SA20S s Y 5 2.5 25 20 20 180 20 2 TPS20 TIP06F RDMW0517M0E
ARX30R254SA20S s Y 4 3.0 25 20 19 180 20 2 TPS22 TIP07FS RDMW0620M0E
* 1 Y=Yes
*
2 Clamp Torque (lbf-in) : TPS20=4.5, TPS22=4.5, TPS22S=4.5
* 3 RE is shown for insert corner R.
Using the ARX Effectively (Reducing Unremoved Material)
a When Milling Even Surfaces
L
Ball nose end milling With the use of the ARX
Unremoved material
INDEXABLE MILLING
To reduce Higher machining
(cusp height)
unremoved material, efficiency
the pick feed needs
to be reduced. Even with a large
(Machining efficiency pick feed, no unremoved
will decrease.) material will remain.
Pf Pf
a When Milling Corner Radius
With the use of the ARX
Ball nose end milling
A large shank diameter offering high rigidity can
To machine small corner also machine small corner radii.
radii, the tool diameter (The cutting load of a subsequent finishing tool
needs to be reduced. will be decreased thereby lengthening its’ tool
(Tool rigidity will life. Surface finish quality
decrease.) Sm
La
rge will be improved.) all
rad ra
ius diu
s
L248 s : Stocked in Japan
MULTI FUNCTIONAL R
MILLING KAPR R
R
ARX Fig.1 (Type with the center cutting edge)
P M K N S H
Steel Stainless Steel Cast Iron Hardened Steel
DCX
DCON
DC
LH
LF
Fig.2 (Type without the center cutting edge (multi-tooth))
DCON
DCX
DC
Metric Standard LH
LF
y STEEL SHANK TYPE Right hand tool holder only.
* 1
* 2
Number of Teeth
Type (Fig.)
Stock
Dimensions (mm)
Coolant Thru
Type
Order Number
RE*
3
R DCX DCON DC LF LH Insert Screw Wrench Insert
ARX25R102SA10S Y 2 2.5 10 10 5 120 20 TIP06F
the Center
s 1 TPS20 RDMW0517M0E
Cutting Edge
ARX30R122SA10S s Y 2 3.0 12 10 6 120 20 1 TPS22S TIP07FS RDMW0620M0E
ARX35R142SA12S Y 2 140 20 TIP07FS
Without the Center Cutting Edge (Multi-tooth) With
s 3.5 14 12 7 1 TPS22 RDMW0724M0E
ARX25R122SA10S s Y 2 2.5 12 10 7 120 20 2 TPS20 TIP06F RDMW0517M0E
ARX25R163SA16S s Y 3 2.5 16 16 11 180 20 2 TPS20 TIP06F RDMW0517M0E
ARX30R163SA16S s Y 3 3.0 16 16 10 180 20 2 TPS22 TIP07FS RDMW0620M0E
ARX25R173SA16S s Y 3 2.5 17 16 12 180 20 2 TPS20 TIP06F RDMW0517M0E
ARX30R173SA16S s Y 3 3.0 17 16 11 180 20 2 TPS22 TIP07FS RDMW0620M0E
ARX25R204SA20S s Y 4 2.5 20 20 15 180 20 2 TPS20 TIP06F RDMW0517M0E
ARX30R203SA20S s Y 3 3.0 20 20 14 180 20 2 TPS22 TIP07FS RDMW0620M0E
ARX25R224SA20S s Y 4 2.5 22 20 17 180 20 2 TPS20 TIP06F RDMW0517M0E
ARX30R224SA20S s Y 4 3.0 22 20 16 180 20 2 TPS22 TIP07FS RDMW0620M0E
ARX25R255SA20S s Y 5 2.5 25 20 20 180 20 2 TPS20 TIP06F RDMW0517M0E
ARX30R254SA20S s Y 4 3.0 25 20 19 180 20 2 TPS22 TIP07FS RDMW0620M0E
* 1 Y=Yes
*
2 Clamp Torque (lbf-in) : TPS20=4.5, TPS22=4.5, TPS22S=4.5
* 3 RE is shown for insert corner R.
Using the ARX Effectively (Reducing Unremoved Material)
a When Milling Even Surfaces
L
Ball nose end milling With the use of the ARX
Unremoved material
INDEXABLE MILLING
To reduce Higher machining
(cusp height)
unremoved material, efficiency
the pick feed needs
to be reduced. Even with a large
(Machining efficiency pick feed, no unremoved
will decrease.) material will remain.
Pf Pf
a When Milling Corner Radius
With the use of the ARX
Ball nose end milling
A large shank diameter offering high rigidity can
To machine small corner also machine small corner radii.
radii, the tool diameter (The cutting load of a subsequent finishing tool
needs to be reduced. will be decreased thereby lengthening its’ tool
(Tool rigidity will life. Surface finish quality
decrease.) Sm
La
rge will be improved.) all
rad ra
ius diu
s
L248 s : Stocked in Japan