Общий каталог Mitsubishi 2020 - 2021 - страница 1419
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
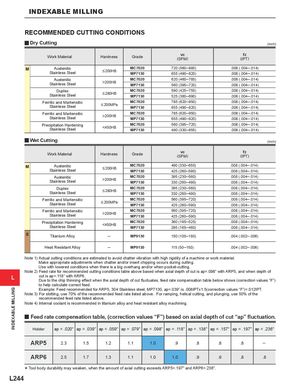
y Dry Cutting
(inch)
| Work Material | Hardness | Grade | vc (SFM) | fz (IPT) |
| M Austenitic | MC7020 | 720(560─885) | .008(.004─.014) | |
| Stainless Steel | MP7130 | 655(490─820) | .008(.004─.014) | |
| Austenitic | >200HB | MC7020 | 620(460─785) | .008(.004─.014) |
| Stainless Steel | MP7130 | 560(395─720) | .008(.004─.014) | |
| Duplex | MC7020 | 590(425─755) | .008(.004─.014) | |
| Stainless Steel | MP7130 | 525(360─690) | .008(.004─.014) | |
| Ferritic and Martensitic | MC7020 | 785(620─950) | .008(.004─.014) | |
| Stainless Steel | a | MP7130 | 655(490─820) | .008(.004─.014) |
| Ferritic and Martensitic | >200HB | MC7020 | 785(620─950) | .008(.004─.014) |
| Stainless Steel | MP7130 | 655(490─820) | .008(.004─.014) | |
| Precipitation Hardening | MC7020 | 560(395─720) | .008(.004─.014) | |
| Stainless Steel | MP7130 | 490(330─655) | .008(.004─.014) |
y Wet Cutting
(inch)
| Work Material | Hardness | Grade | vc (SFM) | fz (IPT) |
| M Austenitic | MC7020 | 490(330─655) | .008(.004─.014) | |
| Stainless Steel | MP7130 | 425(260─590) | .008(.004─.014) | |
| Austenitic | MC7020 | 395(230─560) | .008(.004─.014) | |
| Stainless Steel | >200HB | MP7130 | 330(260─490) | .008(.004─.014) |
| Duplex | MC7020 | 395(230─560) | .008(.004─.014) | |
| Stainless Steel | MP7130 | 330(260─490) | .008(.004─.014) | |
| Ferritic and Martensitic | MC7020 | 560(395─720) | .008(.004─.014) | |
| Stainless Steel | MP7130 | 425(260─590) | .008(.004─.014) | |
| Ferritic and Martensitic | MC7020 | 560(395─720) | .008(.004─.014) | |
| Stainless Steel | >200HB | MP7130 | 425(260─590) | .008(.004─.014) |
| Precipitation Hardening | MC7020 | 360(195─525) | .008(.004─.014) | |
| Stainless Steel | MP7130 | 295(165─460) | .008(.004─.014) | |
| S Titanium Alloy | ─ | MP9130 | 150 (100─180) | .004 (.002─.006) |
| Heat Resistant Alloy | ─ | MP9130 | 115 (50─150) | .004 (.002─.006) |
Note 1) Actual cutting conditions are estimated to avoid chatter vibration with high rigidity of a machine or work material. Make appropriate adjustments when chatter and/or insert chipping occurs during cutting. Use with lowered conditions when there is a big overhang and/or when pocket-cutting. Note 2) Feed rate for recommended cutting conditions table above based when axial depth of cut is ap=.098” with ARP5, and when depth of L cut is ap=.118” with ARP6. Due to the chip thinning effect when the axial depth of cut fluctuates, feed rate compensation table below shows (correction values “F”) to help calculate correct feed. Example: Feed recommended for ARP5, 304 Stainless steel, MP7130, ap=.039” is .008IPTx1.5(correction values “F”)=.012IPT. Note 3) For slotting, use 70% of the recommended feed rate listed above. For ramping, helical cutting, and plunging, use 50% of the recommended feed rate listed above. Note 4) Internal coolant is recommended in titanium alloy and heat resistant alloy machining. y Feed rate compensation table, (correction values “F”) based on axial depth of cut “ap” fluctuation.
| Holder | ap = .020" | ap = .039" | ap = .059" | ap = .079" | ap = .098" | ap = .118" | ap = .138" | ap = .157" | ap = .197" | ap = .236" |
| ARP5 | 2.3 | 1.5 | 1.2 | 1.1 | 1.0 | .9 | .8 | .8 | .8 | ─ |
| ARP6 | 2.5 | 1.7 | 1.3 | 1.1 | 1.0 | 1.0 | .9 | .9 | .8 | .8 |
* Tool body durability may weaken, when the amount of axial cutting exceeds ARP5=.197" and ARP6=.236".