Общий каталог Mitsubishi 2020 - 2021 - страница 1359
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
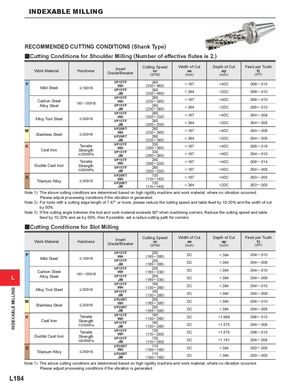
RECOMMENDED CUTTING CONDITIONS (Shank Type)
yCutting Conditions for Shoulder Milling (Number of effective flutes is 2.)
| Work Material | Hardness | Insert Grade/Breaker | Cutting Speed vc (SFM) | Width of Cut ae (inch) | Depth of Cut ap (inch) | Feed per Tooth fz (IPT) |
| P Mild Stl | VP15TF WH | 395 (330─460) | .006─.010 | |||
| ee | VP15TF JM | 395 (330─460) | .006─.010 | |||
| Carbon Steel | 180─350HB | VP15TF WH | 260 (230─395) | .006─.010 | ||
| Alloy Steel | VP15TF JM | 260 (230─395) | .006─.010 | |||
| All Tl Stl | VP15TF WH | 260 (200─330) | .004─.008 | |||
| oy oo ee | VP15TF JM | 260 (200─330) | .004─.008 | |||
| M Stil Stl | VP20RT WH | 260 (230─395) | .004─.008 | |||
| aness ee | VP20RT JM | 260 (230─395) | .004─.008 | |||
| K Ct I | Tensile | VP15TF WH | 330 (260─395) | .006─.016 | ||
| as ron | Strength | VP15TF JM | 330 (260─395) | .004─.010 | ||
| DilCI | Tensile | VP15TF WH | 260 (200─330) | .006─.014 | ||
| ucte ast ron | Strength | VP15TF JM | 260 (200─330) | .004─.008 | ||
| S Titi All | VP20RT WH | 130 (115─165) | .003─.005 | |||
| anum oy | VP20RT JM | 130 (115─165) | .003─.005 |
Note 1) The above cutting conditons are determined based on high rigidity machine and work material, where no vibration occurred. Please adjust processing conditions if the vibration is generated. Note 2) For tools with a cutting edge length of 7.87″ or more, please reduce the cutting speed and table feed by 10-20% and the width of cut by 50%. Note 3) If the cutting angle between the tool and work material exceeds 90º when machining corners ,Reduce the cutting speed and table feed by 10-20% and ae by 50%. Also if possible, set a radius cutting path for corners.
yCutting Conditions for Slot Milling
| Work Material | Hardness | Insert Grade/Breaker | Cutting Speed vc (SFM) | Width of Cut ae (inch) | Depth of Cut ap (inch) | Feed per Tooth fz (IPT) |
| P Mild Stl | VP15TF WH | 200 (165─395) | DC | .004─.010 | ||
| ee | VP15TF JM | 200 (165─395) | DC | .004─.006 | ||
| Carbon Steel | 180─350HB | VP15TF WH | 200 (165─330) | DC | .004─.010 | |
| Alloy Steel | VP15TF JM | 200 (165─330) | DC | .004─.006 | ||
| All Tl Stl | VP15TF WH | 165 (130─260) | DC | .004─.010 | ||
| oy oo ee | VP15TF JM | 165 (130─260) | DC | .004─.006 | ||
| M Stil Stl | VP20RT WH | 200 (165─395) | DC | .004─.010 | ||
| aness ee | VP20RT JM | 200 (165─395) | DC | .004─.006 | ||
| K | Tensile | VP15TF WH | 165 (130─260) | DC | .006─.010 | |
| Cast Iron | Strength | VP15TF JM | 165 (130─260) | DC | .004─.008 | |
| Tensile | VP15TF WH | 130 (115─260) | DC | .006─.010 | ||
| Ductile Cast Iron | Strength | VP15TF JM | 130 (115─260) | DC | .004─.008 | |
| S | VP20RT WH | 115 (100─165) | DC | .003─.005 | ||
| Titanium Alloy | 350 | VP20RT JM | 115 (100─165) | DC | .003─.005 |
Note 1) The above cutting conditons are determined based on high rigidity machine and work material, where no vibration occurred. Please adjust processing conditions if the vibration is generated.