Общий каталог Mitsubishi 2020 - 2021 - страница 1313
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
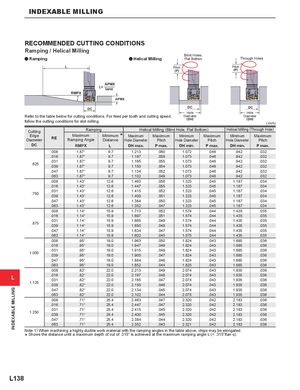
RECOMMENDED CUTTING CONDITIONS
Ramping / Helical Milling
Blind Holes,
a Ramping a Helical Milling Flat Bottom Through Holes
L Pitch Pitch
(P) (P)
APMX L= tan RMPX APMX
| DC | DC | DC |
| Hole | Hole |
| Refer to the table below for cutting conditions. For feed per tooth and cutting speed, | Diameter | Diameter |
| follow the cutting conditions for slot milling. | (DH) | (DH) |
(inch)
| Cutting | Rampin | g | Helica | l Milling (Blin | d Hole, Flat Bot | tom) | Helical Milling ( | Through Hole) | |
| Edge Diameter DC | RE | Maximum Ramping Angle RMPX | Minimum Distance L | Maximum Hole Diameter DH max. | Maximum Pitch P max. | Minimum Hole Diameter DH min. | Maximum Pitch P max. | Minimum Hole Diameter DH min. | Maximum Pitch P max. |
| .008 | 1.87° | 9.7 | 1.213 | .060 | 1.072 | .046 | .942 | .032 | |
| .016 | 1.87° | 9.7 | 1.197 | .059 | 1.073 | .046 | .942 | .032 | |
| .031 | 1.87° | 9.7 | 1.165 | .055 | 1.073 | .046 | .942 | .032 | |
| .625 | .039 | 1.87° | 9.7 | 1.150 | .054 | 1.073 | .046 | .942 | .032 |
| .047 | 1.87° | 9.7 | 1.134 | .052 | 1.073 | .046 | .942 | .032 | |
| .063 | 1.87° | 9.7 | 1.102 | .049 | 1.073 | .046 | .942 | .032 | |
| .008 | 1.43° | 12.6 | 1.463 | .056 | 1.323 | .045 | 1.187 | .034 | |
| .016 | 1.43° | 12.6 | 1.447 | .055 | 1.323 | .045 | 1.187 | .034 | |
| .031 | 1.43° | 12.6 | 1.415 | .052 | 1.323 | .045 | 1.187 | .034 | |
| .750 | .039 | 1.43° | 12.6 | 1.400 | .051 | 1.323 | .045 | 1.187 | .034 |
| .047 | 1.43° | 12.6 | 1.384 | .050 | 1.323 | .045 | 1.187 | .034 | |
| .063 | 1.43° | 12.6 | 1.352 | .047 | 1.323 | .045 | 1.187 | .034 | |
| .008 | 1.14° | 15.9 | 1.713 | .052 | 1.574 | .044 | 1.435 | .035 | |
| .016 | 1.14° | 15.9 | 1.697 | .051 | 1.574 | .044 | 1.435 | .035 | |
| .031 | 1.14° | 15.9 | 1.665 | .049 | 1.574 | .044 | 1.435 | .035 | |
| .875 | .039 | 1.14° | 15.9 | 1.650 | .048 | 1.574 | .044 | 1.435 | .035 |
| .047 | 1.14° | 15.9 | 1.634 | .047 | 1.574 | .044 | 1.435 | .035 | |
| .063 | 1.14° | 15.9 | 1.602 | .045 | 1.575 | .044 | 1.435 | .035 | |
| .008 | .95° | 19.0 | 1.963 | .050 | 1.824 | .043 | 1.685 | .036 | |
| .016 | .95° | 19.0 | 1.947 | .049 | 1.824 | .043 | 1.685 | .036 | |
| .031 | .95° | 19.0 | 1.915 | .048 | 1.824 | .043 | 1.685 | .036 | |
| 1.000 | .039 | .95° | 19.0 | 1.900 | .047 | 1.824 | .043 | 1.685 | .036 |
| .047 | .95° | 19.0 | 1.884 | .046 | 1.824 | .043 | 1.685 | .036 | |
| .063 | .95° | 19.0 | 1.852 | .044 | 1.825 | .043 | 1.685 | .036 | |
| .008 | .82° | 22.0 | 2.213 | .049 | 2.074 | .043 | 1.935 | .036 | |
| .016 | .82° | 22.0 | 2.197 | .048 | 2.074 | .043 | 1.935 | .036 | |
| 112 | .031 | .82° | 22.0 | 2.165 | .047 | 2.074 | .043 | 1.935 | .036 |
| .5 | .039 | .82° | 22.0 | 2.150 | .046 | 2.074 | .043 | 1.935 | .036 |
| .047 | .82° | 22.0 | 2.134 | .045 | 2.074 | .043 | 1.935 | .036 | |
| .063 | .82° | 22.0 | 2.102 | .044 | 2.075 | .043 | 1.935 | .036 | |
| .008 | .71° | 25.4 | 2.463 | .047 | 2.320 | .042 | 2.183 | .036 | |
| .016 | .71° | 25.4 | 2.447 | .047 | 2.320 | .042 | 2.183 | .036 | |
| .031 | .71° | 25.4 | 2.415 | .045 | 2.320 | .042 | 2.183 | .036 | |
| 1.250 | .039 | .71° | 25.4 | 2.400 | .045 | 2.320 | .042 | 2.183 | .036 |
| .047 | .71° | 25.4 | 2.384 | .044 | 2.320 | .042 | 2.183 | .036 | |
| .063 | .71° | 25.4 | 2.352 | .043 | 2.321 | .042 | 2.183 | .036 |
Note 1) When machining a highly ductile work material with the ramping angles in the table above, chips may be elongated.* Shows the distance until a maximum depth of cut of .315" is achieved at the maximum ramping angle L (= .315"/tan α).