Общий каталог Mitsubishi 2020 - 2021 - страница 1230
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
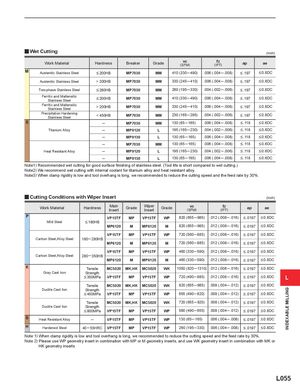
y Wet Cutting
(inch)
| Work Material | Hardness | Breaker | Grade | vc (SFM) | fz (IPT) | ap | ae |
| M Austenitic Stainless Steel | MP7030 | MM | 410 (330─490) | .006 (.004─.008) | |||
| Austenitic Stainless Steel | > 200HB | MP7030 | MM | 330 (245─410) | .006 (.004─.008) | ||
| Two-phase Stainless Steel | MP7030 | MM | 260 (195─330) | .004 (.002─.006) | |||
| Ferritic and Maltensitic Stainless Steel | MP7030 | MM | 410 (330─490) | .006 (.004─.008) | |||
| Ferritic and Maltensitic Stainless Steel | > 200HB | MP7030 | MM | 330 (245─410) | .006 (.004─.008) | ||
| Precipitation Hardening Stainless Steel | < 450HB | MP7030 | MM | 230 (165─295) | .004 (.002─.006) | ||
| S | ─ | MP7030 | MM | 130 (65─165) | .006 (.004─.008) | ||
| Titanium Alloy | ─ | MP9120 | L | 195 (165─230) | .004 (.002─.006) | ||
| ─ | MP9130 | L | 130 (65─165) | .006 (.004─.008) | |||
| ─ | MP7030 | MM | 130 (65─165) | .006 (.004─.008) | |||
| Heat Resistant Alloy | ─ | MP9120 | L | 195 (165─230) | .004 (.002─.006) | ||
| ─ | MP9130 | L | 130 (65─165) | .006 (.004─.008) |
Note1) Recommended wet cutting for good surface finishing of stainless steel. (Tool life is short compared to wet cutting.) Note2) We recommend wet cutting with internal coolant for titanium alloy and heat resistant alloy. Note3) When clamp rigidity is low and tool overhang is long, we recommended to reduce the cutting speed and the feed rate by 30%.
| Cutting Conditions | ith Wiper I | nsert | (inch) | ||||||
| Work Material | Hardness | Main Insert | Grade | Wiper Insert | Grade | vc (SFM) | fz (IPT) | ap | ae |
| P Mild Stl | VP15TF | MP | VP15TF | WP | 820 (655─985) | .012 (.008─.016) | |||
| ee | MP6120 | M | MP6120 | M | 820 (655─985) | .012 (.008─.016) | |||
| Carbon SteelAllo Steel | 180─280HB | VP15TF | MP | VP15TF | WP | 720 (560─885) | .012 (.008─.016) | ||
| ,y | MP6120 | M | MP6120 | M | 720 (560─885) | .012 (.008─.016) | |||
| Cb StlAll Stl | 280─350HB | VP15TF | MP | VP15TF | WP | 460 (330─590) | .012 (.008─.016) | ||
| aron ee,oy ee | MP6120 | M | MP6120 | M | 460 (330─590) | .012 (.008─.016) | |||
| K GCtI | Tensile | MC5020 | MK,HK | MC5020 | WK | 1050 (820─1310) | .012 (.008─.016) | ||
| ray as ron | Strength | VP15TF | MP | VP15TF | WP | 720 (490─985) | .012 (.008─.016) | ||
| Dtil Ct Il | Tensile | MC5020 | MK,HK | MC5020 | WK | 820 (655─985) | .008 (.004─.012) | ||
| uce as on | Strength | VP15TF | MP | VP15TF | WP | 655 (490─820) | .008 (.004─.012) | ||
| Tensile | MC5020 | MK,HK | MC5020 | WK | 720 (655─820) | .008 (.004─.012) | |||
| Ductile Cast Ilon | Strength | VP15TF | MP | VP15TF | WP | 560 (490─655) | .008 (.004─.012) | ||
| S Heat Resistant Alloy | ─ | VP15TF | MP | VP15TF | WP | 130 (65─165) | .006 (.004─.008) | ||
| H Hardened Steel | 40─55HRC | VP15TF | MP | VP15TF | WP | 260 (195─330) | .006 (.004─.008) |
Note 1) When clamp rigidity is low and tool overhang is long, we recommended to reduce the cutting speed and the feed rate by 30%. Note 2) Please use WP geometry insert in combination with MP or M geometry inserts, and use WK geometry insert in combination with MK or HK geometry inserts