Общий каталог Mitsubishi 2020 - 2021 - страница 1222
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
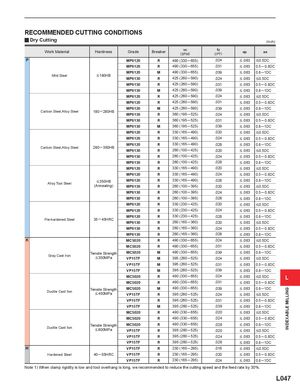
y Dry Cutting
(inch)
| Work Material | Hardness | Grade | Breaker | vc (SFM) | fz (IPT) | ap | ae |
| P | MP6120 | R | 490(330─655) | .024 | |||
| MP6120 | R | 490 (330─655) | .031 | 0.5 ─0.8DC | |||
| MP6120 | M | 490 (330─655) | .039 | 0.8 ─1DC | |||
| Mild Steel | MP6130 | R | 425 (260─590) | .024 | |||
| MP6130 | R | 425 (260─590) | .031 | 0.5 ─0.8DC | |||
| MP6130 | M | 425 (260─590) | .039 | 0.8 ─1DC | |||
| MP6120 | R | 425 (260─590) | .024 | ||||
| MP6120 | R | 425 (260─590) | .031 | 0.5 ─0.8DC | |||
| MP6120 | M | 425 (260─590) | .039 | 0.8 ─1DC | |||
| Carbon Steel,Alloy Steel | 180─280HB | MP6130 | R | 360 (195─525) | .024 | ||
| MP6130 | R | 360 (195─525) | .031 | 0.5 ─0.8DC | |||
| MP6130 | M | 360 (195─525) | .039 | 0.8 ─1DC | |||
| MP6120 | R | 330 (165─490) | .020 | ||||
| MP6120 | R | 330 (165─490) | .024 | 0.5 ─0.8DC | |||
| MP6120 | R | 330 (165─490) | .028 | 0.8 ─1DC | |||
| Carbon Steel,Alloy Steel | 280─350HB | MP6130 | R | 260 (100─425) | .020 | ||
| MP6130 | R | 260 (100─425) | .024 | 0.5 ─0.8DC | |||
| MP6130 | R | 260 (100─425) | .028 | 0.8 ─1DC | |||
| MP6120 | R | 330 (165─490) | .020 | ||||
| MP6120 | R | 330 (165─490) | .024 | 0.5 ─0.8DC | |||
| MP6120 | R | 330 (165─490) | .028 | 0.8 ─1DC | |||
| Alloy Tool Steel | (Annealing) | MP6130 | R | 260 (100─395) | .020 | ||
| MP6130 | R | 260 (100─395) | .024 | 0.5 ─0.8DC | |||
| MP6130 | R | 260 (100─395) | .028 | 0.8 ─1DC | |||
| MP6120 | R | 330 (230─425) | .020 | ||||
| MP6120 | R | 330 (230─425) | .024 | 0.5 ─0.8DC | |||
| MP6120 | R | 330 (230─425) | .028 | 0.8 ─1DC | |||
| Pre-hardened Steel | 35─45HRC | MP6130 | R | 260 (165─360) | .020 | ||
| MP6130 | R | 260 (165─360) | .024 | 0.5 ─0.8DC | |||
| MP6130 | R | 260 (165─360) | .028 | 0.8 ─1DC | |||
| K | MC5020 | R | 490 (330─655) | .024 | |||
| MC5020 | R | 490 (330─655) | .031 | 0.5 ─0.8DC | |||
| GCI | Tensile Strength | MC5020 | M | 490 (330─655) | .039 | 0.8 ─1DC | |
| ray ast ron | VP15TF | M | 395 (260─525) | .024 | |||
| VP15TF | M | 395 (260─525) | .031 | 0.5 ─0.8DC | |||
| VP15TF | M | 395 (260─525) | .039 | 0.8 ─1DC | |||
| MC5020 | R | 490 (330─655) | .024 | ||||
| MC5020 | R | 490 (330─655) | .031 | 0.5 ─0.8DC | |||
| Tensile Strength | MC5020 | M | 490 (330─655) | .039 | 0.8 ─1DC | ||
| Ductile Cast Ilon | VP15TF | R | 395 (260─525) | .024 | |||
| VP15TF | R | 395 (260─525) | .031 | 0.5 ─0.8DC | |||
| VP15TF | M | 395 (260─525) | .039 | 0.8 ─1DC | |||
| MC5020 | R | 490 (330─655) | .020 | ||||
| MC5020 | R | 490 (330─655) | .024 | 0.5 ─0.8DC | |||
| Tensile Strength | MC5020 | R | 490 (330─655) | .028 | 0.8 ─1DC | ||
| Ductile Cast Ilon | VP15TF | R | 395 (260─525) | .020 | |||
| VP15TF | R | 395 (260─525) | .024 | 0.5 ─0.8DC | |||
| VP15TF | R | 395 (260─525) | .028 | 0.8 ─1DC | |||
| H | VP15TF | R | 230 (165─295) | .016 | |||
| Hardened Steel | 40─55HRC | VP15TF | R | 230 (165─295) | .020 | 0.5 ─0.8DC | |
| VP15TF | R | 230 (165─295) | .024 | 0.8 ─1DC |
Note 1) When clamp rigidity is low and tool overhang is long, we recommended to reduce the cutting speed and the feed rate by 30%.