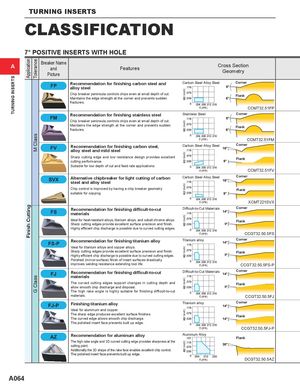
7° POSITIVE INSERTS WITH HOLE
| A | Breaker Name | | | Cross Section | |
| | and | Features | | |
| | | | | Geometry |
| | Picture | | | |
| FP Recommendation for finishing carbon steel and | Carbon Steel·Alloy Steel | Corner |
| alloy steel | | |
| Chip breaker peninsula controls chips even at small depth of cut. | (inch | Flank |
| Maintains the edge strength at the corner and prevents sudden | | |
| fractures. | | |
| | CCMT32.51FP f (IPR) |
| Recommendation for finishing stainless steel | Stainless Steel | Corner |
| FM | | |
| Chip breaker peninsula controls chips even at small depth of cut. | | |
| Maintains the edge strength at the corner and prevents sudden | (inch | Flank |
| fractures. | | |
| | CCMT32.51FM f (IPR) |
| Recommendation for finishing carbon steel, | Carbon Steel·Alloy Steel | Corner |
| alloy steel and mild steel | | |
| Sharp cutting edge and low resistance design provides excellent | (inch | Flank |
| cutting performance. | | |
| Suitable for low depth of cut and feed rate applications. | | |
| | CCMT32.51FV f (IPR) |
| Alternative chipbreaker for light cutting of carbon | Carbon Steel·Alloy Steel | Corner |
| steel and alloy steel | | |
| Chip control is improved by having a chip breaker geometry | (inch | Flank |
| suitable for copying. | | |
| | XCMT221SVX f (IPR) |
| Recommendation for finishing difficult-to-cut | Difficult-to-Cut Materials | Corner |
| FS materials | | |
| Ideal for heat-resistant alloys, titanium alloys, and cobalt chrome alloys. | (inch | Flank |
| Sharp cutting edges provide excellent surface precision and finish. | | 9° |
| Highly efficient chip discharge is possible due to curved cutting edges. | | |
| | CCGT32.50.5FS f (IPR) |
| Recommendation for finishing titanium alloy | Titanium alloy | Corner |
| FS-P | | |
| Ideal for titanium alloys and copper alloys. | | |
| Sharp cutting edges provide excellent surface precision and finish. | (inch | Flank |
| Highly efficient chip discharge is possible due to curved cutting edges. | | 9° |
| Polished (mirror-surface) finish of insert surfaces drastically | | |
| improves welding resistance extending tool life. | f | CCGT32.50.5FS-P |
| (IPR) | |
| Recommendation for finishing difficult-to-cut | Difficult-to-Cut Materials | | Corner |
| materials | | | |
| The curved cutting edges support changes in cutting depth and | (inch | | Flank |
| allow smooth chip discharge and disposal. | | 9° | |
| The high rake angle is highly suitable for finishing difficult-to-cut | | | |
| materials. | f | CCGT32.50.5FJ |
| (IPR) | |
Finishing titanium alloy Titanium alloy Corner
Ideal for aluminum and copper. The sharp edge produces excellent surface finishes. (inch Flank The curved edge allows smooth chip discharge.
The polished insert face prevents built up edge. f (IPR) CCGT32.50.5FJ-P Recommendation for aluminum alloy Aluminum Alloy Flank The high rake angle and 3D curved cutting edge provides sharpness at the cutting point. (inch Additionally the 3D shape of the rake face enables excellent chip control. The polished insert face prevents built up edge. f (IPR) DCGT32.50.5AZ
 Каталог Mitsubishi Materials запасные части
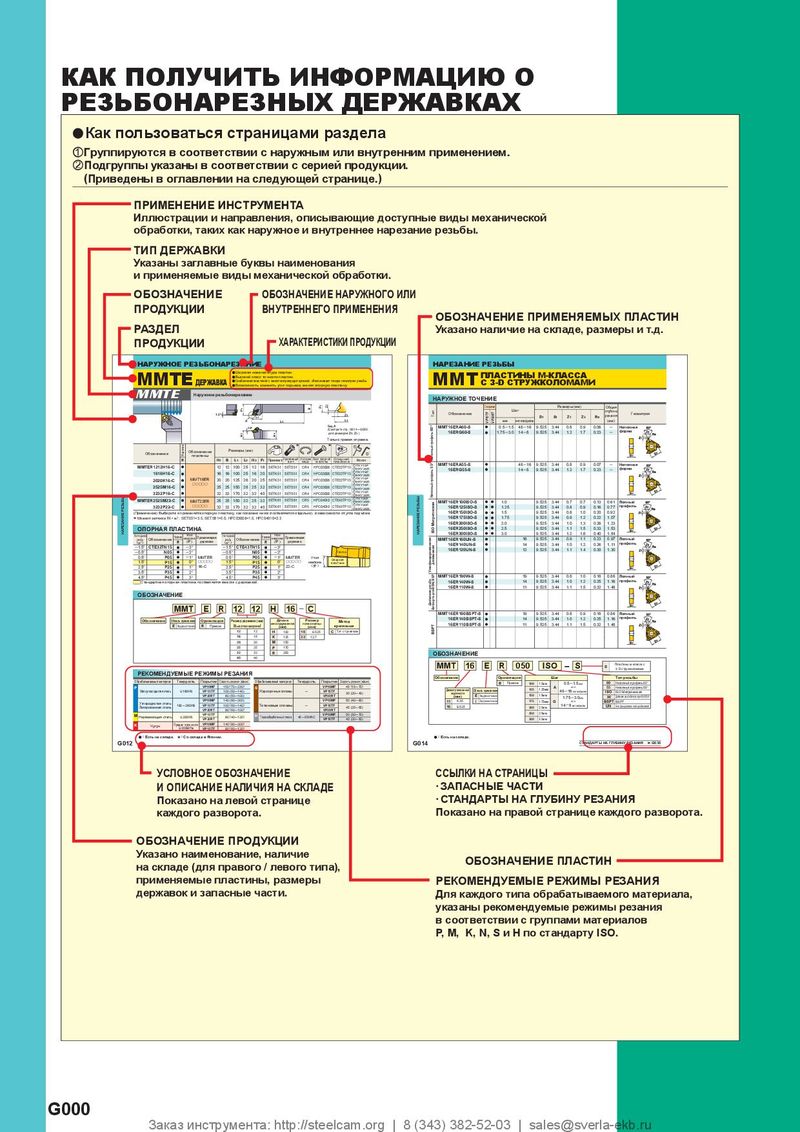 Каталог Mitsubishi Materials резьбонарезной инструмент
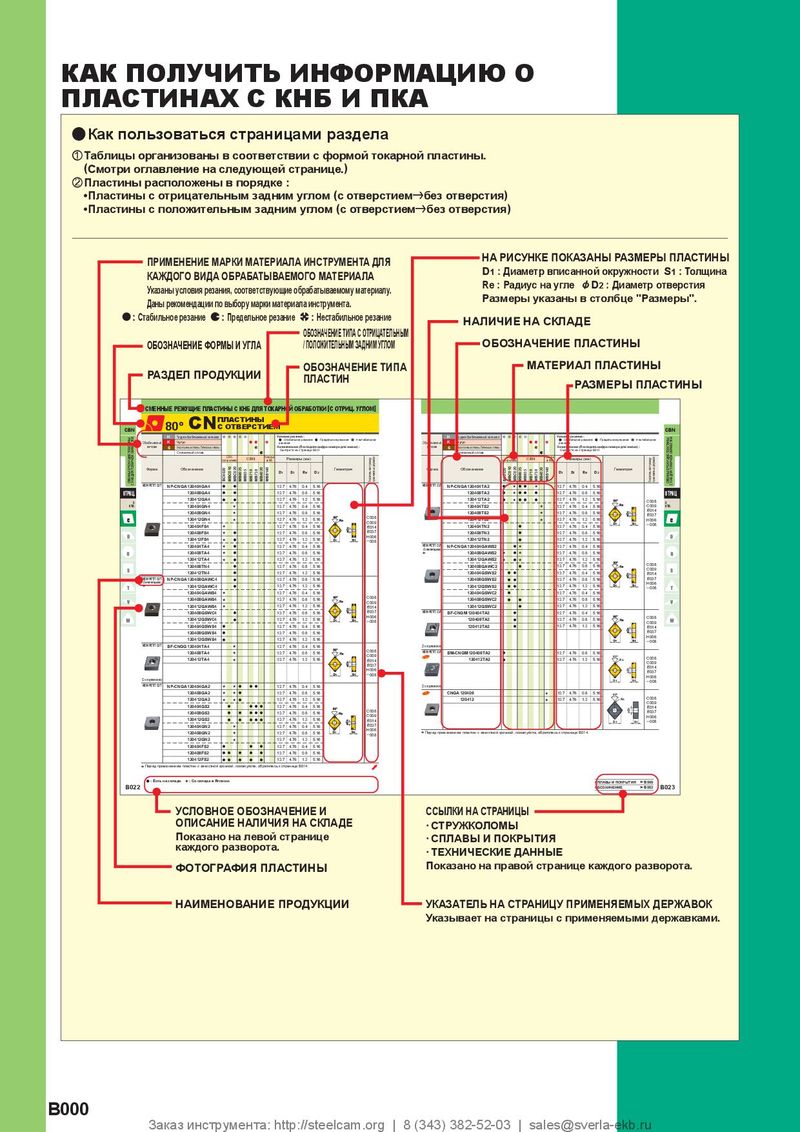 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
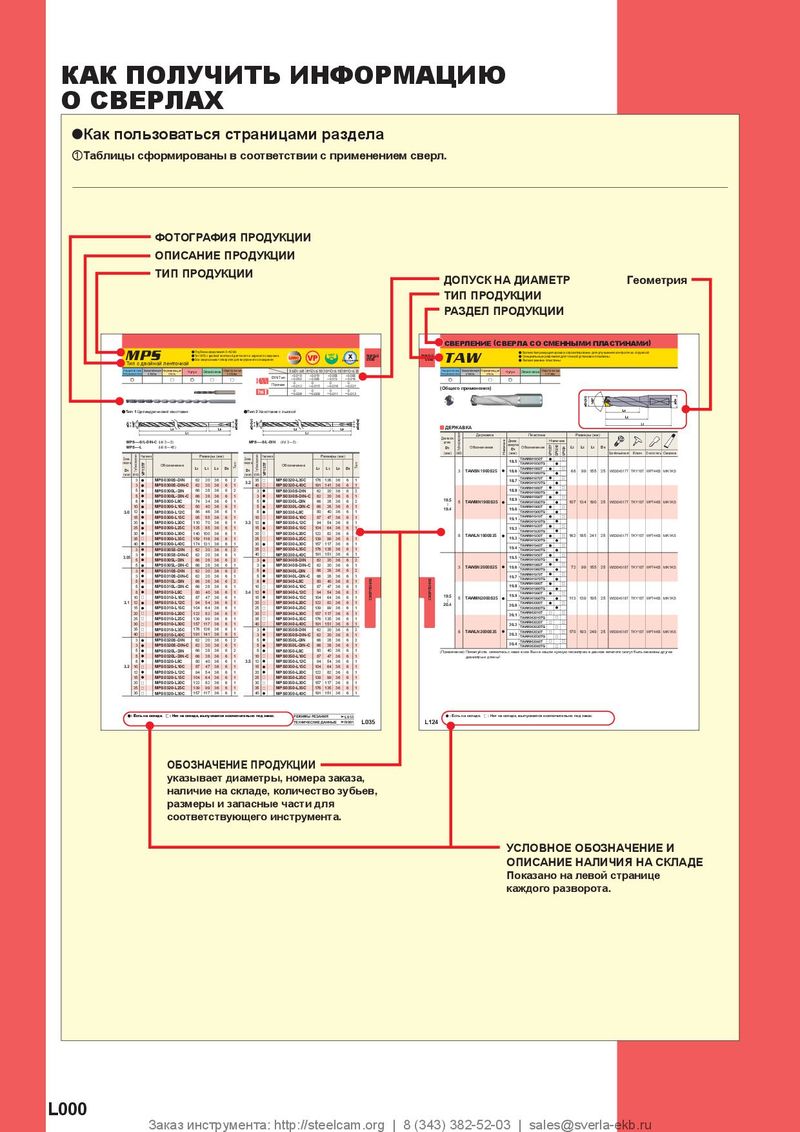 Каталог Mitsubishi Materials сверлильные инструменты
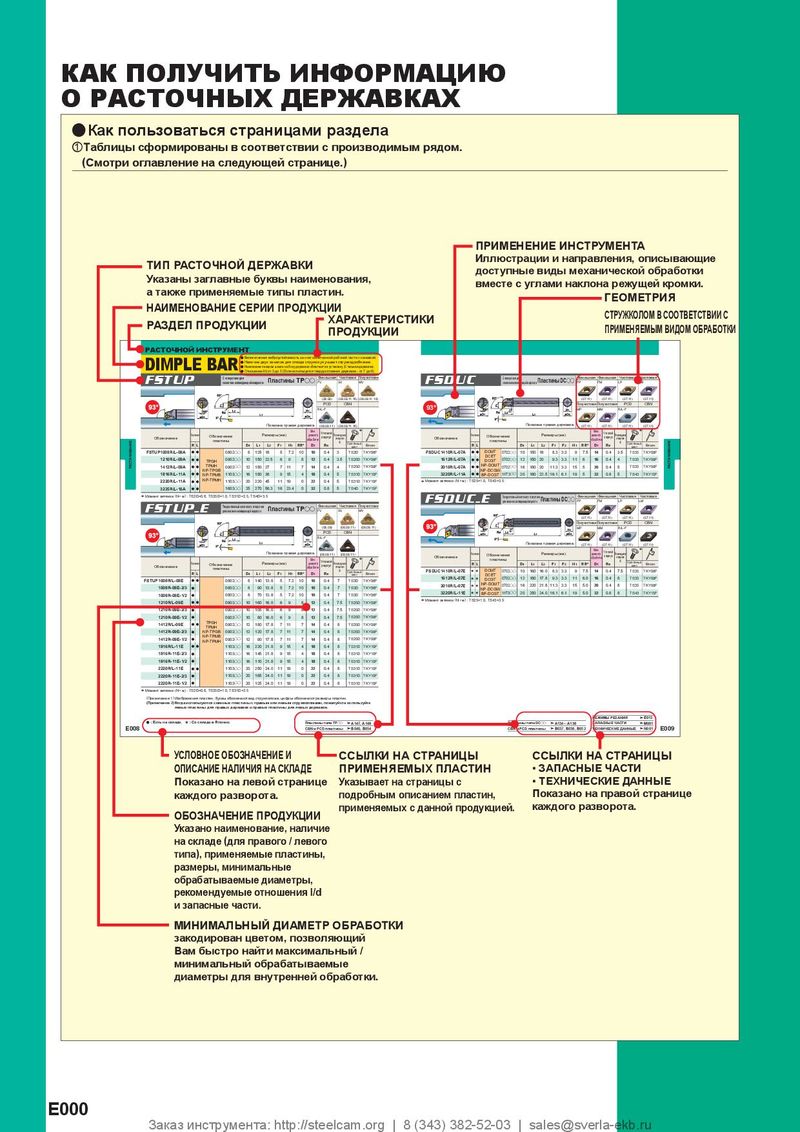 Каталог Mitsubishi Materials расточной инструмент
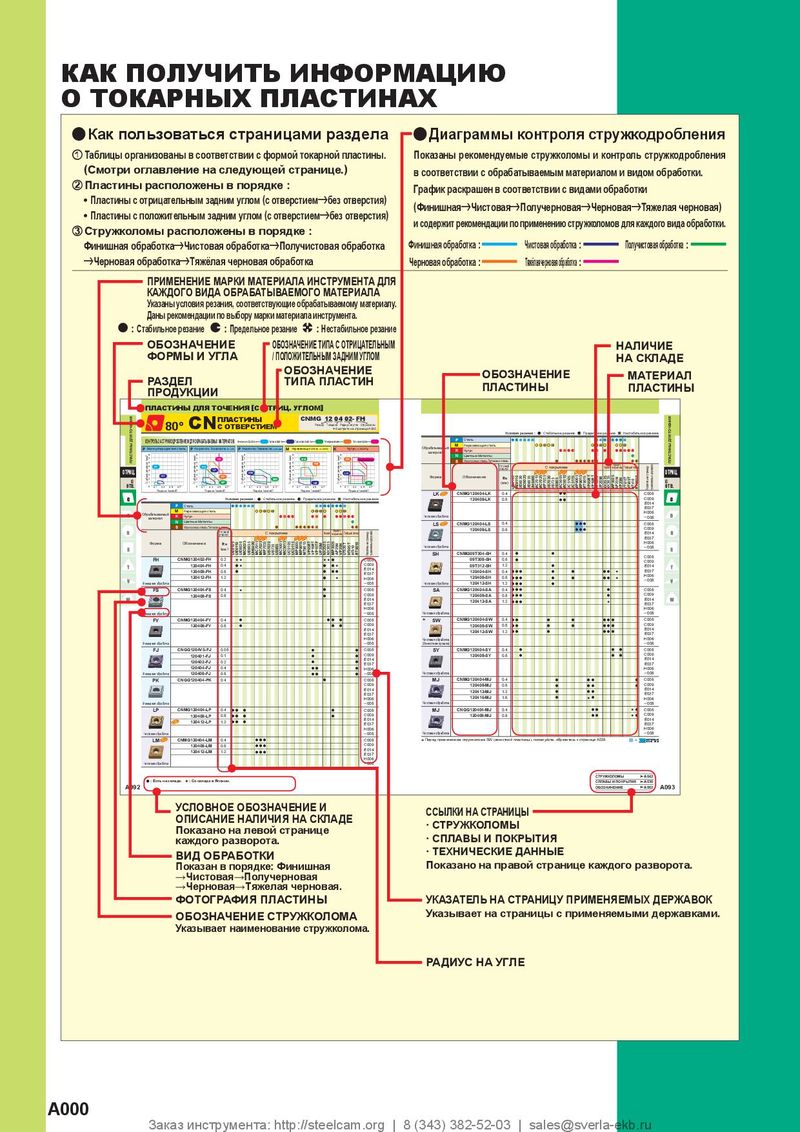 Каталог Mitsubishi Materials пластины для точения