Общий каталог Mitsubishi 2020 - 2021 - страница 1012
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
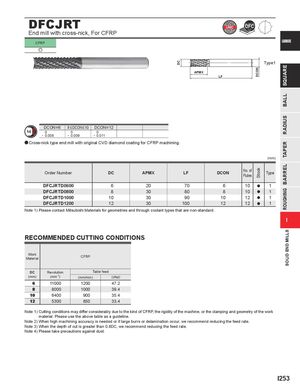
DFCJRT
End mill with cross-nick, For CFRP
CFRP e
APMX
LF
CARBIDE
Type1
| DCON=6 | 8 | DCON | 10 | DCON=12 |
| 0 | 0 | 0 | ||
| - 0.008 | - 0.009 | - 0.011 |
a Cross-nick type end mill with original CVD diamond coating for CFRP machining.
| (mm) | |||||||
| Order Number | DC | APMX | LF | DCON | No. of Flutes | Stock | Type |
| DFCJRTD0600 | 6 | 20 | 70 | 6 | 10 | a | 1 |
| DFCJRTD0800 | 8 | 30 | 80 | 8 | 10 | a | 1 |
| DFCJRTD1000 | 10 | 30 | 90 | 10 | 12 | a | 1 |
| DFCJRTD1200 | 12 | 30 | 100 | 12 | 12 | a | 1 |
Note 1) Please contact Mitsubishi Materials for geometries and through coolant types that are non-standard.
I
RECOMMENDED CUTTING CONDITIONS
| Work Material | CFRP | ||
| DC | Revolution | Table | feed |
| (mm) | (min-1) | (mm/min) | (IPM) |
| 6 | 11000 | 1200 | 47.2 |
| 8 | 8000 | 1000 | 39.4 |
| 10 | 6400 | 900 | 35.4 |
| 12 | 5300 | 850 | 33.4 |
Note 1) Cutting conditions may differ considerably due to the kind of CFRP, the rigidity of the machine, or the clamping and geometry of the work material. Please use the above table as a guideline. Note 2) When high machining accuracy is needed or if large burrs or delamination occur, we recommend reducing the feed rate. Note 3) When the depth of cut is greater than 0.8DC, we recommend reducing the feed rate. Note 4) Please take precautions against dust.