Общий каталог Mitsubishi 2020 - 2021 - страница 1010
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
CARBIDE
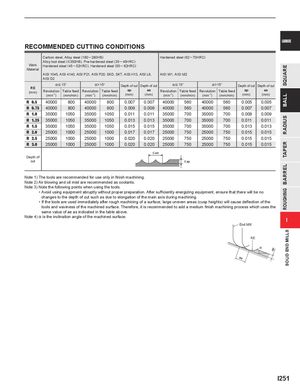
RECOMMENDED CUTTING CONDITIONS
| Work Material | Carbon stee Alloy tool st Hardened s AISI 1045, A AISI D2 | l, Alloy steel eel ( teel (45─52H ISI 4140,AIS | (180─280H , Pre-harde RC), Harde I P21, AISI P | B) ned steel (35 ned steel (55 20, SKD, SK | ─45HRC) ─62HRC) T, AISI H13, | AISI L6, | Hardened s AISI W1, AI | teel (62─70 SI M2 | HRC) | |||
| RE | % | 15° | %> | 15° | Depth of cut | Depth of cut | % | 15° | %>1 | 5° | Depth of cut | Depth of cut |
| (mm) | Revolution (min-1) | Table feed (mm/min) | Revolution (min-1) | Table feed (mm/min) | ap (mm) | ae (mm) | Revolution (min-1) | Table feed (mm/min) | Revolution (min-1) | Table feed (mm/min) | ap (mm) | ae (mm) |
| R 0.5 | 40000 | 800 | 40000 | 800 | 0.007 | 0.007 | 40000 | 560 | 40000 | 560 | 0.005 | 0.005 |
| R 0.75 | 40000 | 800 | 40000 | 800 | 0.009 | 0.009 | 40000 | 560 | 40000 | 560 | 0.007 | 0.007 |
| R 1.0 | 35000 | 1050 | 35000 | 1050 | 0.011 | 0.011 | 35000 | 700 | 35000 | 700 | 0.009 | 0.009 |
| R 1.25 | 35000 | 1050 | 35000 | 1050 | 0.013 | 0.013 | 35000 | 700 | 35000 | 700 | 0.011 | 0.011 |
| R 1.5 | 35000 | 1050 | 35000 | 1050 | 0.015 | 0.015 | 35000 | 700 | 35000 | 700 | 0.013 | 0.013 |
| R 2.0 | 25000 | 1000 | 25000 | 1000 | 0.017 | 0.017 | 25000 | 750 | 25000 | 750 | 0.015 | 0.015 |
| R 2.5 | 25000 | 1000 | 25000 | 1000 | 0.020 | 0.020 | 25000 | 750 | 25000 | 750 | 0.015 | 0.015 |
| R 3.0 | 25000 | 1000 | 25000 | 1000 | 0.020 | 0.020 | 25000 | 750 | 25000 | 750 | 0.015 | 0.015 |
| Depth of cut |
Note 1) The tools are recommended for use only in finish machining. Note 2) Air blowing and oil mist are recommended as coolants. Note 3) Note the following points when using the tools.
- Avoid using equipment abruptly without proper preparation. After sufficiently energizing equipment, ensure that there will be no changes to the depth of cut such as due to elongation of the main axis during machining.
- If the tools are used immediately after rough machining of a surface, large uneven areas (cusp heights) will cause deflection of the tools and waviness of the machined surface. Therefore, it is recommended to add a medium finish machining process which uses the same value of ae as indicated in the table above.
Note 4) % is the inclination angle of the machined surface. I End Mill
RE ap ae