Общий каталог Mitsubishi 2020 - 2021 - страница 1002
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
CARBIDE
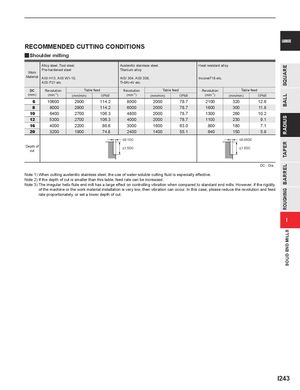
RECOMMENDED CUTTING CONDITIONS
yShoulder milling
| Work Material | Alloy steel, Tool Pre-hardened st AISI H13, AISI W AISI P21 etc. | steel, eel 1-10, | Austenitic stainl Titanium alloy AISI 304, AISI 3 Ti-6Al-4V etc. | ess steel, 06, | Heat resistant a Inconel718 etc. | lloy | |||
| DC | Revolution | Table | feed | Revolution | Table | feed | Revolution | Table f | eed |
| (mm) | (min-1) | (mm/min) | (IPM) | (min-1) | (mm/min) | (IPM) | (min-1) | (mm/min) | (IPM) |
| 6 | 10600 | 2900 | 114.2 | 8000 | 2000 | 78.7 | 2100 | 320 | 12.6 |
| 8 | 8000 | 2900 | 114.2 | 6000 | 2000 | 78.7 | 1600 | 300 | 11.8 |
| 10 | 6400 | 2700 | 106.3 | 4800 | 2000 | 78.7 | 1300 | 260 | 10.2 |
| 12 | 5300 | 2700 | 106.3 | 4000 | 2000 | 78.7 | 1100 | 230 | 9.1 |
| 16 | 4000 | 2200 | 86.6 | 3000 | 1600 | 63.0 | 800 | 180 | 7.1 |
| 20 | 3200 | 1900 | 74.8 | 2400 | 1400 | 55.1 | 640 | 150 | 5.9 |
| Depth of cut |
DC : Dia. Note 1) When cutting austenitic stainless steel, the use of water-soluble cutting fluid is especially effective. Note 2) If the depth of cut is smaller than this table, feed rate can be increased. Note 3) The irregular helix flute end mill has a large effect on controlling vibration when compared to standard end mills. However, if the rigidity of the machine or the work material installation is very low, then vibration can occur. In this case, please reduce the revolution and feed rate proportionately, or set a lower depth of cut.