Каталог SGS микро инструмент 2021 - страница 70
Навигация
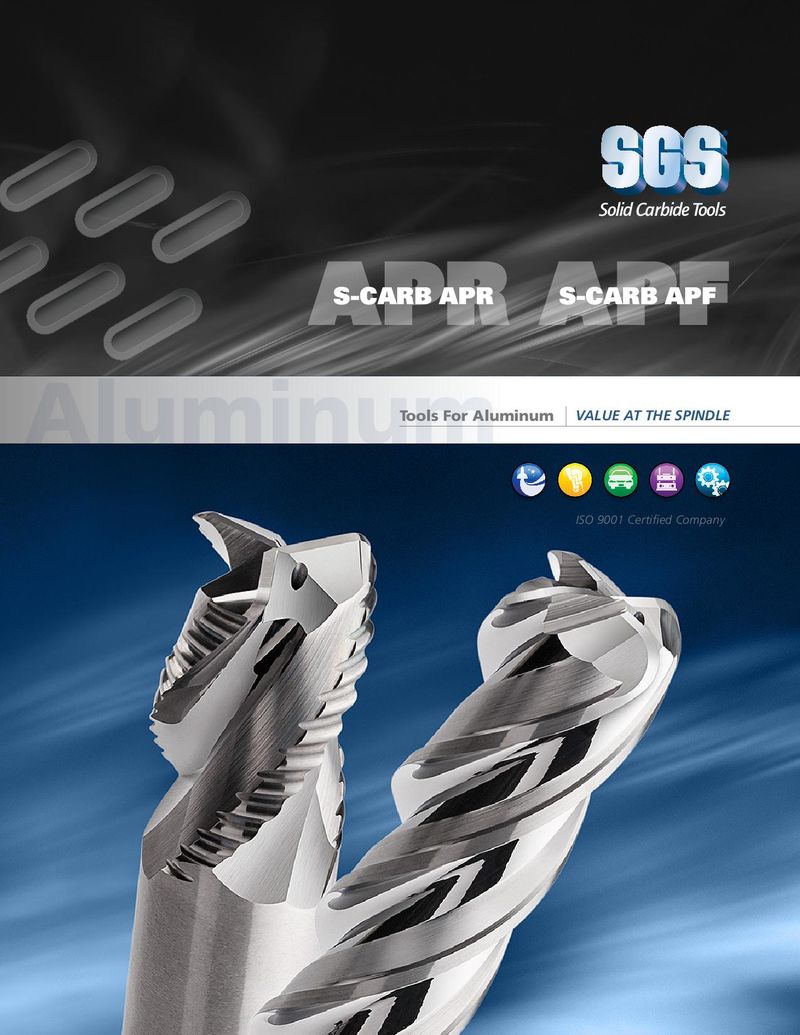 Каталог SGS фрезы для алюминия S-carb
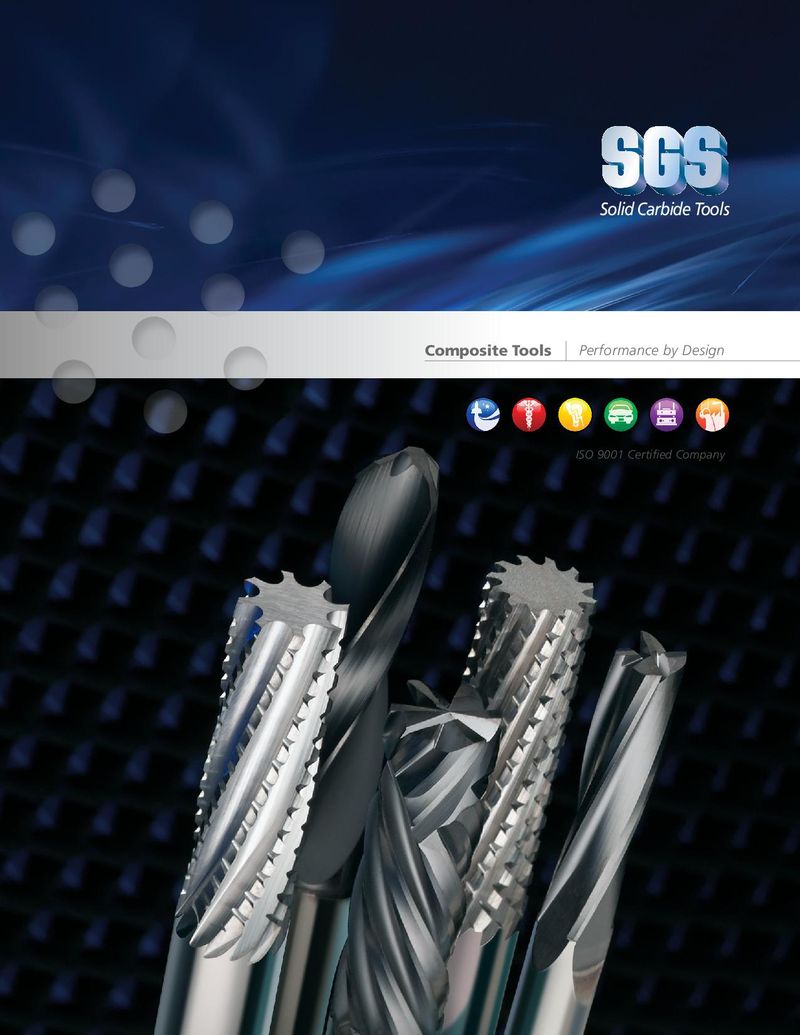 Каталог SGS монолитный инструмент из композитных материалов
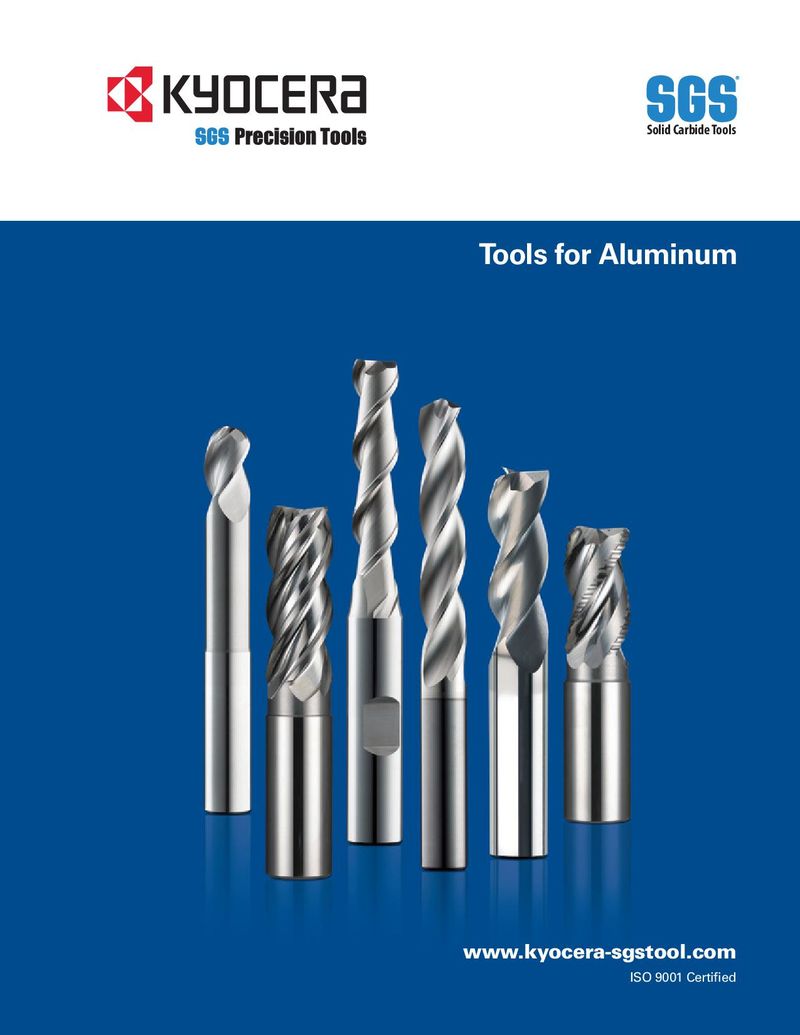 Каталог SGS инструмент для обработки алюминия
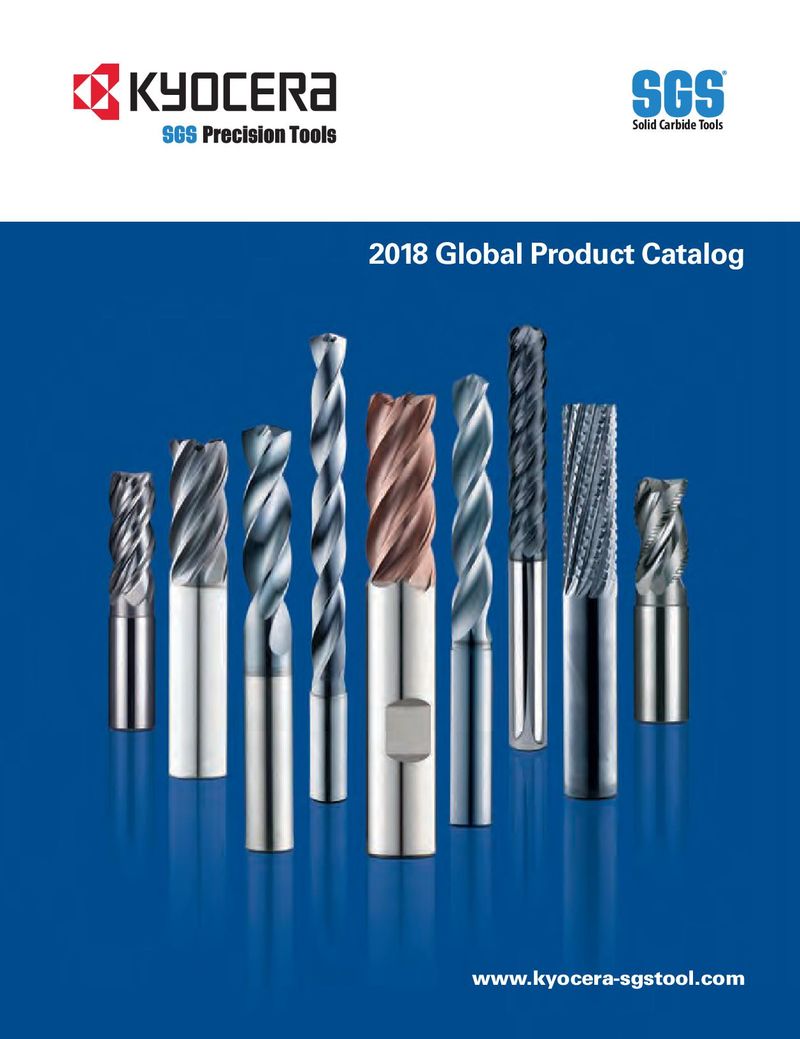 Общий каталог SGS 2018
 Общий каталог SGS 2021
 Каталог SGS фрезы для труднообрабатываемых материалов Series 33
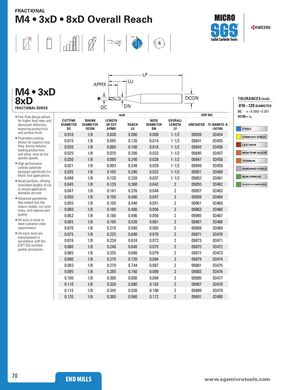
30° POS 15° 4
| LF | |||||||||
| AP | MX | LU | |||||||
| M4 • 3xD | |||||||||
| DCON | TOLERANCES(inch) | ||||||||
| FRACTIONAL SERIES | DC | DN | .010–.120DIAMETER DC =+0000/–0001 | ||||||
| • Four flute design allows | inch | EDP | NO. | .. DCON =h6 | |||||
| for higher feed rates and decreased deflection, improving productivity | CUTTING DIAMETER DC | SHANK DIAMETER DCON | LENGTH OF CUT APMX | REACH LU | NECK DIAMETER DN | OVERALL LENGTH LF | UNCOATED | TI-NAMITE-A (AlTiN) | STEELS |
| and surface finish. | 0.010 | 1/8 | 0.030 | 0.080 | 0.009 | 1-1/2 | 09839 | 03454 | STAINLESS STEELS |
| • Proprietary coating allows for superior chip | 0.015 | 1/8 | 0.045 | 0.120 | 0.014 | 1-1/2 | 09841 | 03455 | |
| flow, driving industry | 0.020 | 1/8 | 0.060 | 0.160 | 0.018 | 1-1/2 | 09843 | 03456 | CAST IRON |
| leading productivity and value, even at low | 0.025 | 1/8 | 0.075 | 0.200 | 0.023 | 1-1/2 | 09845 | 03457 | HIGH TEMP ALLOYS |
| spindle speeds. | 0.030 | 1/8 | 0.090 | 0.240 | 0.028 | 1-1/2 | 09847 | 03458 | TITANIUM |
| • High performance carbide substrate | 0.031 | 1/8 | 0.093 | 0.248 | 0.029 | 1-1/2 | 09849 | 03459 | HARDENED STEELS |
| designed specifically for | 0.035 | 1/8 | 0.105 | 0.280 | 0.032 | 1-1/2 | 09851 | 03460 | |
| Micro Tool applications. • Bd tfli ffi | 0.040 | 1/8 | 0.120 | 0.320 | 0.037 | 1-1/2 | 09853 | 03461 | NON-FERROUS |
| roa poroo, oerng consistent lengths of cut, | 0.045 | 1/8 | 0.135 | 0.360 | 0.042 | 2 | 09855 | 03462 | PLASTICS/COMPOSITES |
| to ensure application demands are met | 0.047 | 1/8 | 0.141 | 0.376 | 0.044 | 2 | 09857 | 03463 | |
| . • Advanced geometries | 0.050 | 1/8 | 0.150 | 0.400 | 0.047 | 2 | 09859 | 03464 | |
| that extend tool life, | 0.055 | 1/8 | 0.165 | 0.440 | 0.051 | 2 | 09861 | 03465 | |
| reduce chatter, cut cycle times, and improve part | 0.060 | 1/8 | 0.180 | 0.480 | 0.056 | 2 | 09863 | 03466 | |
| quality. | 0.062 | 1/8 | 0.186 | 0.496 | 0.058 | 2 | 09865 | 03467 | |
| • All tools in stock to meet customer order | 0.065 | 1/8 | 0.195 | 0.520 | 0.061 | 2 | 09867 | 03468 | |
| requirements. | 0.070 | 1/8 | 0.210 | 0.560 | 0.065 | 2 | 09869 | 03469 | |
| • All micro tools are f | 0.075 | 1/8 | 0.225 | 0.600 | 0.070 | 2 | 09871 | 03470 | |
| manuactured in accordance with the | 0.078 | 1/8 | 0.234 | 0.624 | 0.073 | 2 | 09873 | 03471 | |
| KSPT ISO certified lit d | 0.080 | 1/8 | 0.240 | 0.640 | 0.075 | 2 | 09875 | 03472 | |
| quay proceures. | 0.085 | 1/8 | 0.255 | 0.680 | 0.079 | 2 | 09877 | 03473 | |
| 0.090 | 1/8 | 0.270 | 0.720 | 0.084 | 2 | 09879 | 03474 | ||
| 0.093 | 1/8 | 0.279 | 0.744 | 0.087 | 2 | 09881 | 03475 | ||
| 0.095 | 1/8 | 0.285 | 0.760 | 0.089 | 2 | 09883 | 03476 | ||
| 0.100 | 1/8 | 0.300 | 0.800 | 0.094 | 2 | 09885 | 03477 | ||
| 0.110 | 1/8 | 0.330 | 0.880 | 0.103 | 2 | 09887 | 03478 | ||
| 0.115 | 1/8 | 0.345 | 0.920 | 0.108 | 2 | 09889 | 03479 | ||
| 0.120 | 1/8 | 0.360 | 0.960 | 0.112 | 2 | 09891 | 03480 |