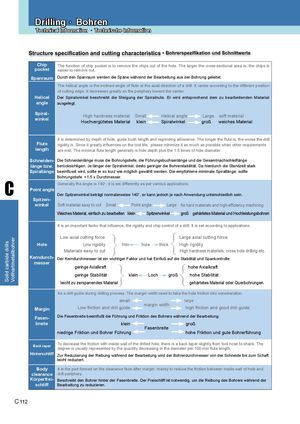
| Chip pocket Spanraum | The function of chip pocket is to remove the chips out of the hole. The larger the cross-sectional area is, the chips is easier to remove out. Durch den Spanraum werden die Späne während der Bearbeitung aus der Bohrung geleitet. |
| Helical angle | The helical angle is the inclined angle of flute at the axial direction of a drill. It varies according to the different position of cutting edge. It decreases greatly as the periphery toward the center. Der Spiralwinkel beschreibt die Steigung der Spiralnute. Er wird entsprechend dem zu bearbeitenden Material ausgelegt. |
| Spiral- winkel | High hardness material Small Helical angle Large soft material Hochvergütetes Material klein Spiralwinkel groß weiches Material |
| Flute length | It is determined by depth of hole, guide bush length and regrinding allowance. The longer the flute is, the worse the drill rigidity is. Since it greatly influences on the tool life, please minimize it as much as possible when other requirements are met. The minimal flute length generally is hole depth plus the 1.5 times of hole diameter. |
| Schneiden- länge bzw. Spirallänge | Die Schneidenlänge muss die Bohrungstiefe, die Führungsbuchsenlänge und die Gesamtnachschleiflänge berücksichtigen. Je länger der Spiralwinkel, desto geringer die Bohrerstabilität. Da hierdurch die Standzeit stark beeinflusst wird, sollte er so kurz wie möglich gewählt werden. Die empfohlene minimale Spirallänge: sollte Bohrungstiefe +1,5 x Durchmesser. |
| Point angle Hole Spitzen- winkel | Generally the angle is 140°, it is set differently as per various applications. Soft material easy to cut Small Point angle Large It is an important factor that influence, the rigidity and chip control of a drill. It is set according to applications. Low axial cutting force Large axial cutting force Low rigidity thin hole thick High rigidity Materials easy to cutHigh hardness materials, cross hole drilling etc. for hard materials and high-efficiency machining Der Spitzenwinkel beträgt normalerweise 140°, er kann jedoch je nach Anwendung unterschiedlich sein. Weiches Material, einfach zu bearbeiten klein Spitzenwinkel groß gehärtetes Material und Hochleistungsbohren |
| Kerndurch- messer | Der Kerndurchmesser ist ein wichtiger Faktor und hat Einfluß auf die Stabilität und Spankontrolle: geringe Axialkraft hohe Axialkraft geringeStabilität klein Loch groß hohe Stabilität leicht zu zerspanendes Material gehärtetes Material oder Querbohrungen. |
| Margin | As a drill guide during drilling process. The margin width need to take the hole friction into consideration. small margin width large Low friction and drill guide high friction and good drill guide |
| Fasen- breite | Die Fasenbreite beeinflußt die Führung und Friktion des Bohrers während der Bearbeitung. klein groß niedrige Friktion und Bohrer Führung hohe Friktion und gute Bohrerführung Fasenbreite |
| Back taper Hinterschliff | To decrease the friction with inside wall of the drilled hole, there is a back taper slightly from tool nose to shank. The degree is usually represented by the quantity decreasing in the diameter per 100 mm flute length. Zur Reduzierung der Reibung während der Bearbeitung wird der Bohrerdurchmesser von der Schneide bis zum Schaft leicht reduziert. |
| Body clearance | It is the part formed on the clearance face after margin, mainly to reduce the friction between inside wall of hole and drill periphery |
| Körperfrei- schliff | Beschreibt den Bohrer hinter der Fasenbreite. Der Freischliff ist notwendig, um die Reibung des Bohrers während der Bearbeitung zu reduzieren. |
 Каталог ZCC-CT сверла со сменными пластинами
 Общий каталог ZCC-CT 2019
 Каталог ZCC-CT расточные системы
 Каталог ZCC-CT фрезы монолитные
 Каталог ZCC-CT фрезы со сменными пластинами
 Каталог ZCC-CT оснастка