Каталог ZCC-CT сверла монолитные - страница 110
Навигация
 Каталог ZCC-CT сверла со сменными пластинами
 Общий каталог ZCC-CT 2019
 Каталог ZCC-CT расточные системы
 Каталог ZCC-CT фрезы монолитные
 Каталог ZCC-CT фрезы со сменными пластинами
 Каталог ZCC-CT оснастка
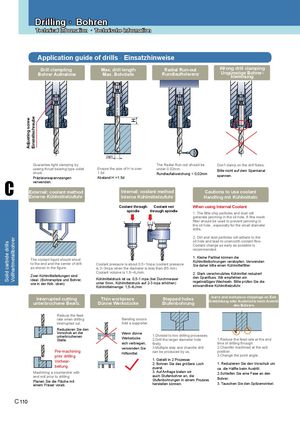
Application guide of drills Einsatzhinweise·
| Drill clampling | Max. drill length | Radial Run-out | Wrong drill clamping |
| Bohrer Aufnahme | Max. Bohrtiefe | Rundlauftoleranz | Ungünstige Bohrer- |
klemmung
| Guarantee tight clamping by | The Radial Run-out should be | Don't clamp on the drill flutes. | |
| useing thrust bearing type collet | Ensure the size of H is over | under 0.02mm. | Bitte nicht auf dem Spankanal |
| chuck.. | 1.5d | Rundlaufabweichung < 0,02mm | |
| Abstand H =1.5d | spannen. | ||
| C Präzisionsspannzangen | |||
| verwenden. |
| External: coolant method | Internal: coolant method | Cautions to use coolant |
| Externe Kühlmittelzufuhr | Interne Kühlmittelzufuhr | Handling mit Kühlmitteln |
Coolant through Coolant not When using Internal Coolant
spindle through spindle 1. The little chip particles and dust will generate jamming in the oil hole. A fine mesh filter should be used to prevent jamming in
the oil hole , especially for the small diameter drills. 2. Dirt and dust particles will adhere to the oil hole and lead to unsmooth coolant flow. Coolant change as early as possible is recommended. The coolant liquid should shoot 1. Kleine Partikel können die to the end and the center of drill Kühlmittelbohrungen verstopfen. Verwenden Coolant pressure is about 0.5~1mpa (coolant pressure Sie daher bitte einen Kühlmittelfilter. as shown in the figure. is 2~3mpa when the diameter is less than Ø5 mm) Coolant volume is 1.5~4L/min. 2. Stark verschmutztes Kühlmittel reduziert Zwei Kühlmittelleitungen sind den Spanfluss. Wir empfehlen ein ideal. (Bohrerspitze und Bohrer, Kühlmitteldruck ist ca. 0,5-1 mpa (bei Durchmesser
| wie in der Abb. oben) | unter 5mm, Kühlmitteldruck auf 2-3 mpa erhöhen) | regelmäßiges Wechseln. Bitte prüfen Sie die |
| Kühlmittelmenge: 1,5-4L/min | einwandfreie Kühlmittelzufuhr. |
| Interrupted cutting | Thin workpiece | Stepped holes | burrs and workpiece chippings on Exit |
| unterbrochene Bearb. | Dünne Werkstücke | Stufenbohrung | Gratbildung oder Ausbrüche beim Austritt |
des Bohrers Reduce the feed rate when drilling Bending occurs interrupted cut. Add a supporter.
Reduzieren Sie den Vorschub an der Wenn dünne unterbrochenen 1.Divided to two drilling processes.
| Stelle. | Werkstücke | 2.Drill the larger diameter hole | 1.Reduce the feed rate at the end |
| sich verbiegen, | firstly. | time of drilling through | |
| verwenden Sie | 3.Multiple step and chamfer drill | 2.Chamfer machined at the exit | |
| Pre-machining | can be produced by us. | position. |
Hilfsmittel. 3.Change the point angle. prior drilling Vorbear- 1. Geteilt in 2 Prozesse 2. Bohren Sie das größere Loch 1. Reduzieren Sie den Vorschub um
beitung zuerst. ca. die Hälfte beim Austritt.
Machining a countersink with 3. Auf Anfrage bieten wir 2.Schleifen Sie eine Fase an den
end mill prior to drilling. auch Stufenbohrer an, die Stufenbohrungen in einem Prozess Bohrer. Planen Sie die Fläche mit 3. Tauschen Sie den Spitzenwinkel. einem Fräser vorab. herstellen können.